
Engineering decisions, organised
Surface Preparation, Plating & Inspection
Compare mechanical preparation, plating and passivation around the substrate, finish standard, corrosion requirements and inspection plan.
Updated October 11, 2026 · 33 focused articles
Preparation decides whether the finish survives
Most finish failures are preparation failures. Oil, coolant residue, oxide, burrs and fingerprints all sit between the substrate and the coating, and each one produces a defect that looks like a coating problem: poor adhesion, pinholes, patchy colour, blistering. Cleaning and deoxidising are therefore part of the specification, not a housekeeping detail.
The material sets the preparation route. Aluminium needs deoxidising before anodising or conversion coating. Steel needs degreasing and descaling before plating or painting. Stainless needs passivation to remove free iron left by machining or handling, which is the difference between a part that resists corrosion and one that rusts at a fingerprint.
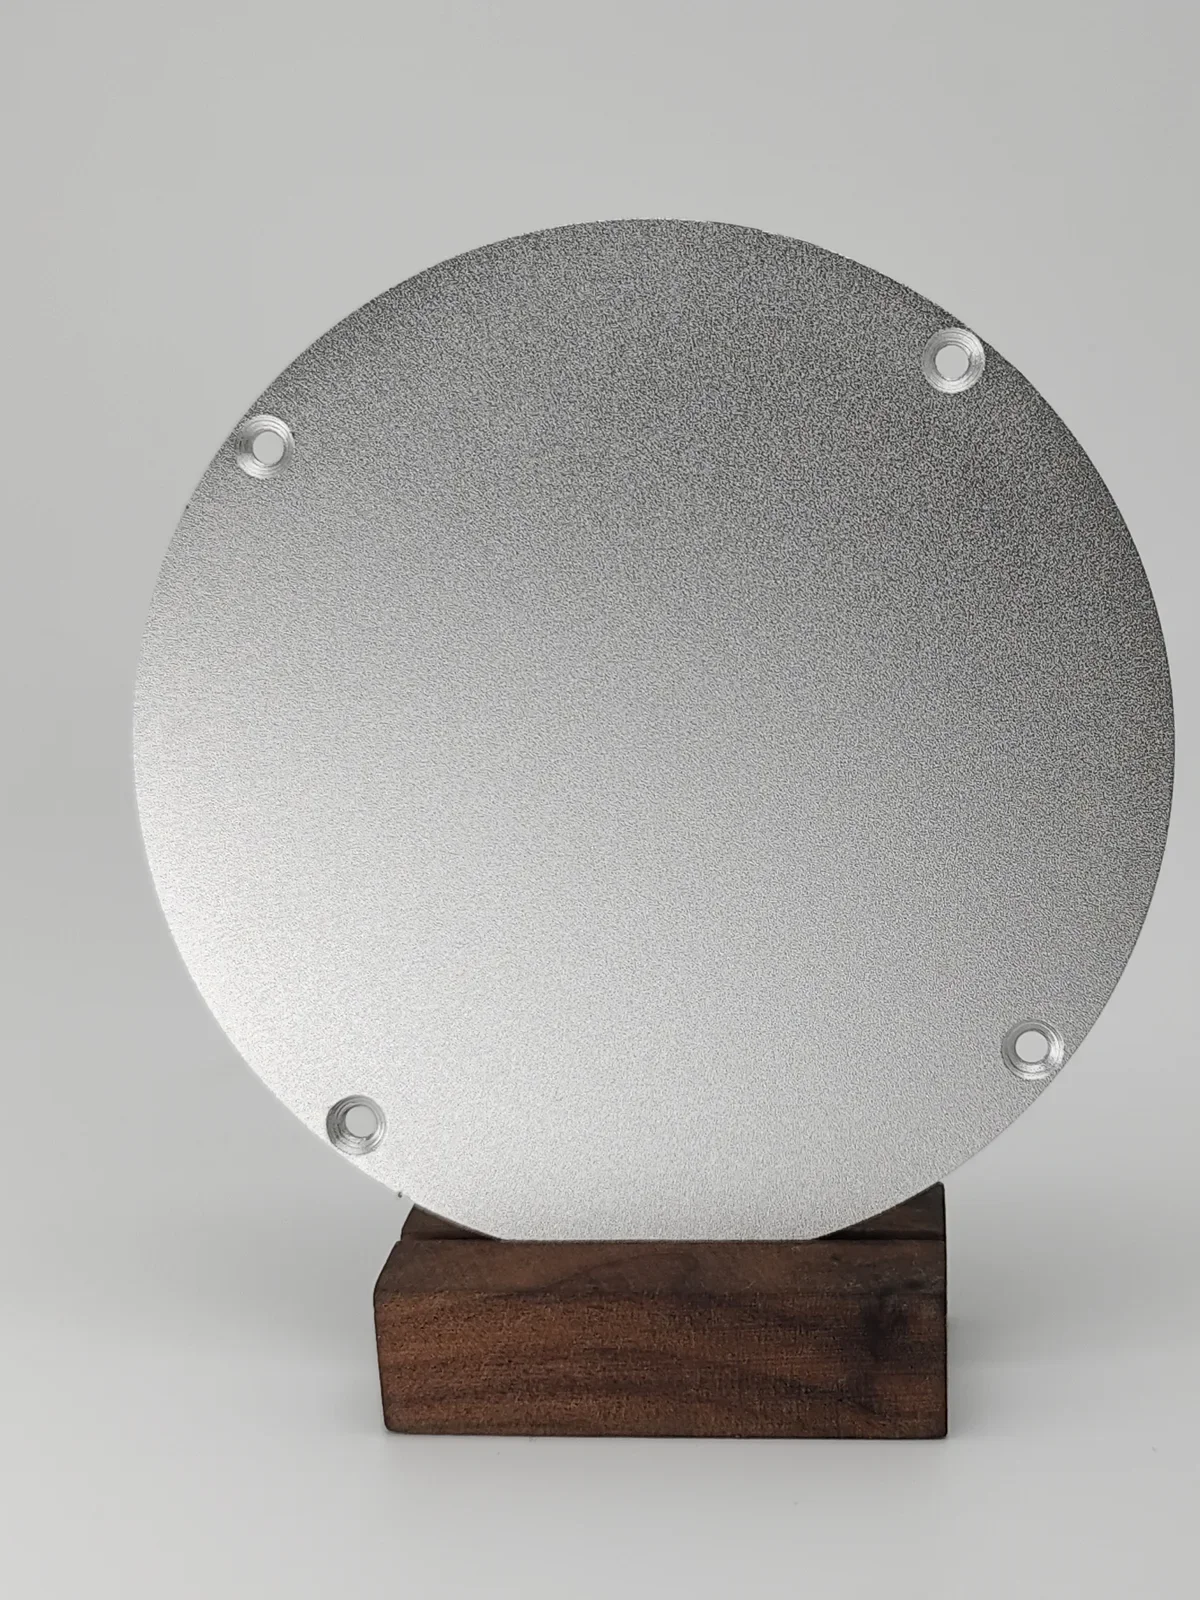
Deburring and edge quality
Edges take coating differently from faces. A sharp edge has less area to hold the film, so it wears through first, and a burr under a coating becomes a defect that lifts. Deburring before finishing is standard for functional edges and cosmetic ones; the method — hand, vibratory, thermal, electrochemical — depends on the edge quality the drawing asks for.
Edge quality also matters for safety and assembly. A 0.2 mm burr on a handling edge is a cut finger, and a burr on a mating face is a clearance problem. Specifying a chamfer or a radius is cheaper than specifying a deburring operation, because the cutter can produce it in the same pass.
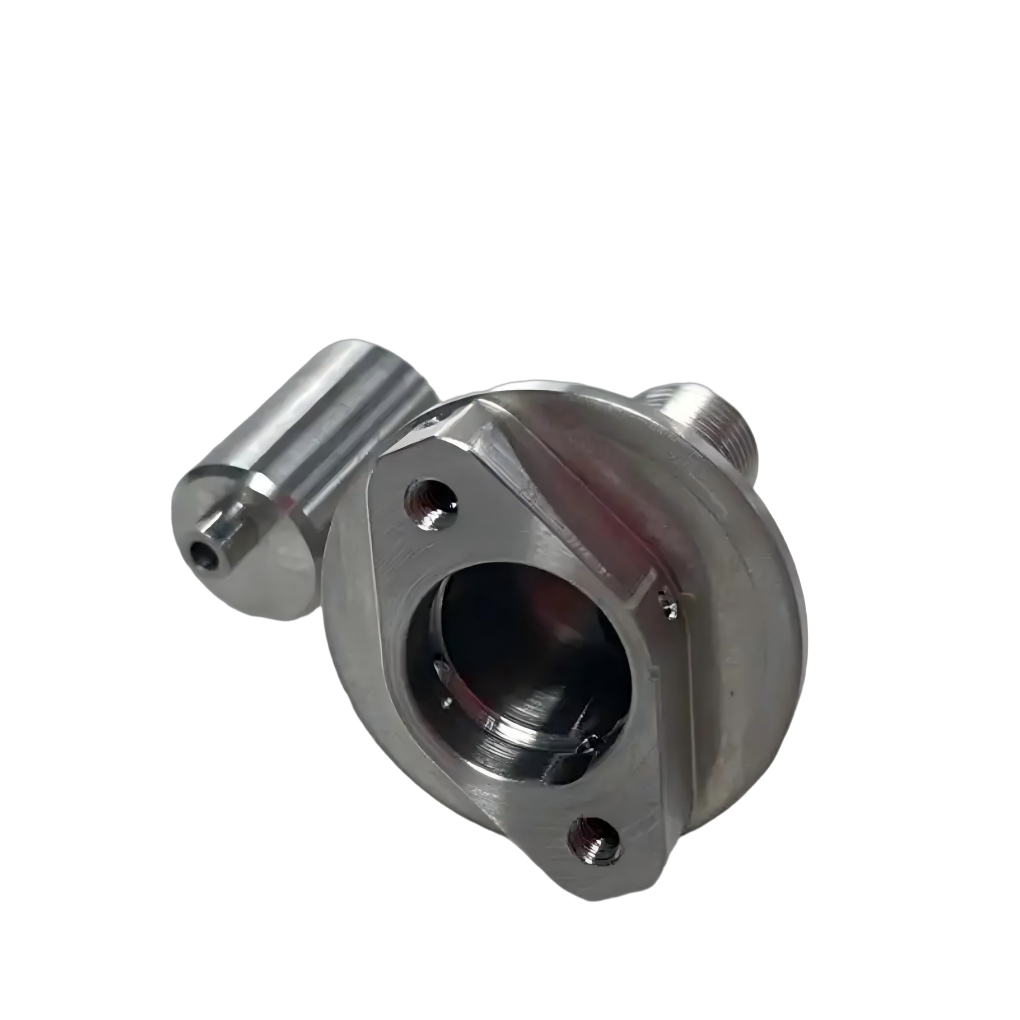
Passivation, cleanliness and the evidence
Passivation is not a coating and does not change dimensions. It removes free iron from a stainless surface and lets the natural oxide layer reform, which is why it is specified after machining, after welding and after blasting. Cleanliness specifications go further: particle counts, hydrocarbon limits and, in medical or semiconductor work, a validated cleaning process with residue testing.
The specification habit that prevents most of this is to name the preparation, not just the finish. Anodise after deoxidising, powder coat after blasting and degreasing, passivate after machining — the sequence is the quality control, and it costs nothing to write down.
Where the part is cleaned between operations rather than at the end, say so. Handling marks, coolant residue and adhesive from protective film all become finish defects that are attributed to the coater and caused upstream.
Cleanliness also has a shelf life. A passivated part handled without gloves and stored in a humid shop will not stay clean, and the finish that fails three weeks later is usually a handling problem rather than a process one. Packaging belongs in the specification for anything that leaves the building.
Blasting, deburring and passivation are usually priced as one preparation step. Splitting them across suppliers is how a part arrives clean and is contaminated again before it reaches the line.
Find the guide for your next decision
Follow the guide that matches the feature, failure mode or project decision you are working on.
Bead Blasting Stainless Steel: A Uniform Finish That Does Not Create Rust
Black Oxide on Stainless Steel: Activation, Color and Corrosion Reality
Blackened Steel Finishes: Oil, Wax and Sealer Options for Corrosion Control
Bead Blasting Aluminum: Avoiding Smearing, Peening and Dimensional Change
How does passivation stop stainless steel from rusting early?
Industrial Surface Finishing: Engineering Standards, Process Metallurgy, and Global Supply Chain Integration for Custom Parts
Bead Blasting: Uniform Matte Finishes for Precision Machined Parts
Surface Finish Standards: Engineering Guidance for Custom Metal and Plastic Parts
How should you choose deburring and finishing processes for better parts?
CNC Surface Finish: Ra Values, Measurement and Finishing Choices
5-Axis Tolerances and Surface Finish: What to Expect on Complex Surfaces
How to Machine Press-Fit Holes: Tolerance, Surface Finish, and Assembly
O-Ring Groove Design: Dimensions, Tolerances and Surface Finish
How to Measure Surface Roughness: Ra vs Rz and Profilometer Methods
Black Oxide vs Phosphate Coating for Steel Parts
Bead Blasting Media Types: Glass, Ceramic, Aluminum Oxide, and Steel Shot
Passivation Service: Specifying ASTM A967 and AMS 2700 Correctly
Citric vs Nitric Acid Passivation: Bath Choice, Cycle Time and Waste Handling
Black Oxide Coating: Hot vs Cold Processing and What to Specify
Glass Bead Blasting: Producing a Uniform Matte Finish Ready for Coating
Bead Blasting vs Sandblasting: Media, Profile and Finish Compared
Stringent Surface Finish Requirements: Turning a Ra Callout Into a Process
Passivation Services: Restoring the Oxide Layer on Stainless Steel
Knurling & Texturing: Designing Functional Surfaces for Prototyping and Custom Parts
Color and Finish Matching Across Prototypes and Production: From Pantone to Texture Samples
Industrial Surface Treatments: Selection, Fit and Inspection Guide
Surface Finish on Sealing Faces: Roughness, Lay and Defects That Need Separate Limits
Precision Surface Finish and Edge Rounding: Protect Functional Geometry During Finishing
Surface Roughness Lay Direction: Match Tool Marks to Sealing and Sliding Functions
Aerospace Surface Finish Masking: Protect Bores, Bonds and Electrical Interfaces
Surface Roughness Cutoff Length: Why Two Measurements Can Disagree
125 Surface Finish: Read the Units and Parameter Before Approving the Drawing
Finished Parts Inspection: Building a Plan the Parts Can Actually Pass
Before you release the project
- Define the function, environment and the question this batch must answer.
- Specify material grade, geometry, quantity, finish and the dimensions that control fit.
- Agree the inspection method and the evidence required to accept the parts.
- Record the drawing revision and approval before production begins.
Common planning questions
When should the finish be specified?
Before production. Film thickness, masking, substrate preparation and cosmetic requirements can change dimensions, conductivity and assembly fit.
Is one finish suitable for every alloy?
No. Substrate chemistry, condition and service environment influence preparation and compatibility. Specify the actual alloy and intended use.
Move from guidance to a reviewed project
Send the CAD model and drawing with material, quantity, finish and inspection requirements. Use the relevant service page to review the available manufacturing route.