
Manufacturing knowledge · 6CProto Guides
Engineering decisions, organised
Surface Finishing Guides
Specify the finish by its job: corrosion protection, conductivity, appearance, wear or cleanliness. Include thickness and masking where fit matters.
Updated October 11, 2026 · 63 focused articles
A finish is a process, not a colour
Two parts can look identical and behave completely differently, because the finish is a chemical or mechanical process with its own tolerances. Anodising converts the aluminium surface into an oxide layer, grows it inward and outward, and leaves a coating of roughly 5 to 25 micrometres depending on the class. Powder coating builds 60 to 100 micrometres per coat on top of the substrate. Electroplating deposits metal and can add tens of micrometres. Each one changes the dimension of the part, and each one changes it differently on edges, threads and bores.
That is why a finish callout belongs on the drawing with a thickness and a masked area, not in a note at the bottom. A thread that must accept a fastener has to be masked or plugged; a bore that carries a bearing cannot grow by 80 micrometres; a sliding fit that worked as-machined may not after coating.
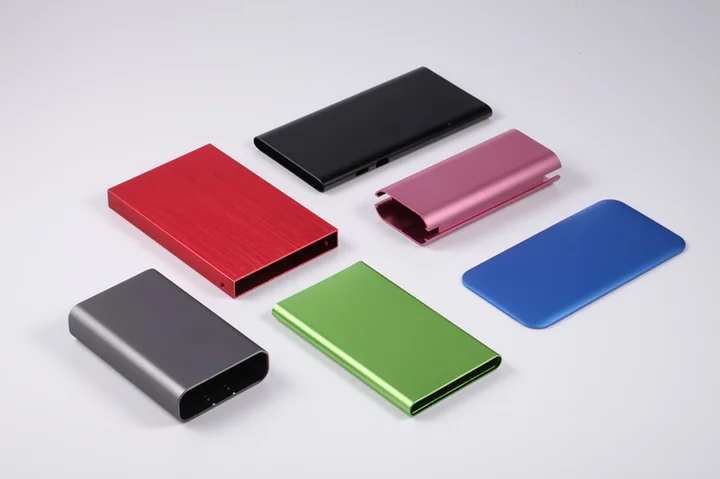
Specify the finish by the failure it prevents
A finish is easier to choose when it is tied to a failure mode. Corrosion on aluminium calls for anodising or a conversion coating; corrosion on steel calls for plating, passivation or paint. Wear on a sliding surface calls for hard anodising, electroless nickel or a coating with a defined hardness. Electrical conductivity calls for passivation or a conversion coating rather than an anodic layer, which is an insulator. Appearance calls for consistency — the same alloy, the same finish class and the same grain direction across every part in the batch, because anodised aluminium from two alloy lots will not match.
Where the requirement is cosmetic, say which faces matter. A finish specified across the whole part forces masking, handling and inspection on surfaces nobody will see, and it hides the fact that the visible face is the only one that needed the extra operation.
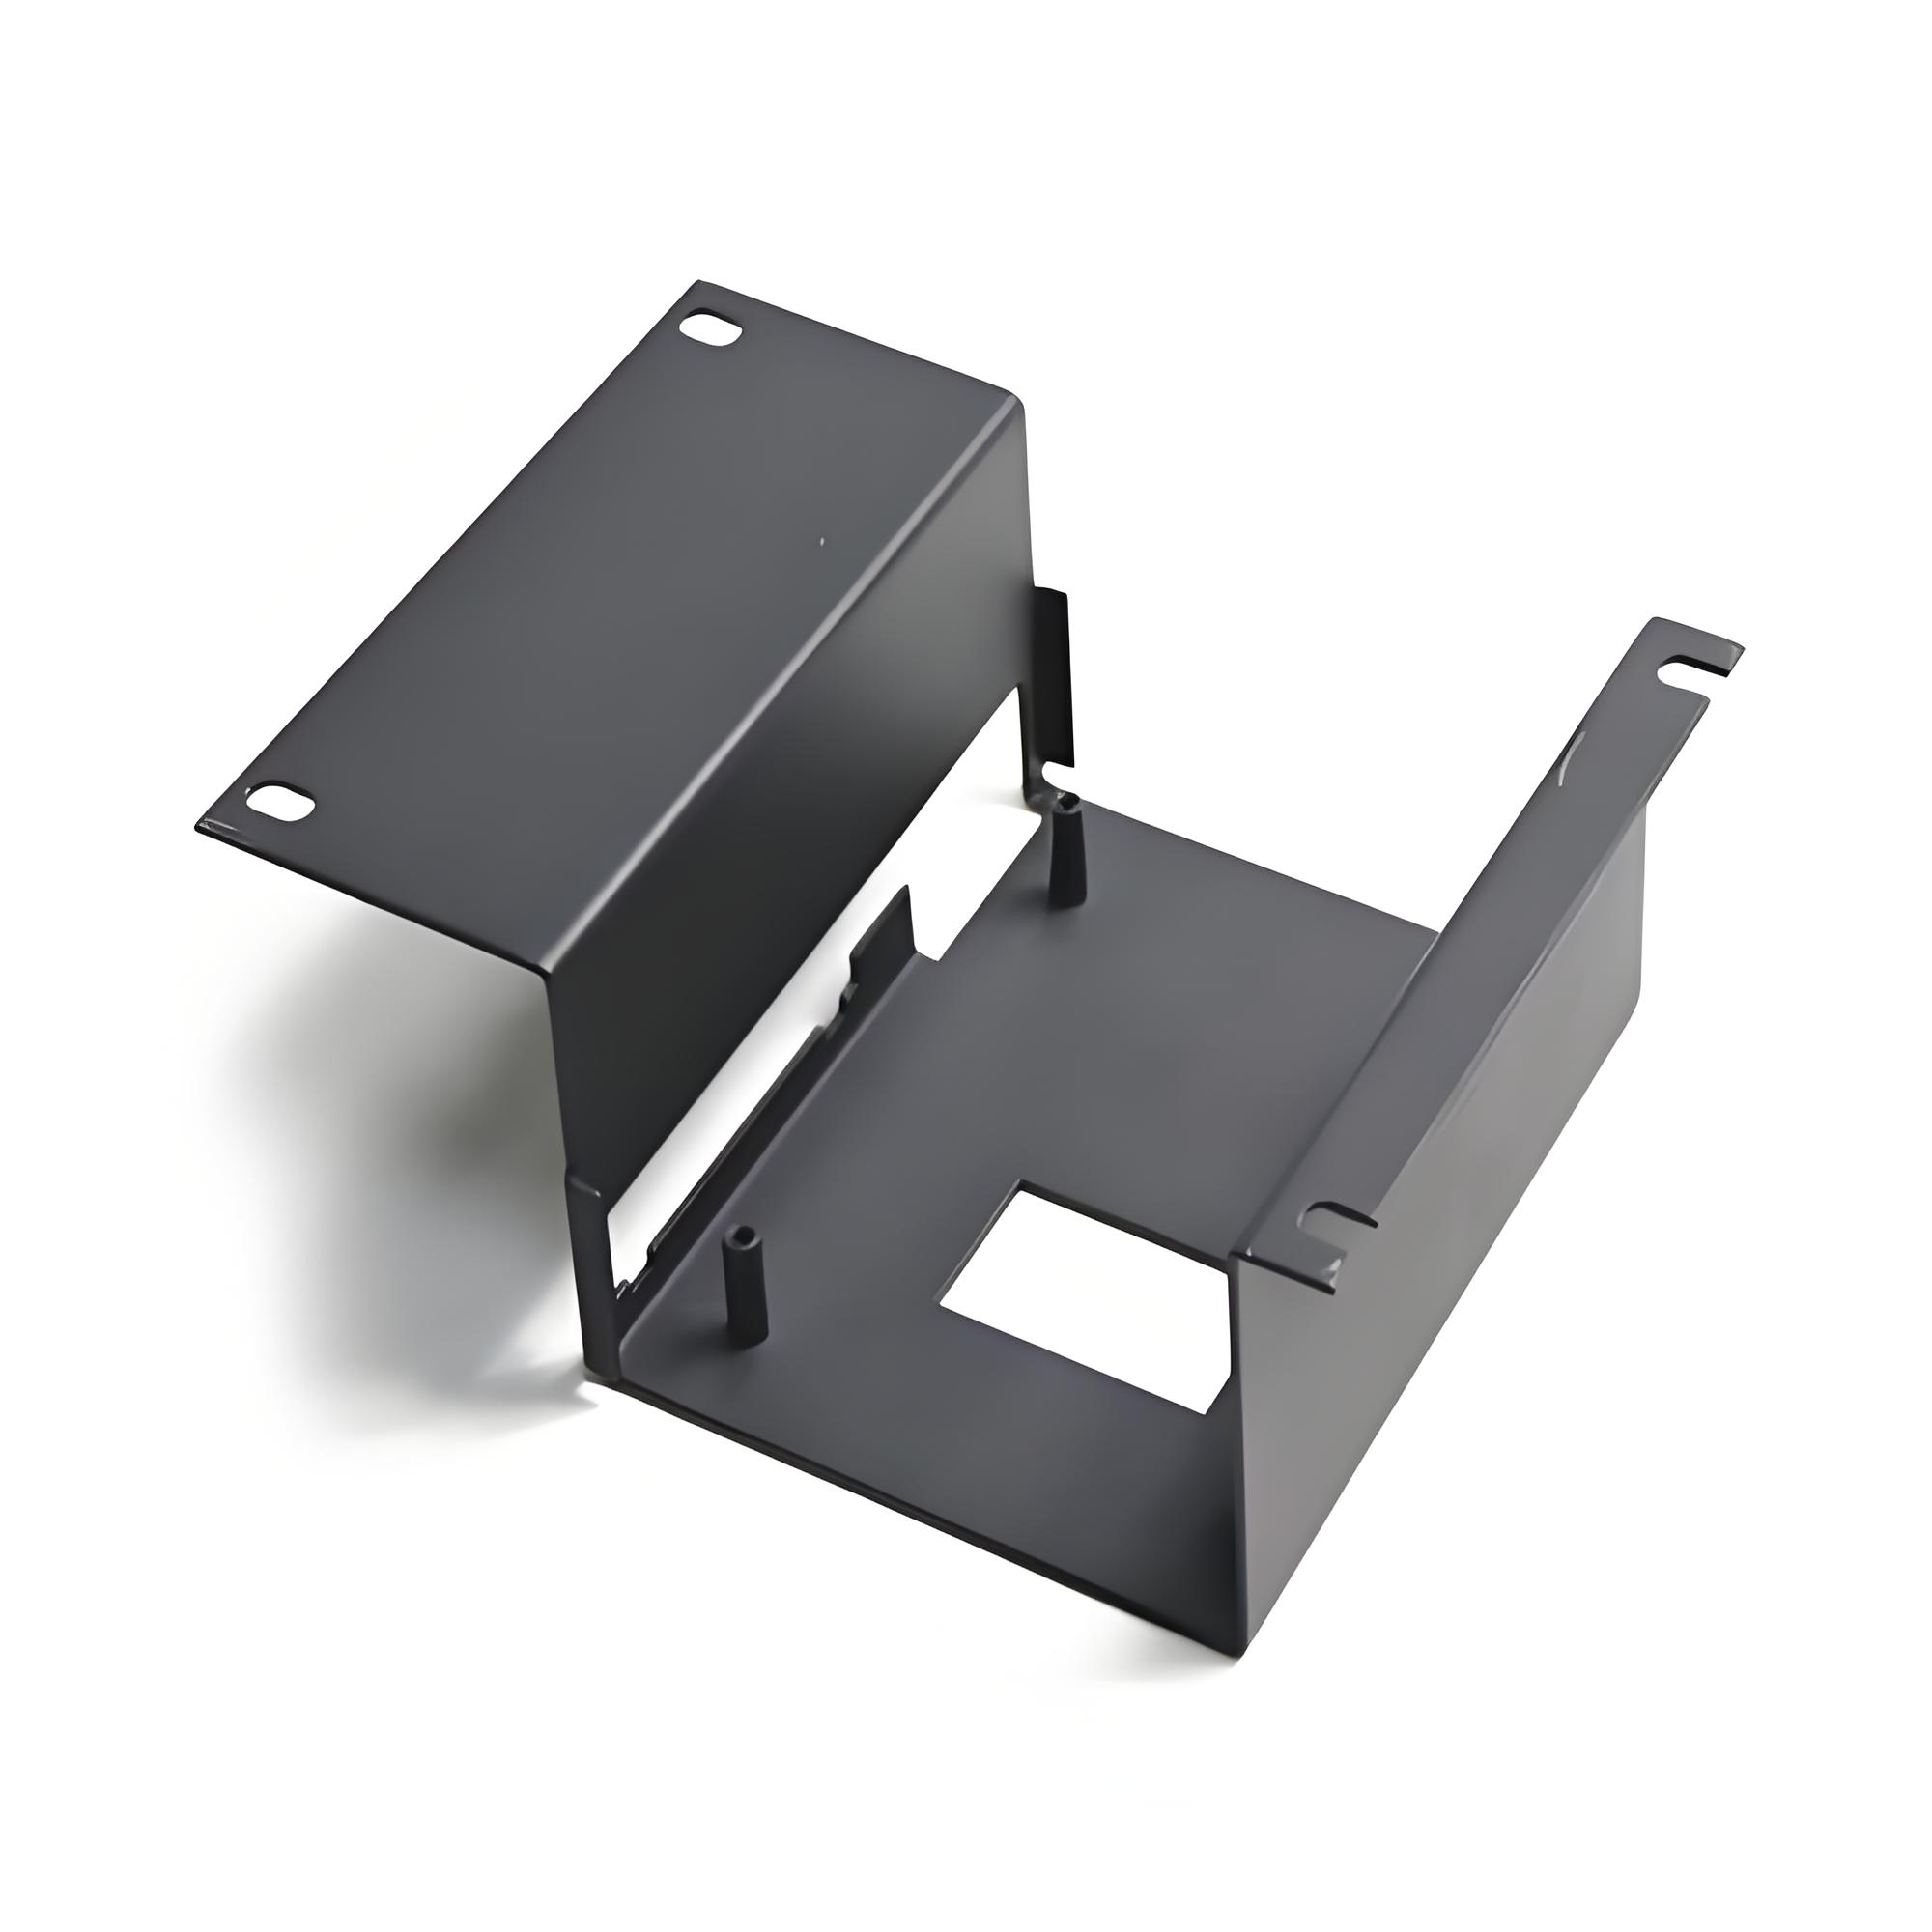
What finishing does to dimensions and lead time
Build-up is the dimension problem; handling is the schedule problem. Plating and coating usually run in batches at a specialist, add several days to the route, and add a masking step for every feature that must stay bare. Anodising and passivation are faster but still require the part to be clean, and contamination from machining coolant or fingerprints shows up as a patchy finish that has to be stripped and redone.
The practical rule is to finish the design before the finish is specified: decide which surfaces are functional, which are cosmetic, which must conduct, and which must stay within a tolerance after coating. Everything else can be left as-machined.
Masking, threads and post-finish assembly
Every finished part has features that must stay bare. Threads, dowel holes, bearing bores, electrical contacts and mating surfaces are masked, plugged or machined after coating, and each of those is a manual operation with its own cost and its own chance of error. A design that puts a thread at the bottom of a blind pocket and then asks for powder coating has created a masking problem that could have been avoided by leaving a plain land around the hole.
Assembly sequence matters as much. A pressed insert fitted before anodising will be anodised with the part and may no longer fit; a fastener torqued before painting has to be re-torqued after. Where the finish is cosmetic and the assembly is mechanical, the usual order is finish first, assemble second — which means the design has to tolerate the coating thickness at every interface.
How to write a finish callout that can be accepted
A useful callout names four things: the process and its standard, the class or thickness, the areas that are excluded, and the acceptance criteria. “Anodise to MIL-A-8625 Type II, Class 2, black, 10 to 15 micrometres, mask threads and bore A” is a specification. “Black anodised” is a wish, and it will be interpreted differently by every supplier who quotes it.
Acceptance is where most disputes start. Colour and gloss need a reference — a master sample, a RAL or Pantone number, a gloss unit range. Adhesion needs a test method and a pass level. Corrosion needs hours to failure in a named test. If none of that is stated, the finish is accepted on the supplier’s judgement, which is fine until two batches have to match.
Choose your starting point
Each route below owns a distinct part of the topic. Start with the decision you need to make, then use the focused articles within that route.
Anodizing, Conversion Films & Coatings
Compare anodizing, conversion films, powder coating and other coatings through substrate compatibility, thickness and the properties required after finishing.
Surface Preparation, Plating & Inspection
Compare mechanical preparation, plating and passivation around the substrate, finish standard, corrosion requirements and inspection plan.
Before you release the project
- Define the function, environment and the question this batch must answer.
- Specify material grade, geometry, quantity, finish and the dimensions that control fit.
- Agree the inspection method and the evidence required to accept the parts.
- Record the drawing revision and approval before production begins.
Common planning questions
When should the finish be specified?
Before production. Film thickness, masking, substrate preparation and cosmetic requirements can change dimensions, conductivity and assembly fit.
Is one finish suitable for every alloy?
No. Substrate chemistry, condition and service environment influence preparation and compatibility. Specify the actual alloy and intended use.
Move from guidance to a reviewed project
Send the CAD model and drawing with material, quantity, finish and inspection requirements. Use the relevant service page to review the available manufacturing route.