

Explore Surface Preparation, Plating & Inspection
bead blasting is the surface finishing process most often specified by two words and a smile, and most often rejected because the drawing never said what “matte” means. It is a controlled abrasion process that produces a uniform matte texture by blasting fine media at the part surface, and it is genuinely useful: it hides machining marks, improves paint and coating adhesion, and creates a consistent appearance across a batch. But whether the result is accepted depends on media, pressure, coverage, and what the part calls out. This article covers how bead blasting actually works, how it compares to other blasting and finishing routes, how it fits into a machining workflow, and what to specify so the finish can be measured and repeated.
What a Bead Blasting Finish Is
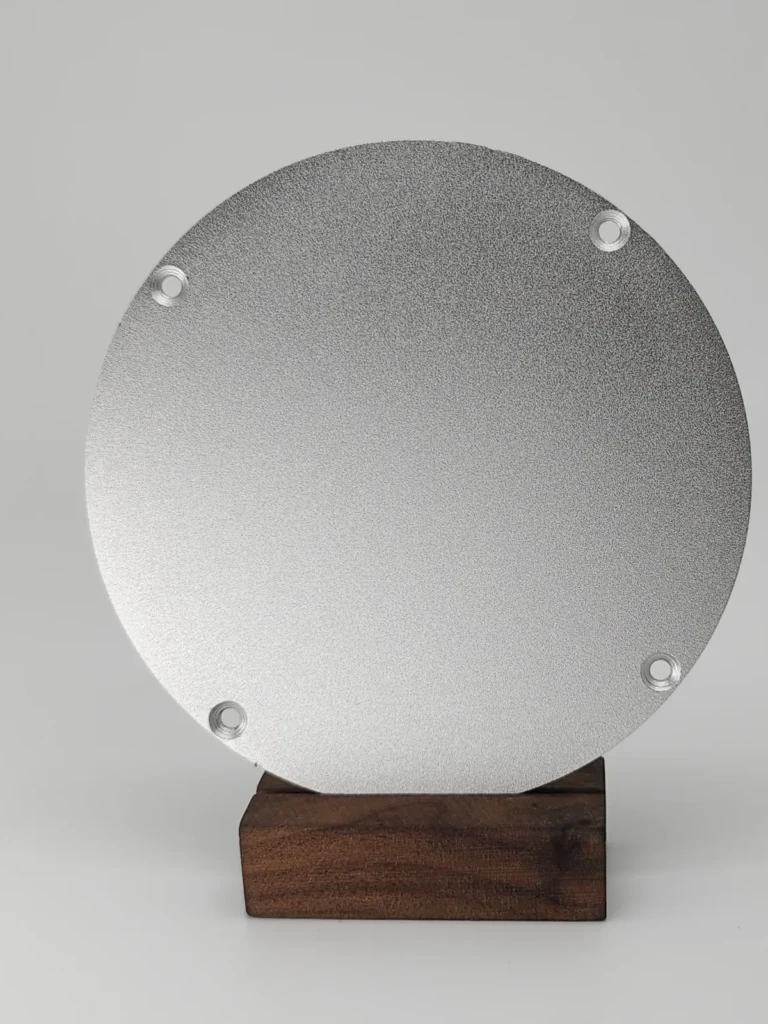
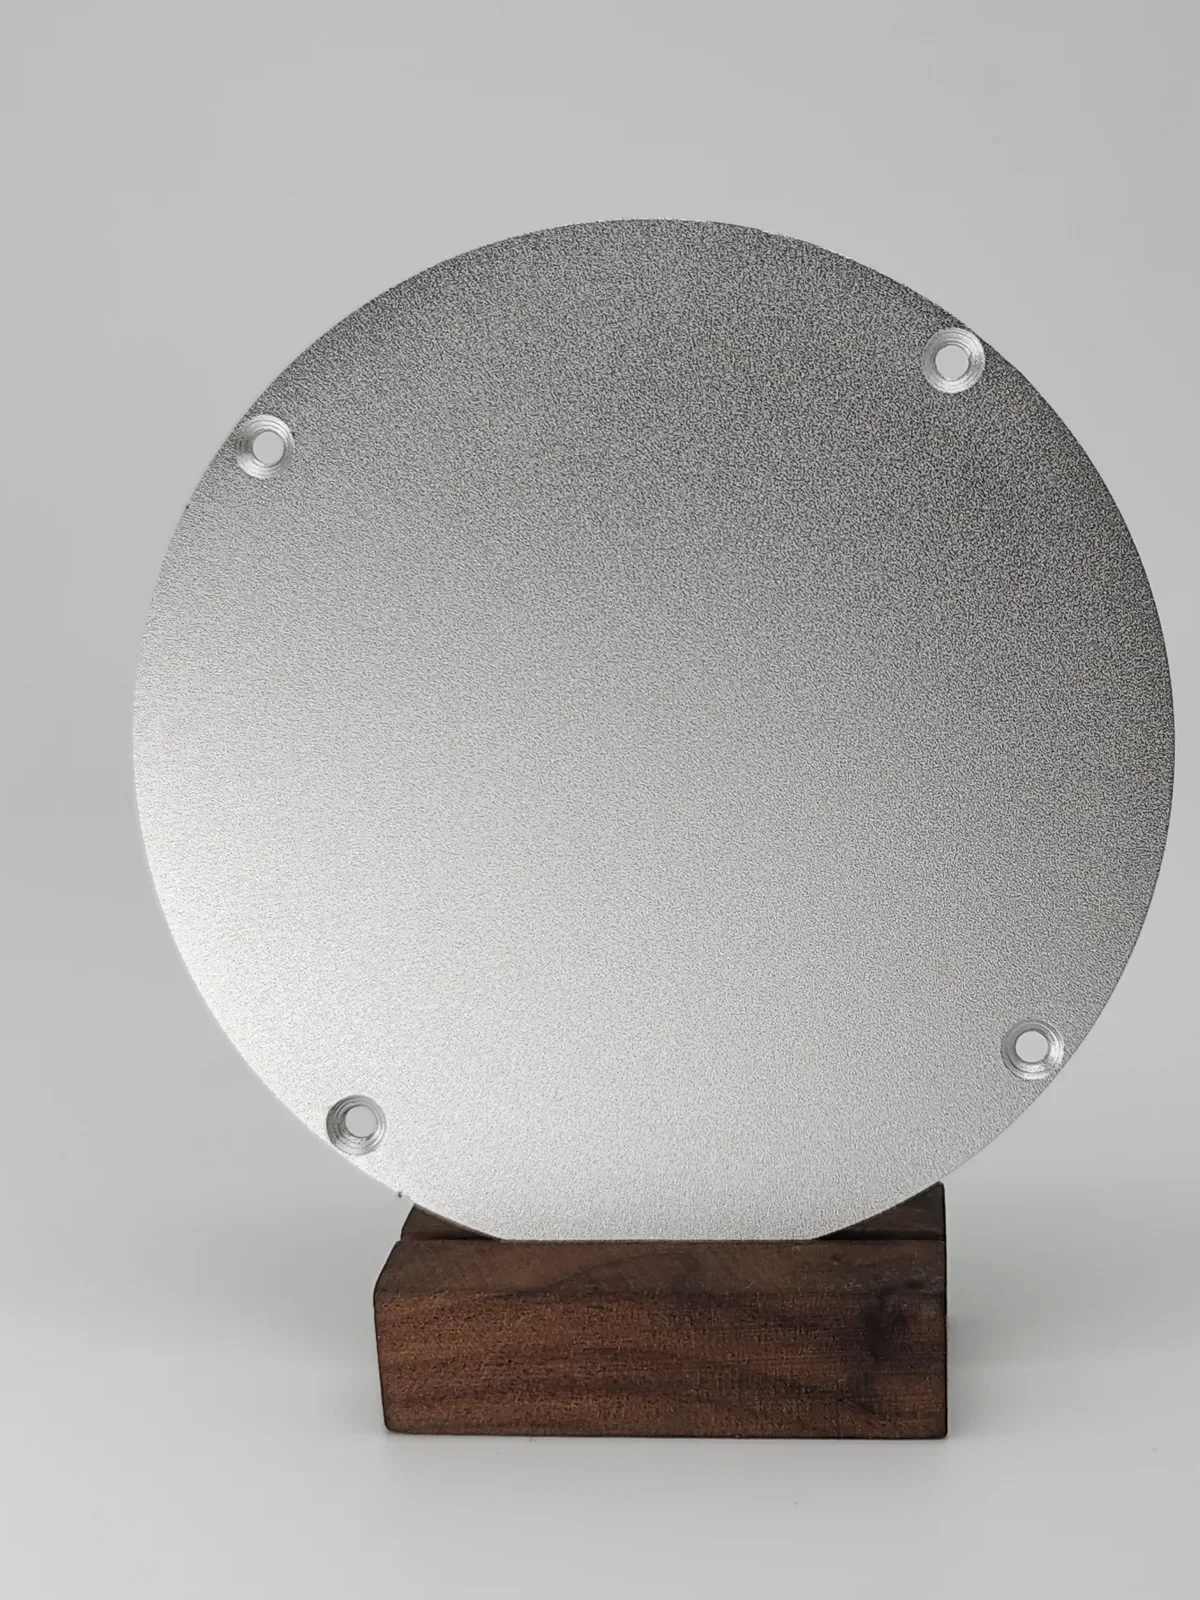
Bead blasting propels small spheres of media – glass beads are the common choice – onto the part surface under controlled pressure. Each impact creates a tiny, uniform dimple. The cumulative effect is a matte texture with no sharp directional scratches, which distinguishes it from sandblasting, whose angular media leaves a more aggressive, directional profile.
The finish’s signature is consistency: uniform dimples, even coverage, no chatter marks or machining streaks visible. That uniformity is exactly why it is used before painting and coating – the anchor profile helps coatings bond – and for cosmetic parts that need a repeatable, non-glare surface.
Why Choosing the Finish Is Harder Than It Looks
Three variables control the result, and all three must be set deliberately:
- Media type and size: glass beads for a fine matte, other media for coarser profiles.
- Pressure and nozzle distance: too little pressure leaves uneven coverage; too much can peen or distort thin features.
- Exposure time and coverage: even coverage is the goal, and thin walls or delicate geometry can bend under aggressive blasting.
A finish specified only as “bead blast” leaves every one of these decisions to the shop floor. The result may be fine; it may also be wrong for your part, and you will not know until first article.
Bead Blasting vs. Other Surface Routes
| Route | Characteristic | Typical use |
|---|---|---|
| Bead blasting | Fine, uniform matte, no directional scratches | Cosmetic matte, pre-coat anchor profile |
| Sandblasting | Aggressive, directional profile | Coarse cleaning, heavy anchor profiles |
| Brushing / satin | Uniform fine lines | Decorative semi-matte appearance |
| Machined / as-machined | Tool marks visible | Functional parts where finish is not specified |
The choice changes more than appearance: it changes surface roughness, which changes how the part is perceived, how coatings bond, and how the part handles in the hand.
How Bead Blasting Fits Into a Machining Workflow
Bead blasting usually comes after machining and before coating or assembly. Order matters: blast before anodizing or painting on metals where the coating will not hide the texture, and before assembly so the media does not lodge in threads or cavities. Parts with tapped holes, bearings, or sealed features may need masking or cleaning steps afterward.
Because blasting changes the surface microprofile, it can slightly change how a dimension is measured with touch probes. Tight fits should be inspected with this in mind, and critical dimensions should be confirmed before and after finishing where the finish touches the feature.
Specifying a Bead Blast So It Can Be Repeated
- State the target finish and the surface it applies to (all faces, or specified faces only).
- Where it matters, state an achievable roughness range and the standard used for measuring it.
- Note which features must not be blasted (threads, sealing faces, bearing seats) and require masking.
- Confirm whether tolerances apply before or after blasting on critical dimensions.
Use Cases That Fit Bead Blasting
- Machined housings and brackets where visible tool marks are unacceptable.
- Parts that will be powder coated or painted and need a consistent anchor profile.
- Hand-held consumer and industrial parts where grip and appearance both matter.
- Any design intent that calls for a repeatable, non-glare surface across batches.
The Bottom Line
Bead blasting delivers a uniform matte finish when the process is controlled and the spec is explicit. Choose it for the cosmetic or coating reasons it serves, define the media, coverage, and protected features, and measure the first article against the drawing. A bead-blasted finish that is repeated from drawing to delivery is a finish, not an accident.
Note: achievable roughness and texture depend on media, pressure, material, and geometry; confirm the finish on a sample before production.