

Explore 3D Printing Processes & Comparisons
3D printing has outgrown its reputation as a prototyping tool, but moving a printed part into end-use service is not automatic. The process that made the prototype now has to meet the material, strength, tolerance, and repeatability of a production part, and the choice between SLA, SLS, and MJF decides what that production part can be. Each process leaves a different imprint on the material: SLA cures resin with light, SLS fuses nylon powder with a laser, MJF fuses powder with inkjet-style jets of fusing agent. This article compares the three for end-use parts, the jobs each actually fits, and what has to be verified before a printed part earns its production label.
The Difference Between Prototype and End-Use
A prototype proves form, fit, and sometimes function under controlled conditions. An end-use part carries real load, environment, and repeatability requirements: the material must behave predictably in service, the part must hold its tolerance across the run, and the process must be reproducible. The transition from prototype to end-use changes what is verified. Strength, moisture and heat behavior, surface state, and batch consistency replace the quick geometry checks that a prototype needed. The printed part that is “good enough for the demo” is not necessarily good enough for the product.
SLA: Detail and Cosmetic End-Use
SLA produces the smoothest surface and finest detail of the three, which suits end-use parts where appearance or small features matter: housings, covers, handles, and parts that will be touched and seen. The trade is the material: photopolymer resin is generally more brittle than fused nylon, and sustained load, heat, and impact are limited. SLA is the right end-use choice where detail and finish govern and the mechanical duty is light. The part should be verified in the resin and processed for the surface before it ships, because the resin’s behavior and the finish are part of the part.
SLS: Functional Nylon End-Use
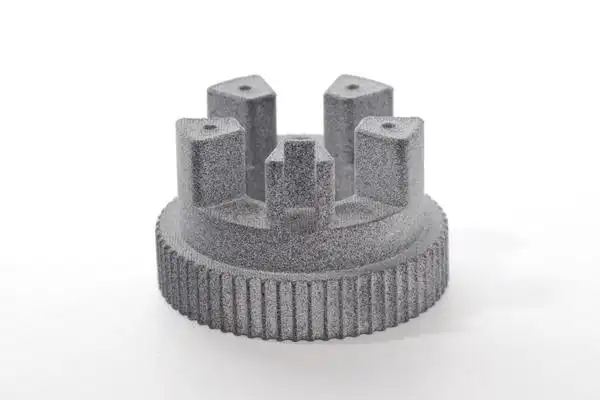
SLS fuses nylon powder into tough, functional parts without supports, which makes it the workhorse for end-use plastic parts that carry load: brackets, ducts, housings, clips, and low-volume production components. The sintered nylon is strong, impact-resistant, and can be drilled, tapped, and post-processed. The trade is surface and detail: SLS is rougher and coarser than SLA, so it suits function over finish. For parts that serve, not just present, SLS is often the honest end-use choice.
MJF: The Production-Speed Step Up
MJF uses inkjet-style jets to apply fusing agent to nylon powder, building parts faster than SLS with similar material properties. It produces functional nylon parts with good mechanical behavior, and its speed makes it practical for larger quantities and end-use runs. The surface is similar to SLS, so the part is verified on function, strength, and dimensional control rather than cosmetics. MJF is the process that carries printed nylon from a prototype oddity toward a repeatable production route.
What to Verify Before the End-Use Label
- Strength and fatigue in the printed condition, because printed properties differ from molded ones.
- Dimensional behavior: moisture, temperature, and the residual stress of the process.
- Layer and process consistency across the run, not just the first part.
- Surface state where the part is touched, sealed, or cleaned.
- Batch documentation if the part carries traceability or certification.
The verification list turns a promising printed part into an established end-use part, and it is the difference between shipping a part and shipping a hope.
Dimensional and Environmental Behavior
Printed parts carry the layer structure and the process’s residual stress, and nylon absorbs moisture, so the dimension and the strength change with the environment. An end-use printed part has to be specified for the environment it will live in: the temperature, the humidity, the load, and the duration. The drawing states the measurement basis and the environment, and the first article and the batch are verified against it, because a part that is dimensionally right at the printer and wrong in the field is a part that failed its service spec.
Picking the Process by the Part’s Job
Choose SLA for detail and cosmetic end-use, SLS for tough functional parts at reasonable quantity, and MJF for functional nylon at higher speed. The decision follows the part’s job first, then the material and detail trade, then the volume and cost. A housing that must look good is an SLA part; a bracket that must carry load is an SLS or MJF part. The process that fits the duty is the process that earns the production label, and the quote should reflect the choice, not a default.
Bottom Line
SLA, SLS, and MJF take 3D printing beyond prototypes when the process and the material match the end-use duty: SLA for detail and finish, SLS for tough functional nylon, MJF for faster functional production. The transition from prototype to end-use changes the verification from form to strength, dimensional stability, and batch consistency. Verify the printed-condition properties, specify the environment, and document the run. A printed part becomes an end-use part when it is proven to serve in service, not when it survived the demo.
Related Capabilities and Turning the Advice Into an Order
The discipline in this article holds best inside a wider capability set, where the drawing, the datum, and the inspection travel with the part across the program. The 3D printing SLA pages cover the service scope and the tolerances that apply, and the first article ties the design to the measured result. The concrete next step is to send a drawing with the critical features and the datum stated, ask for the DFM review, and request the first-article report with values, so the advice becomes a controlled order instead of a good idea.
Post-Processing the End-Use Printed Part
An end-use printed part is rarely ready at the printer. Support removal, sanding, dyeing, and coating turn it into the finished product, and each step carries its own time and tolerance. The post-processing also affects the surface that wears, seals, or is seen, so the finish target and the process are part of the part spec. A printed enclosure that is coated and sanded presents and protects differently from one shipped as-printed. Define the finish at RFQ, confirm the post-processing schedule, and let the first article carry the finished surface. The print is the blank; the post-processing is the part.
Sizing the End-Use Program to the Process
The end-use decision includes the route economics. SLA and MJF are detail- and speed-driven; SLS is tough-functional; and each process has a cost floor tied to the machine time and the post-processing. The quantity and the part’s mechanical duty decide which route pays, and the quote should show the per-part cost at the real volume. A printed end-use part is chosen when the process and the part’s job align, not when the prototype was convenient. The economics are part of the material decision.
Interpreting the Mechanical Data of a Printed Part
A printed end-use part is verified on its printed mechanical behavior, not the data sheet of the raw material. Print orientation, layer adhesion, and porosity change the strength, and the datasheet does not predict the printed condition. Test the part or a coupon in the printed state, at the service load, and the result is the honest number. The difference between the resin’s datasheet and the printed part is the whole reason the verification exists. A part chosen and tested in its printed condition is a part whose limits are known.
The Printed Part in Its Final Finish
The end-use printed part is finished before it ships: the supports removed, the surface sanded, the dye or coating applied, and the part inspected. The finish changes the surface that wears, seals, and is judged, so it is part of the part spec, and the finishing time is part of the lead time. A printed enclosure with a sanded and coated surface presents and protects differently from one shipped as-printed. Define the finish at RFQ, and let the first article carry the finished appearance. The print is the blank; the finish makes it a product.
The Data Sheet That the Printed Part Ignores
Printed parts do not obey the resin data sheet by default; the printed condition changes the properties with the layer structure, the orientation, and the porosity. The end-use decision should rest on data from the printed state, tested at the service load, not on the raw material's brochure. A part chosen and tested in its printed condition is a part whose limits are known after the fact rather than discovered in the field. The data sheet is the starting point; the printed verification is the number that matters. Confirm the printed-condition data before the part serves.
The Volume Decision Inside the End-Use Choice
The end-use decision includes the volume: a printed part at tens or hundreds is a production route, at thousands it may yield to molding or machining. The quote shows the per-part cost at the real quantity, and the break-even against the other routes. A printed end-use part chosen at the volume where it is economical is the right choice; one stretched past its economics is a choice the cost will revisit. The volume is part of the material and process decision, and it belongs in the RFQ. The route and the quantity are decided together.
Related Capabilities and Guides
For the service scope and the material and tolerance details behind this article, see the 3D printing services, the SLS printing, and the MJF printing. The first article of your order ties the design to the measured result, and the same drawing, datum, and inspection discipline carry across the program.