
What Is SLA 3D Printing?
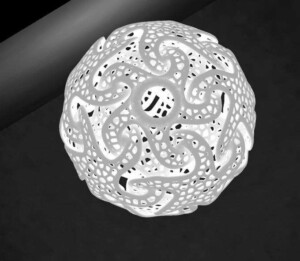
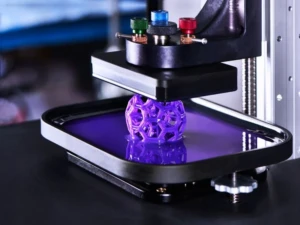
SLA (stereolithography) is a vat photopolymerization process that uses an ultraviolet laser to cure liquid photopolymer resin layer by layer. It produces parts with smooth surfaces, sharp features, and fine details, making it ideal for appearance models, form-and-fit testing, master patterns, and complex prototypes.
Compared with FDM and SLS, SLA is typically selected when surface quality, dimensional accuracy, and small-feature resolution are the main priorities. After printing, each part is cleaned and post-cured, with optional sanding, polishing, painting, clear coating, and other finishing services available.
Explore SLA 3D Printing Services and Resources
Review SLA materials, dimensional capabilities, finishing options, design guidelines, applications, quality controls, and frequently asked questions to plan your project with confidence.
How Our SLA 3D Printing Process Works
How Our SLA 3D Printing Process Works
From file upload to finished SLA parts in four clear steps.
Why Choose 6CProto for SLA 3D Printing?
From detailed appearance models to functional prototypes and low-volume resin parts, 6CProto combines high-resolution SLA printing, engineering support, flexible finishing options, and quality inspection to help bring your designs to life.
Quality Assurance for SLA 3D Printed Parts
Every SLA project is reviewed from file preparation through final inspection to help ensure dimensional accuracy, surface quality, and consistent results.
Engineering Review Before Printing
Our engineers review part geometry, minimum wall thickness, supports, print orientation, dimensional tolerances, resin selection, and finishing requirements before production begins.
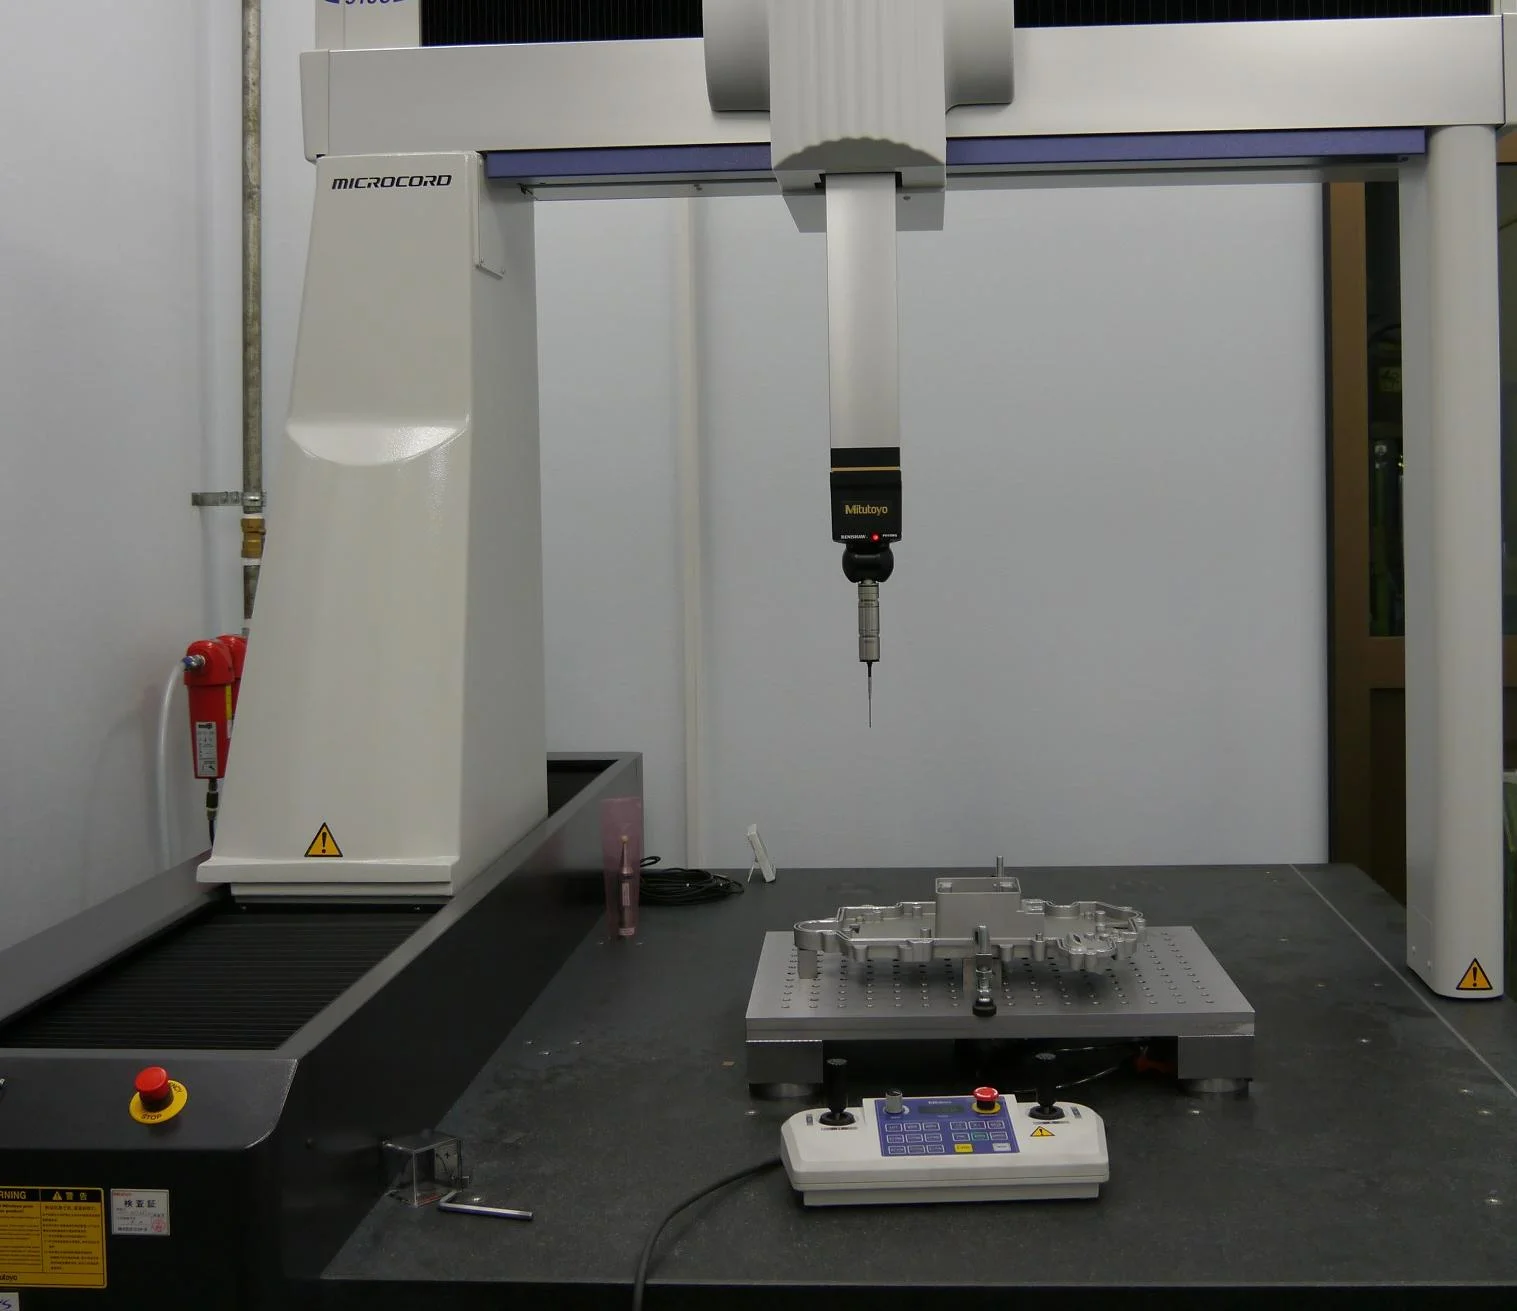
In-Process and Final Inspection
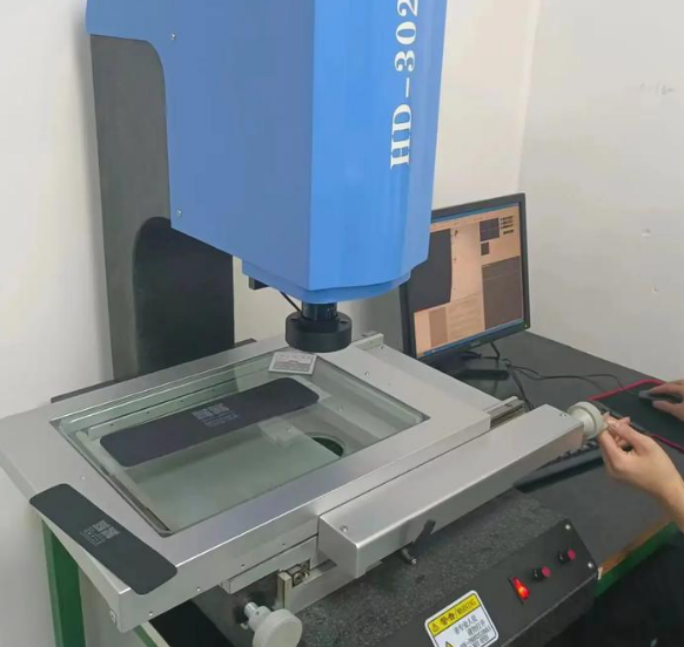
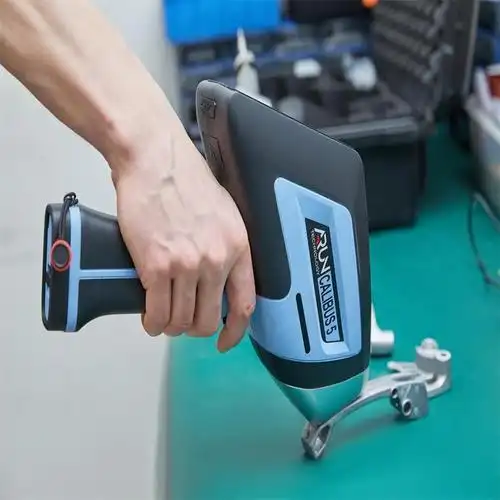
SLA parts receive visual inspection after printing, cleaning, and UV post-curing. Critical dimensions can also be checked against approved drawings or specified project requirements.
Documented Quality Controls
- File and manufacturability review before production
- First-article inspection when required
- Visual and dimensional quality checks
- Final inspection before packaging and shipment
- ISO 9001:2015 quality management controls
SLA 3D Printing Materials
Choose from general-purpose, tough, heat-resistant, and translucent SLA resins for detailed prototypes, appearance models, functional evaluation parts, and low-volume production. The most suitable resin depends on the required surface finish, durability, temperature resistance, transparency, and intended application.
SLA 3D Printing Capabilities
Review our standard SLA printing specifications for build size, wall thickness, layer resolution, tolerances, materials, lead time, and finishing. Final achievable specifications depend on part geometry, resin selection, print orientation, dimensions, and surface requirements.
| Parameter | SLA Capability |
|---|---|
| Printing Process | SLA — Stereolithography |
| Available Materials | General-purpose, tough, heat-resistant, and translucent photosensitive resins |
| Maximum Build Size | 2100 × 1000 × 700 mm |
| Minimum Wall Thickness | 0.4–0.6 mm |
| Layer Thickness | 0.025–0.1 mm |
| Design Tolerance | ±0.05 to ±0.1 mm |
| Standard Lead Time | Approximately 5 days, depending on quantity, complexity, and finishing |
| Recommended File Formats | STEP, STP, STL, SLDPRT, IGES, IGS, and other common 3D CAD formats |
| Available Finishing | Sanding, polishing, painting, clear coating, plating, and custom cosmetic finishes |
Note: Final tolerance, wall thickness, lead time, and finish depend on part size, geometry, resin, quantity, and project requirements. Upload your CAD files for an engineering review.
SLA Surface Finishes and Post-Processing
Improve the appearance, durability, and functionality of SLA printed parts with professional cleaning, post-curing, sanding, polishing, painting, clear coating, plating, and custom cosmetic finishing.
Support Removal & Cleaning
After printing, temporary supports are carefully removed and parts are cleaned to eliminate residual resin before curing and inspection.
UV Post-Curing
Controlled UV post-curing helps the printed resin reach its intended mechanical properties, surface condition, and dimensional stability.
Sanding & Polishing
Sanding and polishing reduce support marks and improve surface smoothness for display models, master patterns, and visual prototypes.
Painting & Color Matching
After surface preparation, parts can be painted using a specified color or Pantone reference to meet cosmetic and branding requirements.
Clear Coating
Clear coating improves the cosmetic finish and can enhance the appearance of translucent or clear SLA resin components.
Plating & Custom Graphics
Electroless nickel plating, decals, logos, and other custom graphics may be applied when required by the project.
Finish availability depends on the selected resin, part geometry, surface condition, and project requirements.
Common Applications of SLA 3D Printing
SLA 3D printing is commonly selected when smooth surfaces, fine details, complex geometries, and accurate visual presentation are more important than the mechanical strength of production thermoplastics.
Appearance Models
Smooth surfaces and fine details make SLA suitable for presentation prototypes, styling models, trade-show samples, and visual design reviews.
Form-and-Fit Testing
Produce accurate housings, covers, connectors, and assemblies to evaluate dimensions, clearances, interfaces, and ergonomics before tooling.
Master Patterns
Create detailed master patterns for silicone molding, vacuum casting, investment casting, and other part replication processes.
Complex Prototypes
Build internal channels, thin features, organic shapes, lattice-like structures, and other geometries that may be difficult to produce by machining.
Medical & Dental Models
Create anatomical models, planning aids, dental demonstration models, and non-implant medical device prototypes using project-appropriate resin.
Low-Volume Resin Parts
Manufacture small quantities of customized covers, fixtures, display components, and specialized resin parts without injection mold tooling.
Material, tolerance, finishing, and inspection requirements should be selected according to the intended application.
SLA Design Guidelines for Better Parts
Good SLA results begin with a printable design. Use these guidelines to reduce distortion, support marks, trapped resin, assembly problems, and unnecessary post-processing.
Recommended Design Practices
- Maintain printable walls: Use a minimum wall thickness of approximately 0.4–0.6 mm, depending on resin, geometry, and part size.
- Hollow large parts: Hollowing can reduce material use, but suitable drain and vent openings must be included to prevent trapped resin.
- Identify visible surfaces: Tell us which surfaces are cosmetic so supports and contact points can be positioned appropriately.
- Allow assembly clearance: Include suitable clearance between mating parts to account for printing tolerances, curing, and finishing.
- Use fillets and gradual transitions: Rounded corners and gradual thickness changes can reduce local stress and distortion.
- Provide critical dimensions: Upload a 2D drawing when specific tolerances, fits, threads, or inspection points are required.
Common Design Issues to Avoid
- Fully enclosed cavities: Closed internal spaces can trap uncured resin and make cleaning impossible.
- Extremely thin unsupported features: Long, delicate walls and pins may deform or break during printing and cleaning.
- Large unsupported flat surfaces: Broad flat areas may require orientation changes or additional support to control distortion.
- Sharp internal corners: Sudden transitions can concentrate stress and increase the risk of cracking in brittle resin.
- Zero-clearance assemblies: Parts designed with no allowance may bind after printing, curing, or surface finishing.
- Unspecified cosmetic requirements: Clearly communicate required color, gloss, transparency, visible surfaces, and acceptable support marks.
Need more guidance? Read our
common 3D printing design mistakes and solutions guide →
What Customers Say About 6CProto
SLA 3D Printing FAQs