

Explore 3D Printing Processes & Comparisons
The two quotes look close enough that the decision gets deferred to whoever is available, and the part is then printed in a process that cannot answer the question the test was written to answer. SLA and SLS overlap on cost for small quantities and on lead time for simple geometry, which is exactly why the choice has to be made on the property that matters rather than on price. This comparison is written for engineers who already know both processes exist and need the decision criteria: where resin detail stops being an advantage, where nylon durability starts carrying risk, and how to compare the two fairly before committing a build. Where three processes are in play rather than two, the wider trade-offs between extrusion, resin, and powder bed are covered in the FDM, SLA, and SLS comparison.
Which process is more accurate, SLA or SLS?
SLA resolves finer detail; SLS holds size across a batch.
Resin printing reproduces small features and smooth surfaces that powder beds round off, while SLS avoids the support marks and post-cure shrinkage that move a resin part after the build.
The two processes miss nominal in different ways, so the question of accuracy has no single winner. SLA draws each layer with a focused light source, which allows fine walls, sharp internal corners, and small text. The errors that follow come from curing: photopolymer shrinks as it crosslinks, the shrinkage follows the build direction, and post-curing continues to move the part after it leaves the machine. Support contacts also leave marks exactly where a part is most likely to be measured.
SLS fuses powder in a heated bed with no supports, so a part has nothing to remove and nothing pulling it out of position during the build. Its limits are resolution rather than repeatability: the powder particle size sets a floor on fine detail, small holes and thin ribs can partially fuse, and surfaces arrive with a matte texture that requires blasting or machining to look finished. Across a batch, though, that same stability is what lets a nylon part be ordered again months later and still fit its mating component.
For a drawing with tight tolerances on a small number of features, resin usually wins the feature and loses the assembly. For a drawing that defines interfaces across several parts, nylon usually assembles more reliably even when the surface looks rougher. Both statements assume the callouts are measurable at prototype quantity, which is the framework set out on the standards and tolerances page.
| Attribute | SLA (resin) | SLS (nylon powder) |
|---|---|---|
| Fine features and text | Reproduces small detail and thin walls | Rounds detail at the powder particle scale |
| Surface as built | Smooth but stepped on angles, with support marks | Uniform matte texture, no support marks |
| Dimensional behaviour over time | Moves with post-cure and can creep under load | Stable after cooling; no curing step |
| Support structures | Required, and removed by hand | Not required; powder supports the part |
| Typical role | Appearance, fit, flow, optical parts | Functional parts, fixtures, end-use nylon |
How does part geometry decide the process?
Geometry votes before cost does.
Enclosed volumes, deep internal channels, and fine lattices favour powder bed because there is nothing to remove afterwards, while large flat cosmetic faces and thin optical sections favour resin.
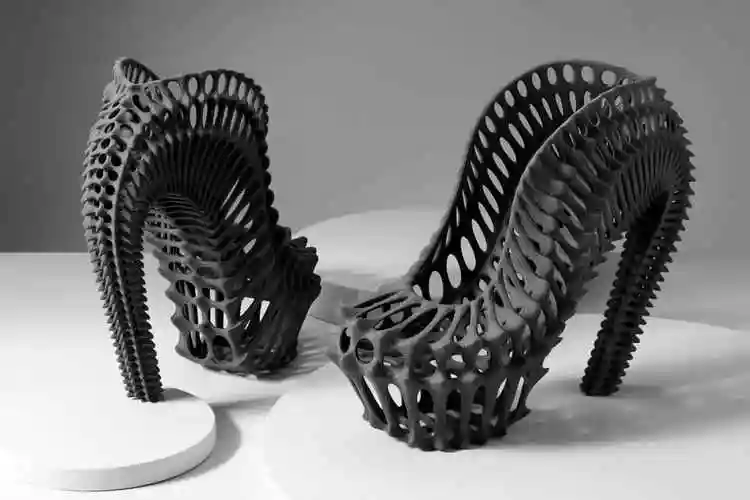
Powder-bed printing removes one entire class of design constraint: unsupported geometry. Overhangs, internal lattices, and nested features build without support structures because the un-sintered powder holds them in place. That is why lattice structures and complex manifolds are usually quoted in SLS nylon rather than resin, where every overhang needs a support that must later be cut away from a surface that may not tolerate the scar.
Resin moves the constraint rather than removing it. Deep pockets and internal channels are printable, but trapped uncured resin has to drain and cure, which puts a practical limit on enclosed volumes. In exchange, resin handles the geometry that powder beds struggle with: very thin walls, large smooth curved surfaces, and features that must read sharply in a photograph or an airflow path.
Two practical checks settle most geometry questions before a quote is requested. First, ask whether any surface that must stay cosmetically perfect also needs a support in one process and not the other. Second, ask whether any internal volume will trap material. If the answer to either question is uncomfortable, the alternative process is worth pricing even at a higher unit cost.
How do the cost curves differ?
Resin prices by machine time; nylon prices by bed volume.
A single resin part carries its whole build, while powder-bed parts share the bed, so the cost gap narrows sharply as quantities rise and disappears once the same geometry can be nested efficiently.
Resin cost scales with the height of the part and the number of layers, because one build usually serves one client’s parts. Supports add material and hand work. The result is that a single complex resin part can cost more than a nylon equivalent, even though the material itself is not expensive.
Powder-bed cost scales with the volume of the build chamber and the packing efficiency inside it. Parts that can be stacked and nested share the machine time, and the same powder that supports the geometry also fills the gaps between parts. At low quantities the difference is modest; at a few dozen identical parts, packing usually decides the quote.
| Cost driver | SLA | SLS |
|---|---|---|
| Primary unit | Build height and layer count | Bed volume and packing density |
| Support material | Yes, plus removal labour | None |
| Batch effect | Small parts share a build | Strong; dozens of parts can share a bed |
| Hand work | Sanding, polishing, support scars | Blasting, dyeing, sealing |
| Reprint risk | Higher where specs are incomplete | Lower across repeat batches |
Which mechanical behaviour matters in service?
Resin behaves stiffly; nylon deforms and recovers.
Resin takes a load, then cracks when it is exceeded; nylon bends further before failing, survives impact better, and is less sensitive to the direction of the load.
The distinction matters because prototypes are usually tested to a failure criterion rather than to a strength value. A housing that must survive a drop test is testing impact energy, where nylon’s elongation gives it a clear advantage. A bracket that must hold a static load without deflecting is testing stiffness, where the comparison depends on the resin grade chosen and the orientation it was built in.
Resin parts also change under sustained load. A constant stress held for weeks can produce creep that a short test never reveals, which is why a resin prototype can pass a static check and still distort in service. Nylon is not immune to this, but it tolerates more strain before the deformation becomes visible.
Temperature belongs in the same conversation. Resins are available in high-temperature grades that hold shape after post-cure, and those grades are appropriate close to warm electronics. Where a part lives at elevated temperature for long periods, though, the thermoplastic route has more room, and the property data behind it is published per grade by powder-bed equipment and material suppliers such as EOS and 3D Systems. The measurement and qualification work behind those published properties is coordinated through the NIST additive manufacturing program.
How do finishing and post-processing differ?
Resin finishing removes material; nylon finishing treats it.
Sanding and polishing remove material from a resin part to reach a surface, while blasting and dyeing treat a nylon part without changing its geometry much.
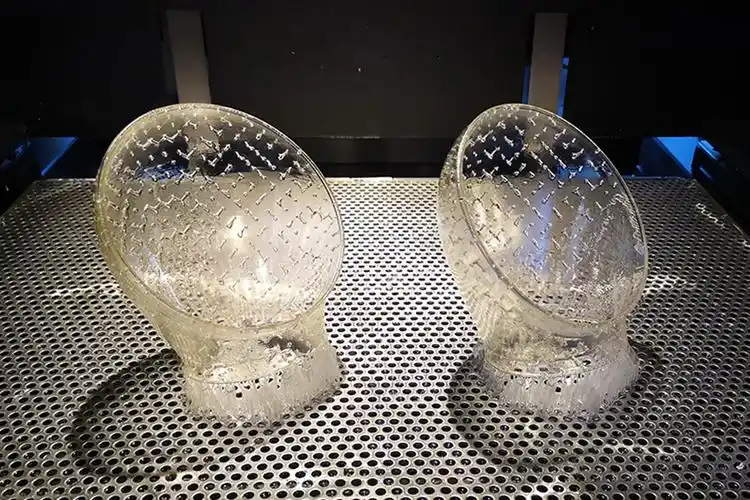
Resin post-processing, as run in a service such as SLA resin printing, starts with support removal, which leaves witness marks, then moves through progressive sanding and, for clear or glossy parts, polishing. Every step takes material from the surface, so dimensions move. That is not a defect; it is a process characteristic that has to be budgeted on the drawing, especially on bores and press fits.
Nylon parts arrive with a uniform matte texture. Media blasting cleans and evens that texture, dyeing introduces colour that penetrates the surface rather than coating it, and sealing closes porosity where a part will see fluid or pressure. A machined interface is common where a nylon part must meet a tight tolerance, which is a normal hybrid route rather than a rework.
For parts that must look identical in a set, nylon has the advantage: blasting and dyeing treat a whole batch in the same way, whereas hand polishing produces variation between parts. For a single part that must look smooth and glossy, resin has no equivalent in the powder bed.
Which process holds up for repeat orders and low-volume production?
Nylon repeats reliably; resin needs a frozen recipe.
A repeat nylon batch depends on powder grade and build parameters, while a repeat resin batch depends on the same grade, orientation, and finishing sequence being used again.
This is the gap that most comparison articles leave open, and it decides the second order rather than the first. With powder bed, the material is a documented grade and the process is largely automatic: parts coming off the same parameters in the same machine behave the same way, which is why SLS and MJF are used for bridge production rather than prototypes alone. The supplier documentation for the powder-bed platforms used in that work, including HP Multi Jet Fusion, describes how the build parameters and material grades are controlled.
Resin production at low volume is entirely possible, and 6CProto runs both processes in-house, which means the choice does not force a change of supplier. It does require discipline. If the second batch is built at a different angle, finished by a different hand, or printed in a visually identical but different resin, the parts will differ in ways a drawing may not capture. Recording orientation, support strategy, and finishing recipe against the part number is what makes a resin repeat order a repeat.
Where parts are needed across several months in small quantities, the usual pattern is to make the dimensional decisions in nylon and use resin for the appearance and fit iterations around it.
How should the DFM review change with the process?
Each process needs a different DFM review.
Resin reviews focus on orientation, support placement, and drain paths; powder-bed reviews focus on wall thickness, minimum feature size, and how the part will be nested in the bed.
A resin DFM review is mostly about protecting surfaces. Which faces must avoid supports, where can the part be rotated to hide layer steps, will uncured resin drain from internal volumes, and does the finishing budget allow the removal that polishing requires. Getting those answers wrong produces a part that is dimensionally right and cosmetically unusable. The mechanics behind those rules are documented in the Formlabs SLA printing guide.
A powder-bed review is mostly about the geometry that survives the process. Whether thin ribs will distort during cooling, whether small holes will fuse closed, whether the part’s tallest section adds unnecessary build height, and how neighbouring parts in the bed affect cooling and dimensional spread. The design tips library covers the shared rules, and the physical basis for separating process families follows the terminology and process categories maintained by standards bodies such as ASTM committee F42.
What does a side-by-side validation build look like?
One geometry, two processes, one test that can fail.
Print the same file in resin and nylon, agree in advance what the test must prove, and let that single criterion decide rather than comparing overall impressions.
A useful validation build costs more than one part and far less than a wrong tooling decision. Send the identical model to both processes, then test the property that the design depends on: drop the assembly, load the bracket, cycle the latch, or assemble the stack of parts and measure the stack-up. Appoint one failure criterion before the parts arrive, because a comparison run after the results is a comparison that will be argued.
Two outputs are worth keeping from that build beyond the pass or fail result. The first is dimensional data from the mating features in both materials, which is the evidence a production decision needs. The second is the orientation and finishing record for the winning process, since it becomes the reference for every repeat order.
Where both parts pass, the tie-break is normally the property that is hardest to control: colour and appearance consistency, thermal behaviour in service, or the ability to order the same part again without a new review.
Turning the comparison into a decision
The decision rarely turns on accuracy alone. Resin gives finer detail, smoother surfaces, and clear parts, at the cost of support marks, post-cure movement, and hand finishing that changes dimensions. Nylon gives impact tolerance, thermal stability, and batch consistency without supports, at the cost of surface texture, rounded fine detail, and design rules that the geometry must respect.
Sorting the requirements into those three columns typically resolves the choice in a single pass. Where the part is judged by how it looks or how precisely a feature reads, resin is the tool. Where the part is judged by how it survives, how it fits after a month, or whether the fifth batch matches the first, the powder bed is the tool. When both are true, running one geometry through both processes is cheaper than arguing about it.
FAQ
Can SLA parts be used for functional testing?
They can, with the right grade and orientation, but the test has to match the material’s behaviour. Resin is well suited to fit checks, flow visualization, and short-term structural loads. It is less suitable where the part sees impact or a load held for weeks, because creep can distort a part that passed a static check. Choose a tough or high-temperature grade, orient the part so the highest stress does not cross the layer plane, and state the service condition in the request.
Which process suits living hinges and snap fits?
Snap fits usually work in both, provided the resin grade has elongation and the orientation does not place the flexing feature across the layer plane. Living hinges are a harder case: they depend on repeated flexing and are sensitive to molecular orientation, so an unfilled nylon is normally the safer choice and is the standard material for hinges in production parts. Prototype a hinge in nylon even when the rest of the assembly is being reviewed in resin.
How do I compare quotes for the same part in two processes?
Normalize the scope before comparing the numbers. Ask both quotes to state the quantity, the finish per surface, whether inspection results are included, and whether the price assumes the part is nested with other work. A resin quote for a single part and a nylon quote for a well-packed bed are not the same product. Once the scope matches, compare cost per usable part, not cost per print, and include the price of a reprint when a specification is incomplete.
Do SLS parts need any support removal at the end?
No support structures are built, which removes one finishing step entirely. What replaces it is powder removal: loose powder is cleared from internal channels and small features, and any partially fused material around thin sections is brushed out. For parts with enclosed volumes, powder escape paths need to be designed in, because a sealed cavity will hold material that cannot be extracted afterwards.
If the choice between resin detail and nylon durability is still open for a specific part, send the model with the property that decides it. 6CProto runs SLA, SLS, and MJF in the same facility, so both routes can be quoted from one file and one manufacturing review. Upload the geometry at the 6CProto quote page or send the drawing to projects@6cproto.com.