

Choosing a 3D printing process is choosing a set of trade-offs: speed against finish, strength against cost, material variety against simplicity. FDM, SLA and SLS, and SLS are the three most common processes for functional and visual parts, and each shines in a different situation. This article compares them on the properties that actually decide fit: material, strength, surface finish, accuracy, and cost, and gives a practical way to select the right one for your part.
How the Three Processes Differ
FDM (fused deposition modeling) extrudes thermoplastic filament in layers, so the material is strong but the surface shows layer lines and properties vary with orientation. SLA (stereolithography) cures liquid resin with a laser or projector, giving high detail and smooth surface but a resin that is often more brittle. SLS (selective laser sintering) fuses polymer powder with a laser, producing strong parts without support structures and with better isotropic-ish behavior, at higher machine cost.
Material and Coupled Properties
FDM uses engineering thermoplastics like ABS, PETG, nylon, and composites, offering toughness and temperature resistance with visible layers and anisotropic strength. SLA resins can be rigid, tough, or flexible but are generally less durable and light-sensitive. SLS typically uses nylon powders, producing tough, functional parts with no supports for complex geometry, though surface is rougher than SLA.
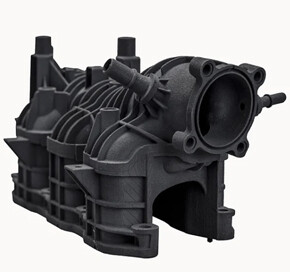
Check mechanical data on the printed condition, because layer adhesion and orientation change results in all three, and any process differs from an injection-molded benchmark.
Finish and Detail
SLA leads on detail and smooth surface, making it a fit for visual prototypes, patterns, and fine features. FDM parts show layer lines unless post-processed, and have a lower detail limit. SLS parts sit in the middle: strong and clean geometry with a slightly grainy surface. If the part is visual, SLA’s surface wins; if it is functional and handled, SLS or FDM may serve better.
Build, Supports, and Geometry
FDM needs supports on overhangs; SLA needs supports that may leave marks; SLS does not need supports. SLS is very good at complex, freeform, and internal-geometry parts, and nests multiple parts. FDM is cheap and scalable for short runs; SLA gives detail to smaller parts. Consider geometry complexity and post-process cleanup.
The Economics
FDM is the lowest entry-cost and common for quick, large, or functional parts. SLA has low part cost with resin and detail. SLS has higher machine and material barriers, but can be economical for small, complex batches that the others could not make in one piece. The honest answer is that the process that prices lowest is the one whose properties match the part.
A Selection Table
| Situation | Best fit | Reason |
|---|---|---|
| Visual and detail parts | SLA | Smooth, fine detail, good for presentation |
| Functional thermoplastic parts | FDM or SLS | Real material behavior |
| Complex geometry with internal cavities | SLS | Powder-based, limited supports needed |
| Budget model, quick iteration | FDM | Lowest entry cost and speed |
The Bottom Line
Choose between FDM, SLA, and SLS by asking what the part proves and what its material must do. If detail and surface matter, pick SLA. If functional toughness matters, use FDM or SLS, and choose SLS for complex no-support geometry. Match the process to the part, and the printed prototype or part earns its place in the product.
Note: process availability, materials, and properties vary by supplier; confirm datasheets, orientation, and post-processing before design decisions.