

A fabricated assembly is bought for one reason: the risk of the joint is easier to transfer than to manage. When a frame has to be welded square, a panel has to align after coating, or a set of brackets has to match a mounting pattern, buying the finished item replaces a build problem with a specification problem.
What counts as a custom fabricated assembly
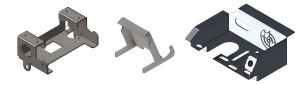
The term covers any part built from formed and machined components and delivered as one item: welded frames, enclosures with doors and hinges, panels carrying pressed inserts, and structural brackets joined to a base plate. The defining feature is that the finished item is measured as a unit, because the joining step introduces geometry that no single component drawing describes.
| Assembly type | Dominant process | What usually drives the tolerance |
|---|---|---|
| Welded frame or chassis | Cutting, forming, welding | Fixture position and weld sequence |
| Enclosure with moving parts | Forming, hardware, fastening | Hinge alignment and clearance across the joint |
| Panel with pressed inserts | Cutting, forming, insertion | Insert position and edge distance |
| Machined base with formed brackets | Milling, forming, fastening | The machined datum the brackets reference |
How joining changes what tolerance means
Before joining, each component has its own tolerance. After joining, the item has a different one, because the process either adds distortion or adds clearance. Welding adds heat and therefore movement, which is why a fixture and a defined sequence do more for the result than tightening the panel tolerances. Fastening adds clearance, which accumulates across a joint rather than staying local to one hole.
The practical consequence is that the assembly drawing should control the dimension that matters after joining, referenced to a datum that survives the process. A machined face or a fixtured hole makes a reliable reference; a formed edge that has been heated is not. Getting that choice right at the drawing stage removes most of the rework that otherwise happens at first article.
Can a fabricated assembly be produced without a welding fixture?
Sometimes, but not where alignment matters.
A single-part frame with generous tolerances can be tacked and welded on a flat table. Once an assembly has to match a mounting pattern, carry a hinged door or accept a mating component, the position of features relative to each other has to be held during welding, and that is a fixture job. The fixture is charged once and then protects every subsequent unit.
Where the quantity is very small, the alternative is a machined datum: build the assembly slightly oversize on the critical faces, then machine them after welding so the final geometry is produced by a cutting operation rather than by the welding. It costs an extra process and removes a whole class of variation.
Finish and hardware sequencing
Coating a finished assembly is cheaper than coating components separately, because handling happens once, but it constrains everything after it: welding after coating damages the finish, and pressing inserts after coating risks marking a visible face. The sequence therefore has to be planned as part of the design rather than added to the order.
Two rules prevent most problems. Keep weld areas free of coating, because coating inside a joint contaminates it, and mask or postpone any hardware whose fit would be changed by the coating thickness. Where the assembly will be visible, it is also worth naming the faces that must not be handled, since an assembly is carried more often than a flat panel. Coating and surface condition classifications follow ASTM Committee B08, drawing conventions follow ASME, and material data for the grades involved is published by ASM International.
How to inspect a fabricated assembly before shipment
Inspection on an assembly is a different exercise from inspecting parts. The useful record covers the interfaces: the mounting pattern, the faces that mate with other components, the alignment of any moving part through its range, and the overall envelope. Dimensions that were already verified on the individual components do not need repeating unless the joining process could have changed them.
Two practical points help. Measuring an assembly in the same orientation as it will be installed avoids apparent errors that come from how the item is supported, and recording the fixture used allows a later batch to be compared with the first. Process measurement guidance is published by the NIST Manufacturing Extension Partnership, and the environmental obligations that apply to coating and cleaning lines by the US EPA.
What to include on an assembly drawing
An assembly drawing earns its keep by describing relationships rather than components. The mounting pattern that has to match the receiving structure, the faces that mate with other parts, the position of any rotating or sliding element through its range, and the features that must remain adjustable after joining are all relationships. Component dimensions can live on component drawings; the assembly drawing should carry the interfaces.
It is also worth stating what the assembly is for. A frame that carries static load has different priorities from one that has to stay square while a door swings on it, and the two are inspected differently. Where the assembly will be finished, add the coating specification and the faces that must remain free of coating. Forming detail for the components is covered under forming and bending, and the drawing conventions used for these callouts follow ASME standards.
Send the assembly drawing with the interfaces that have to match, and request a quote for the completed fabricated assembly.
FAQ
Can a custom fabricated assembly be quoted from a single drawing?
It can be quoted from one assembly drawing plus component drawings, provided the interfaces are dimensioned on the assembly. Without those interface callouts the supplier has to assume which features must align after joining, and that assumption is where rework begins.
Is it cheaper to buy components separately and assemble in house?
It is usually cheaper when the joint is a simple fastener your team would install anyway. It stops being cheaper once alignment needs a fixture, welding introduces distortion, or the interfaces have to be verified after joining.
Should hardware be fitted before or after coating an assembly?
It depends on whether the coating thickness affects the fit. Inserts that must seat precisely are better fitted after coating, or masked, while hardware protected inside a closed section can be fitted beforehand to reduce handling.