

CNC machining cost is the answer to a long list of questions: the machine, the material, the geometry, the setup, the tolerance, the finish, the inspection, and the quantity. Buyers see a price and wonder why it is what it is; the price is the sum of decisions that each could have gone another way. The useful frame is not “is it cheap” but “what is this quote actually paying for, and which decisions can lower it without hurting the part.” This article breaks down what drives CNC machining cost and the levers that reduce it honestly.
The Machine Time Is the Core
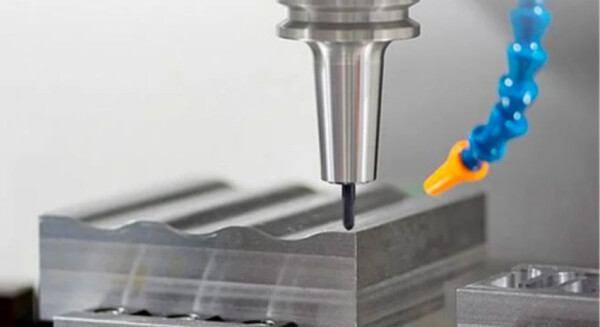
Machine time is the largest and best-understood cost. The part occupies a machine for the cycle time: roughing, finishing, and the setup around it. A part that cuts in twenty minutes costs less than one that cuts in an hour, and the cycle time is set by the geometry, the material, and the strategy. Multi-axis work, hard materials, and deep or complex features extend the cycle. The machine hour carries the shop overhead, so cutting the cycle is the most direct cost lever, and it is decided by design and programming.
Setup and Programming Are the Hidden Fixed Costs
Before the first part cuts, the job needs setup and programming. Fixtures are configured, tools are set, the program is written and simulated, and the first article is verified. These costs are fixed per order, so they matter most at low quantity: a two-part order carries the programming and setup over two parts, while a thousand-part order spreads them. The honest way to think about setup is per order, and the way to lower its impact is quantity, or reusing a proven program for repeat orders.
Material Cost and Stock Choice
The material is bought by weight or by size, and the cost is the raw material plus the waste. Machining is subtractive, so a part that is a small fraction of the blank pays for the whole blank and the chips. The levers are stock choice, orienting and nesting the part to minimize waste, and in some cases sourcing near-net stock. The material grade matters too: exotic alloys cost more per kilo and are harder to cut, and both costs show in the quote. The material decision is a cost decision from the start.
Tolerance and Finish Drive the Inspection and the Cycle
A tight tolerance costs twice: the machining has to hold it, and the inspection has to prove it. A loose general tolerance machines faster and inspects cheaper; a tight GD&T on critical features machines slower and needs CMM or gauge verification. The finish is the same story: a rough as-machined surface is cheap, a finish with a roughness spec adds the finishing pass and the measurement. The lever is specifying tolerance and finish where they matter, not everywhere, because every unnecessary tight callout buys a cost and sells nothing.
Quantity Changes the Per-Part Math
Quantity is the largest multiplier in the cost story. Because setup and programming are fixed, the per-part cost drops as the quantity rises; a run of fifty is far cheaper per part than a run of five. The honest planning question is the real quantity over the program, not a one-off number, because a design change that allows a bigger run at equal quality is one of the strongest cost cuts. For repeat orders, the program can be reused, cutting the fixed cost further.
The Cost Reduction Levers
- Design for machine time: simpler cycles, standard features, fewer setups.
- Quantity: spread the fixed setup and programming over a real run.
- Material: right-sized stock and grade, nesting to reduce waste.
- Tolerance and finish: call them out where they matter.
- Repeat the program and reuse the fixture and the tool data.
- Get a DFM review that names the cost drivers before quoting.
What to Ask for in the Quote
Ask the supplier to break the cost: machine time, setup and programming, material, finishing, and inspection. The breakdown shows which decisions drive the price and which levers are available. A quote that names the machine hours and the setup is one you can act on; a single line item is a number you negotiate blind. The DFM review should name the cost drivers and the opportunities, because the engineer who reads your geometry can see the cheap design and the expensive one.
Bottom Line
CNC machining cost is machine time plus setup, material, finishing, and inspection, scaled by quantity, and each component is a decision. Lower the cost honestly by designing for machine time, spreading setup over quantity, right-sizing the material, and specifying tolerance and finish where they matter. Ask for the breakdown and a DFM review that names the drivers, because the price is a map of decisions. The cheap part is not the one with the discount; it is the one whose decisions were made for efficiency without selling the function.
Related Capabilities and Turning the Advice Into an Order
The discipline in this article holds best inside a wider capability set, where the drawing, the datum, and the inspection travel with the part across the program. The CNC machining materials pages cover the service scope and the tolerances that apply, and the first article ties the design to the measured result. The concrete next step is to send a drawing with the critical features and the datum stated, ask for the DFM review, and request the first-article report with values, so the advice becomes a controlled order instead of a good idea.
The Reorder That Carries the Savings
The cost story closes with the reorder. A part whose program, fixture, and tool data are saved re-quotes and re-machines faster and cheaper than a first order, and the savings compound with the repeat. The buyer should ask the supplier to keep the program, the fixture, and the inspection data on file, so the second order starts from the proven setup. The reorder is where the upfront cost of a good program is paid back. A supplier that stores the program and re-runs it is a supplier whose cost curve you benefit from.
The Parameters That Move the Price
The price moves with a short list of parameters: the part size and geometry, the material, the tolerance, the finish, the quantity, and the secondary operations. Each is a lever, and the buyer who understands the list can move the price by moving the part. A larger radius, a looser tolerance on a non-critical feature, a simpler finish, and a real quantity all lower the cost. The DFM review names the parameters and the opportunities, and the quote reflects them. The cheap part comes from the right parameter choices, not the best discount.
The Value of Asking for the Breakdown
The quote breakdown is the buyer's map of the cost, and asking for it is free. The machine time, the setup, the material, the finish, the inspection, and the per-part price at the real quantity show where the money goes and where the levers are. A supplier that gives the breakdown invites the comparison; one that hides it invites the surprise. The buyer who reads the breakdown knows which parameter to move, and the DFM review confirms it. The breakdown turns a price into a decision.
Asking for the DFM Before the Price
The DFM review before the price is the best cost tool a buyer has. The review reads the part and names the opportunities: the radii, the tolerances, the finish, the stock, and the strategy. It turns a price into a story and a plan. A buyer who asks for the DFM before the quote gets a supplier who thinks about the part; one who asks only for the price gets a number. The DFM is the difference between buying a part and engineering a cost. Ask for it, and the expensive part explains itself before it is ordered.
The Lifecycle View of the Machined Part
The cost of a machined part is not only the unit price; it is the lifecycle: the prototype, the first article, the run, the reorder, the field performance. A part that costs a little more and assembles, serves, and reorders well is cheaper than one that saved on the unit and costs in the field. The lifecycle view is what the DFM and the breakdown serve: they let the buyer see the whole cost, not the invoice. The machined part is priced on the unit and valued on the lifecycle, and the buyer who compares both makes the better decision.
The DFM as the Buyer's Voice in the Cost
The DFM is where the buyer's voice enters the cost: the review reads the part and asks whether the geometry, the tolerance, and the finish are doing useful work. The radii, the pockets, and the callouts are the buyer's design decisions, and each carries a cost. A DFM that names the opportunities lets the buyer choose where the money goes; one that accepts the drawing silently hands the cost to the quote. The buyer who uses the DFM is engineering the cost, not just receiving it. Ask for it, and the price becomes a decision.
Related Capabilities and Guides
For the service scope and the material and tolerance details behind this article, see the CNC machining, the DFM checklist, and the materials. The first article of your order ties the design to the measured result, and the same drawing, datum, and inspection discipline carry across the program.