

Explore Sheet Metal Design, Materials & Assemblies
How Galvanized Steel Parts Work
Galvanized steel parts are steel components protected by a zinc layer, usually applied by hot-dip galvanizing or electrogalvanizing. The zinc acts as a sacrificial barrier: it corrodes preferentially before the base steel, which slows red rust formation and extends the usable life of the part in many environments. The coating also shields small scratches and edge damage, although severe abrasion or aggressive chemicals can still compromise performance.
Hot-Dip, Electrogalvanizing, and Pre-Galvanized Stock
The right method depends on geometry, corrosion exposure, surface finish needs, and the fabrication sequence. Hot-dip galvanizing creates a thicker, tougher coating that is favored for outdoor infrastructure, supports, and exposed frames; its trade-offs are a rougher finish, dimensional growth, and coating buildup on holes and edges. Electrogalvanizing produces a thinner, smoother finish that suits cosmetic parts and visible components, but it carries less corrosion reserve in demanding exposure. Pre-galvanized sheet stock is consistent input for high-volume stamping and forming, yet cut edges and weld zones need extra attention because the protective layer is interrupted there.
For fabricated parts, the practical question is usually whether to build from pre-galvanized material or galvanize after forming. Galvanizing after forming protects the cut edges and weld zones that pre-coated stock leaves exposed, but the coating can build up on internal corners and change the fit of holes and threads. The sheet metal fabrication service covers both routes, and the sheet metal materials page lists the coated stock options.
Designing for the Coating, Not Just the Geometry
Designing well for galvanized parts starts with the coating process. Allow the coating thickness into critical fits, enlarge holes where zinc buildup could interfere, avoid sharp internal corners that trap coating or stress, and plan vent and drain features for closed sections so trapped zinc cannot pool inside. Bend radii need confirmation against the coating because thick zinc can crack or spall at a tight radius, and the weld strategy should be reviewed before the coating is selected because heat disrupts the zinc near the joint.
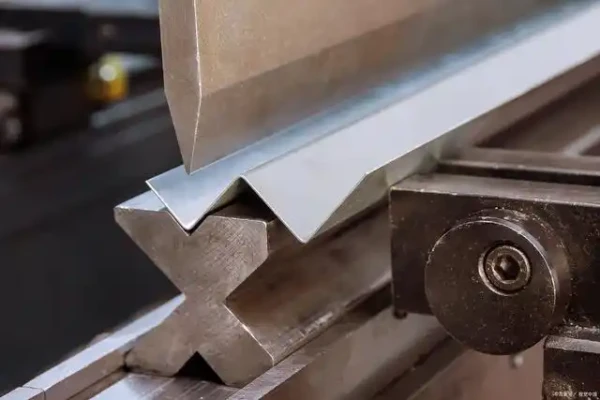
This is where design reviews earn their keep. A common scenario is prototyping an outdoor bracket in plain steel, then moving to galvanized material after field corrosion appears; the redesign usually needs extra clearance at mounting points and a tolerance review. Small geometry changes at this stage prevent expensive rework after coating, and the DFM checklist is a useful starting point for the review even when the part is formed rather than machined.
Cut Edges, Welding, and Post-Coating Work
Cut edges and weld zones are the weak points of galvanized parts. Shearing or laser cutting removes the zinc at the edge, and the protection there depends on the zinc runoff from the adjacent surface or a touch-up coating applied after cutting. Welding is worse: the heat burns the zinc off around the joint and produces zinc oxide fume, so the area needs cleaning, ventilation planning, and post-weld corrosion protection before it is painted or powder coated.
Post-coating machining deserves the same caution. Threading a coated hole changes the thread fit, and grinding or buffing a coated surface removes the protection locally. If the part must be machined after coating, define the masked and machined zones on the drawing and plan touch-up for the exposed steel.
Coating, Fit, and Tolerance Stack-Up
Galvanizing adds dimension, and the added thickness has to live inside the tolerance plan. A hot-dip coating on a formed part is not perfectly uniform: edges and internal corners carry more zinc, so a nominal thickness value is only a starting point for the fit calculation. For tight fits, sliding interfaces, and machined surfaces, plan the coating into the tolerance stack-up from the first drawing, and confirm the inspection method for coating thickness with the supplier. The standards and tolerances page shows how formed and coated parts are toleranced.
The alternatives to galvanized steel are chosen on the same basis. Stainless steel gives stronger corrosion resistance in harsher environments but at higher cost; aluminum saves weight where mass matters; plain carbon steel is cheapest where corrosion exposure is limited. Galvanized steel wins when the goal is dependable performance at controlled cost and the design can tolerate the coating thickness. Industry reference values for coating and testing are available from ASTM standards.
Quality Risks and What to Inspect
The common risks are coating variation, poor adhesion, edge corrosion, dimensional change, and damage during handling or fabrication. Ask suppliers how they inspect coating thickness, surface condition, and dimensional impact, and how they prevent handling damage during shipping. The inspection methods used for fabricated parts, including CMM checks where applicable, are described in the CMM inspection article.
When to Specify Galvanized Steel
Specify galvanized steel when corrosion resistance is needed but the part does not justify a corrosion-proof alloy: outdoor exposure, moisture, condensation, road splash, storage, and utility applications, and anywhere maintenance access is limited and replacement is costly. It is a weaker fit when the part has very tight sliding fits, cosmetic perfection is critical on every surface, the part will be heavily machined after coating, the environment includes harsh chemicals or constant abrasion, or the assembly involves heat-sensitive welds or adhesives. For rapid iterations, consider galvanized steel after the first functional version, when the environment and fit requirements are known; the rapid prototyping service is the usual route for the earlier stages.
Edge, Cut, and Weld Behavior You Need to Plan Around
Galvanized steel is specified for its corrosion performance, but every manufacturing step modifies that performance, and the drawing should reflect the consequences. Cutting the sheet exposes bare steel at the edge, and although the zinc coating provides some cathodic protection to adjacent bare metal, cut edges remain the first place corrosion starts on a galvanized part. Edge treatment, paint systems, or the choice of a heavier coating class can close the gap, and the edge condition should be part of the finishing plan rather than an assumption.
Welding is the second stress point. The zinc boils before the steel melts, producing fumes and weld porosity if the process is not managed, so welding on galvanized material requires preparation: removing the coating at the weld zone, adjusting the process, or accepting and controlling the porosity with the correct filler and ventilation. The same applies to laser cutting and forming: the coating at a bend radius can crack if the radius is too tight for the coating class, and the crack becomes a corrosion path even though the part looks sound.
These behaviors do not make galvanized steel difficult; they make it process-aware. Specify the coating class and the bend radii, state which edges or weld zones will be treated, and let the fabricator quote the preparation and finishing steps. For parts that combine galvanized sheet with formed features and fasteners, the sheet metal fabrication service plans the cutting, forming, and edge treatment sequence together.
Coating Class, Environment, and Service Life
The environment determines the coating class more than the name “galvanized” does. A part that lives indoors in a dry assembly benefits from a standard coating, while a part exposed to road salt, marine air, or repeated condensation needs a heavier coating class or a supplementary paint system. The data sheet for the coating class states the coating mass per unit area, and that number, not the trade name, is what the specification should cite so the supplier buys the right material and the quality check has a value to measure.
Service life expectations follow from the exposure and the coating thickness. Zinc protects steel by corroding preferentially, so the protection lasts as long as the zinc remains, and the corrosion rate depends on the environment. A heavier coating extends the service life in a given environment; a smaller part feature, a threaded hole, or a tight bend can reduce the effective protection locally because the coating is thinner or cracked there. Matching the coating class to the environment and the harshest local feature is the practical design step.
Cosmetic expectations are a separate axis. Galvanized surfaces show spangle, variable finish, and marking after forming, so parts that need a consistent appearance usually get a supplementary paint or powder coat. When appearance matters, specify the final finish and the prep between galvanizing and painting, because adhesion depends on the surface treatment ahead of the paint. The surface finishing service page shows the coating and preparation options available for formed metal parts.
FAQs
Are galvanized steel parts better than painted steel?
Often yes where coating damage or maintenance is a concern. Paint performs well, but galvanized steel adds sacrificial corrosion protection, so a scratch that exposes the steel keeps a layer of zinc working instead of failing outright at the damage site.
Can galvanized steel parts be welded?
Yes, but welding damages the zinc coating near the joint and releases zinc oxide fume. Those areas need cleaning, ventilation planning, and post-weld corrosion protection.
Do galvanized steel parts rust?
They can, eventually, especially if the coating is damaged, worn, or exposed to aggressive conditions. The zinc layer significantly delays corrosion, but it does not make steel immune forever.
Is galvanized steel suitable for precision parts?
It can be, but the coating thickness must be included in the tolerance plan. Tight fits, sliding interfaces, and surfaces machined after coating need special attention.