

Explore Sheet Metal Design, Materials & Assemblies
Geometry Limits Come from the Process
Sheet-metal geometry limits come from the process. The material must be thick enough to form and stiff enough to serve, thin enough to bend, and the features such as holes, slots, and flanges must respect the distances the process needs. Designing within the limits is what separates a part that forms cleanly from one that cracks, distorts, or costs twice. Every process has its envelope: laser cutting handles a thickness range, bending needs a radius the tooling can produce, and forming needs features that do not tear the material.
The practical approach is to design within the envelope and let the fabrication review catch the violations. The limits are not arbitrary, they trace to a machine or a tool: the press brake needs a certain material length to grip the flange, the punch needs clearance from the edge, and the laser needs a minimum feature size to cut cleanly. That is why the same numbers keep appearing in design guides, and why the material column of any limits table is not decoration. A design rule that works for one material does not automatically transfer to another: high-strength steel bends at a larger minimum radius than mild steel of the same gauge, and a thicker sheet needs more flange height to hold in the die.
Thickness Ranges by Material
Sheet-metal thickness ranges by material and process. As a reference, 6CProto’s stated sheet-metal capabilities include laser cutting for steel up to 20 mm, aluminum up to 12 mm, and stainless up to 10 mm, with punching for mild steel up to about 3 mm and bending for thickness up to 6 mm. The material drives the limit, and the process envelope follows.
Common sheet-metal thicknesses cluster around standard gauges because the mills and the shops are set up for them. Aluminum sheet is typically specified between about 0.8 mm and 6 mm for custom fabrication, with 1.0 to 3.0 mm the busy range for enclosures and brackets; steel and stainless cover a similar band with different strength and weight consequences. The selection logic: thinner material forms and bends more easily but needs ribs for stiffness; thicker material carries load but limits bending and adds cost.
Minimum Bend Radius by Material
Comparing the common grades makes the material column concrete. Aluminum 5052 forms with excellent bendability and corrosion resistance, which makes it the default for enclosures and panels that need tight radii; aluminum 6061 offers higher strength but bends less willingly, so it appears where stiffness dominates and the radius can be generous. Mild steel balances cost, strength, and formability and is the workhorse for frames and structural sheet; high-strength steel needs the largest radius of the family and a process that accounts for springback. Stainless 304 forms reasonably with the right radius while 316 work-hardens faster and pushes the radius up further. In practice, the phrase “thickness and bend radius” on a drawing means little without the grade, because the grade sets both the formability and the springback compensation the shop must apply.
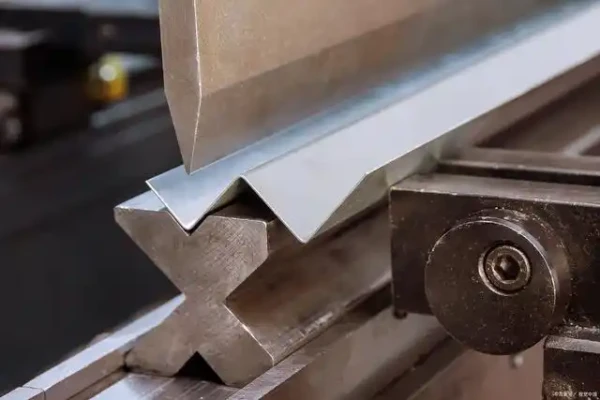
The gauge sets the minimum bend radius and the springback behavior, so thickness is a design input rather than an independent choice. Softer alloys bend tighter than harder ones: 5052 aluminum accepts a tighter radius than 6061, and mild steel bends tighter than high-strength steel of the same gauge. Stainless work-hardens during the bend, which is why it needs a larger radius than carbon steel for a given thickness. The rule is to use a generous radius where the design allows and to specify it with the material, because an undersized radius either cracks the outside fiber during forming or forces a costly process change to a thinner gauge.
Thickness and stiffness interact in a predictable way that belongs in the selection. Bending stiffness scales steeply with thickness, roughly with the cube, while weight scales linearly, so a small gauge increase buys a large stiffness gain but also moves every forming limit. That is why a part that only needs stiffness can often stay thin with ribs or formed flanges added, while a part that carries real load must accept the larger radius that the thicker gauge demands. Run the feature distances and bend radii against the chosen gauge before quoting, because the interaction, not the thickness alone, is what the fabricator forms.
Springback sets the second limit. Every bend springs back by a material- and radius-dependent amount after the tool releases, and the shop compensates with over-bend. A spec that ignores springback produces flanges that sit at the wrong angle, which is why the bend radius and the material temper belong together on the drawing.
Feature Distances: Holes, Slots, and Flanges
The features must respect the distances the process needs. Holes should stay clear of edges by a multiple of the thickness, because a hole near the edge distorts the material or tears through during punching or forming. Holes should stay clear of bend zones entirely: a hole inside a bend radius creates a stress concentration that cracks under forming, and the design rule is to move the hole out of the bend or add it after forming. Minimum flange heights follow the tool that forms them: a flange too short for the die will not grip or will not form consistently, and a rib too shallow produces the same failure.
Laser-cut features add their own limits. The laser needs a minimum feature size to cut cleanly, and internal corners impose a kerf-dependent radius rather than a sharp square corner. Punching adds the edge distance and the slug-size limits, and the laser cutting and punching service pages explain the process envelopes.
Design Within the Envelope
Designing within the envelope starts with the drawing. Show the material grade, thickness, bend radius, and the feature distances on the drawing, and treat the limits table as the checklist that is run before quoting. Where a tight radius and a stiff gauge conflict, the drawing should show both requirements and let the fabrication review resolve the conflict, because a part that needs a tight radius may have to use a thinner gauge, and a part that needs stiffness may have to accept a larger radius.
Non-standard thicknesses are available but carry cost and lead time. A half-gauge material may have to be ordered specially while the standard gauge is on the shelf, so check the supply position before locking a drawing to a thickness the supplier cannot source quickly.
Confirm the Limits with the Supplier
The fabrication review is where the design meets the real envelope, and it should be scheduled before the quote rather than after it. A complete request includes the material grade and temper, the thickness, the bend radius with the direction relative to the grain, the hole positions relative to edges and bends, and the flange heights the tooling must grip. The review catches the violations that the tables cannot encode, such as a bend line running through a stiffened feature or a hole pattern that leaves too little material between openings.
Suppliers quote different limits because their tooling differs. The die sets, punch radii, and machine beds available in a given shop set the real envelope, so treat the published table as a starting point and confirm the shop’s capability at quoting. The sheet metal fabrication service covers cutting, punching, bending, and forming across the material range, and the sheet metal materials page lists the grades and thicknesses available. When you request a quote, include the material, thickness, and bend requirements, and the engineering team can confirm the design against the process envelope.
Conclusion
The tolerance callouts complete the part. Sheet metal holds looser tolerances than machined parts because forming, springback, and the sheet itself introduce variation, so the drawing should apply realistic tolerances to formed features and tight ones only where the assembly needs them. Specifying a machining-grade tolerance on a bent flange sets the shop up to fail or to add cost for no functional gain.
Sheet-metal geometry is process-limited. Thickness, bend radius, and feature distances follow the material and the process, and designing within the envelope produces parts that form cleanly. The fabrication review is the check against reality, and the sheet metal tolerances guide carries the same discipline into the dimensional callouts. The NIST engineering references cover the material property data behind the formability limits.
FAQs
What is the minimum bend radius for sheet metal?
It depends on the material, softer alloys bend tighter than harder ones, and the tooling. Use a generous radius where the design allows, and specify it with the material grade.
How close can a hole be to an edge or bend?
Holes should stay clear of edges by a multiple of the thickness and clear of bend zones entirely. The exact distances depend on the material and the process.
What thickness can sheet metal fabrication handle?
It depends on the process and material. As a reference, 6CProto states laser cutting for steel up to 20 mm, aluminum up to 12 mm, and stainless up to 10 mm, with bending up to about 6 mm.