

Explore Sheet Metal Design, Materials & Assemblies
Battery Enclosures Are Safety Components
A battery enclosure is not a box; it is a safety system. It must contain the cells in normal operation and in a crash, keep water and dust out, manage heat, and survive the operating environment for the life of the vehicle. In practice this means the enclosure is designed from safety and environmental requirements rather than from a convenient sheet size: every weld, fastener, and seal location is a decision with safety consequences.
The mechanical loads come from several directions at once. Vehicle vibration, mounting points, thermal cycling, and crush or impact cases all transfer into the sheet-metal structure, and the panel thickness and formed ribs have to serve all of them. Structural analysis of these load paths should be part of the design package suppliers receive so the gauge and reinforcement layout can be confirmed against the loads rather than guessed.
The enclosure also crosses the electrical boundary. Bus-bar pass-throughs, vent valves, and connector plates pass through the sheet-metal shell, and each crossing needs its own sealing and clearance design. The drawing should treat every penetration as a designed feature rather than a hole added late in the layout.
Sealing and IP Requirements
Sealing keeps the environment out, and the enclosure IP rating defines what that means. The rating is earned at the sealing interface, not by the sheet metal alone: a welded seam must be continuous and leak-tight, a gasketed interface needs a flat, consistent flange surface with controlled fastener spacing, and the gasket groove, fastener torque pattern, and flange flatness must work together. A flatness problem at the flange shows up as a failed ingress test even when the gasket is correct, so the drawing should control the flange zone explicitly.
The vent is the deliberate exception to the seal. Battery packs need pressure equalization and emergency venting, and a sealed box without a designed vent will fail somewhere unintended. The vent opening, its mounting, and its protection from debris should be part of the enclosure design from the first revision.
Sealing validation belongs on the test plan. A water-ingress check at the prototype stage, repeated on the pre-production unit, catches joint problems that visual inspection misses. State which test, at which stage, produces the approval gate for the batch.
Thermal Paths: Fins, Channels, and Interfaces
The enclosure participates in the pack thermal design in three places: the cold plate interface, the side-wall conduction paths, and the air paths for cooled packs. Each path has its own surface requirement, and the sheet-metal process has to deliver them together on one part.
For air-cooled packs, the enclosure forms the flow path rather than merely enclosing it. Louvers, standoffs, and baffles direct air across the cells, and the panel geometry becomes part of the thermal model; the fabricator should see the airflow direction on the drawing so the features are formed the right way around. The forming and bending service page explains how these features are produced, and the sheet metal materials page covers the base alloys and gauges available for enclosure work.
The cold plate interface is the tightest of the three. Flatness, fastener load, and the thermal interface material determine the contact resistance, and the enclosure flange that holds the plate needs controlled flatness and a defined finish. Confirm the machining or forming approach for that zone before quoting.
Material and Coating Choices
Aluminum keeps pack weight down and conducts heat well, which is why most enclosures start there; steel appears when strength or cost dominates. The structural requirement should decide the material family, and the gauge should be confirmed against the load cases rather than chosen from habit. The coating, whether powder, anodizing, or galvanizing, protects the corrosion path and supports electrical isolation at the same time: powder coating covers large surfaces with durable insulation, while bare or masked zones preserve the electrical grounding paths, so the drawing should mark which surfaces are coated and which stay bare for contact.
Coating thickness at edges and threads is a common failure point. A coated bolt hole changes the thread fit, and a coated edge can chip where the sheet is thin; masking, edge break, and post-coating tapping are details to confirm with the supplier before the finish is specified. The standards and tolerances page explains how coating and forming allowances fit into the overall tolerance plan.
Welding, Fasteners, and Assembly
The enclosure is assembled from sheets by welding, fasteners, or both. Continuous welds seal and stiffen but add heat and distortion; fasteners with gaskets allow service access but add parts and sealing points. Each joint should be deliberately assigned to one strategy.
Welded enclosures need a plan for distortion control. The weld sequence, clamping, and panel gauge determine how much the box pulls out of square, and a large welded lid will bow without fixturing; the fabrication plan is part of the quotation and should be reviewed with the design.
Fastened enclosures live or die on the fastener pattern. Spacing that is too wide lets the gasket relax between bolts, and inconsistent torque makes the seal uneven; the drawing should define the pattern, torque, and gasket compression the assembly needs.
Testing and Documentation Expectations
Battery enclosures carry testing and documentation expectations: sealing tests, structural checks, and material and process records. The scope depends on the application and the customer requirements, so define which tests, which records, and what traceability in the RFQ and confirm them with the supplier before production.
The test scope is defined before production: ingress, leak, thermal, and mechanical checks each need a method, a pass criterion, and a stage. The documentation set follows it: material certificates, weld records, dimensional reports, and test results are the enclosure evidence, and the format should be agreed at quoting, because a test that was never written down cannot be used in a review later.
Traceability matters most for safety parts. The batch number, cell lot, and enclosure serial should be linked so a field issue can be traced to the manufacturing conditions; confirm how the supplier labels and records each unit before the production order is placed. The CMM inspection article describes the inspection framework used for custom manufactured parts and the reports to expect.
What to Specify at Quoting
When requesting a fabrication quote, state three things: the IP rating and the sealing test you expect, the thermal requirement and which interface dominates, and the structural or crash load case the enclosure must survive. Together they tell the fabricator which seams weld, which flanges need controlled flatness, and which panels carry the load. Steel thickness and aluminum grade choices can then be confirmed against the actual load cases, and the coating and masking plan follows the environment and the electrical grounding path.
Compare sealing, thermal, and structural requirements against the sheet metal tolerances guide before the drawing is frozen, and confirm the machining or forming approach for the contact zones at quotation. Program-level test methods can be referenced against ASTM standards where an internal specification is not yet defined.
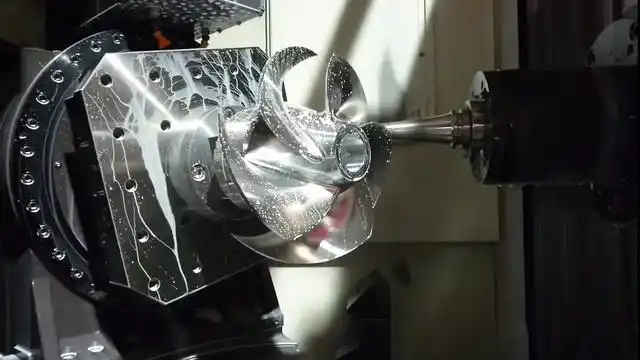
For enclosure parts that combine sheets with machined interfaces, the CNC machining service covers the precision details on the same part.
Crash and Crush Load Paths
A battery enclosure that only passes static checks is not ready for the vehicle. In a crash, the enclosure shares load with the vehicle structure, and how it deforms decides whether the pack stays contained, whether bus bars stay separated, and whether the thermal runaway vent operates as designed. The load case is usually prescribed by the program; the design task is to make the sheet-metal structure carry it predictably.
Folded sections and formed ribs are the practical tools. A hemmed edge, a deep flange, or a corrugation adds stiffness without adding gauge, and stiffening the panel at the mounting points protects the fasteners from tearing out under impact. The same geometry has to leave room for the cell stack and the service paths, so the crash structure is designed in the same iteration as the pack layout, not bolted on afterward.
Deformation behavior matters as much as peak strength. A panel that is too stiff can transfer crash load into the bus bars; one that is too soft can crush the cells before the vehicle structure takes the load. That is why the drawing should state which zones are allowed to deform and which must stay rigid, and why the prototype is tested in the vehicle load frame rather than as a free-standing box.
For suppliers, the practical consequence is that quoting starts with the load case, not the sheet size. When the RFQ names the crash or crush scenario and the required containment criteria, the fabricator can choose gauge, rib layout, and weld strategy against evidence instead of habit. The same logic applies to mounting brackets and shear plates that tie the pack to the vehicle: their gauges and hole patterns are load decisions, and the drawing should say which load case each feature serves.
FAQs
Why is a battery enclosure considered a safety component?
Because it contains the cells, seals the environment, carries crash loads, and manages heat. The sheet-metal design and fabrication follow from these safety requirements, and each joint, seal, and weld location is reviewed against them.
How is the enclosure sealed against water and dust?
Through joint design: welded seams provide continuity, gasketed interfaces control compression, and the flange flatness and fastener pattern hold the seal over the part life. Sealing is specified as an IP rating and verified by the corresponding ingress test.
Which material suits most battery enclosures?
Aluminum when pack weight and thermal behavior dominate, steel when strength and cost matter more. The coating follows the environmental exposure, and the choice should be confirmed against the structural requirement in the RFQ rather than selected from habit.