

Explore Anodizing, Conversion Films & Coatings
The gap between a prototype and a production part is often in the finish. The geometry is the same, but the anodized production cover looks different from the printed or machined prototype beside it, and a finish mismatch can sink a design review at the last minute. Matching prototype finishes to production is not about luck; it is about choosing the prototype route with the finish in mind, transferring the standard, and checking the match under the lighting and at the texture the product will actually have. This article explains how prototypes and production finishes diverge, how to make prototypes carry the production finish, and what to confirm so the review shows the product, not a stand-in.
Why Prototypes and Production Diverge
A production part is made by the production process: anodized aluminum, painted sheet, coated cast metal. A prototype is usually made quickly from whatever route is convenient, printed or machined, and its surface behaves differently from the production material. An anodized production surface has a specific color, gloss, and texture; a printed prototype has none of those. The divergence is not laziness, it is the prototype being built by the fast route. The fix is to plan the finish transfer when the prototype is ordered, not to discover the gap at review.
The Finish Standard: A Physical Master
The reliable bridge between prototype and production is a physical finish standard: the master sample that defines the accepted color, gloss, and texture under defined lighting. A photograph is not a standard, because monitors and white balance shift it. Define the color tolerance, the gloss, the texture, and the lighting used to judge them, and let the same physical master govern the prototype and the production batch. The master is what makes ‘match the sample’ a repeatable spec instead of an argument.
Anodizing on Prototypes
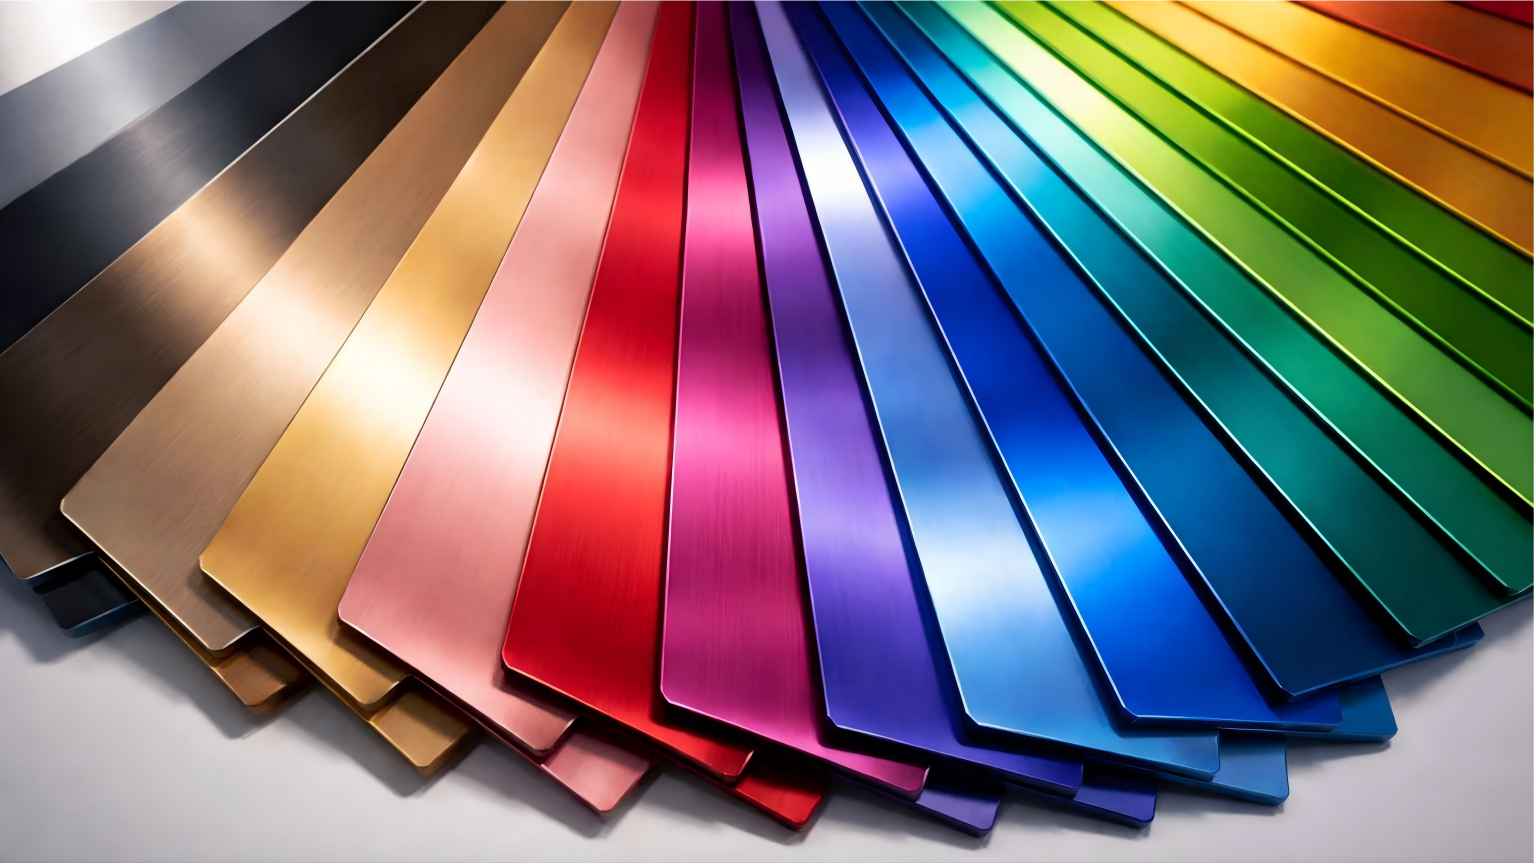
Anodizing is a production finish for aluminum, and prototyping in anodized aluminum is the honest way to match it. A piece anodized in the same alloy, the same pre-treatment, and the same dye reads close to production, because the finish is the same process. For prototyping, the dye is applied over a machined surface that may not be the production texture, so the color matches and the texture may not. Confirm the texture of the prototype surface against the production one, and use the master to judge.
Painting and Coating on Prototypes
For painted products, a prototype can carry the production paint color and gloss with the same paint system. The texture of the substrate changes the read, so the prototype surface should be prepared to resemble the production substrate. If the production part is powder coated, a painted prototype of the same color and gloss shows the color but not the powder texture. State what the prototype must match: color, gloss, texture, or all three, and prepare the prototype surface accordingly.
Texture Is Half the Finish
The same color over two textures reads as two colors. A matte, blasted, or machined surface scatters light differently from a smooth one, so a color matched on a smooth master can be rejected on a textured production part. Texture and color should be specified and judged together: a texture sample and a color master, or an approved part with both. The prototype that matches production textures as well as colors is the one that survives the review table.
Lighting: Judge Under the Real Conditions
Finish judgment depends on the light. A color matched under a cool office light can look wrong under warm gallery light or daylight. Judge the prototype and the production sample under the lighting the end user will use, and state it. This is the cheapest, least-swapped step in finish matching, and the one most commonly skipped, because it decides whether the match holds at the moment it matters.
How to Order a Match-Ready Prototype
- Set the finish standard: a physical master with color, gloss, and texture, and a lighting condition.
- Choose the prototype route that can carry the finish: anodized, painted, or coated.
- Prepare the prototype surface to resemble the production substrate texture.
- Judge the prototype against the master and the production sample under the same light.
- Confirm whether tolerances apply before or after the finish, for fit-critical surfaces.
When a Slightly Different Finish Is Acceptable
Not every prototype needs the production finish. A functional prototype testing mechanics does not need an anodized face; a form prototype for internal review may not justify a full finish line. The cost of the finish transfer should follow the risk of the mismatch. Match the finish when the design review, customer sign-off, or investor demo depends on the appearance; leave it when the prototype exists to test something else. The decision is what the prototype must prove.
Bottom Line
Prototype finishes that match production come from a physical standard, the right prototype route, and the same lighting. Set a master that defines color, gloss, and texture, prototype in the process that can carry the finish, match the texture as well as the color, and judge under the real light. Forget the texture and the light, and a perfect color match fails the table; include them, and the prototype reads as the product. That is what the review should show.
Why the Substrate Texture Decides the Match
The texture of the surface under a finish decides how that finish reads. A powder-coated part over a rough finish shows the texture; over a smooth face it reads smoother. The same paint color over a machined and an as-cast surface looks like two different products. For a prototype to match production, the substrate has to be prepared to the production texture: the prototype surface should be machined, blasted, or smoothed to resemble the production part, not just painted the production color. Decide which surface texture the product will have and reproduce it on the prototype, or the color match fails at the review table.
The Gloss and the Light: The Third Variable
Color and texture are two of the variables; gloss is the third, and it changes how both read. A gloss finish reflects light and shows color saturation; a matte finish scatters it and reads darker at some angles. The gloss is set by the coating and the cure, and it has to be specified and checked against the production sample. A prototype finished to the production color but the wrong gloss looks wrong under light, and a change of one gloss step can be the difference between an approved sample and a reject. Judge color, texture, and gloss together, under defined light.
The Master Sample: The Only Reliable Standard
A physical master sample is the only finish standard that a shop, a reviewer, and a customer all read the same way. The master carries the color, the gloss, the texture, and the lighting intent, and it is what the prototype and the production batch are compared against. Photographs and color numbers drift with screens, calibration, and viewing conditions, so a physical sample is the anchor. Keep the master safe, document which revision it represents, and use it for both the prototype approval and the production release, so the translation is one standard, twice applied.
When a Prototype Needs the Production Finish
The finish transfer is worth the cost when the appearance is on trial. A customer sign-off, a design review, a marketing shoot, or an investor demo is a case where the prototype must read as the product. For those, spend the money to finish the prototype in the production process: anodize the aluminum, paint or powder the panel, texture the surface. For a functional test where appearance is not on trial, the finish is optional. The rule is to match the finish to what the prototype must prove, not to standardize every prototype.
Finish First Articles and the Batch Release
The finish is validated the same way the geometry is: on a first article. Machine the prototype, finish it to the production standard, and review it against the master under the real light. Then the production batch is released against the approved finish sample, and the first article of the run repeats the check. The finish loop is small and cheap, and it is the step that turns a color chart conversation into a product that looks right on the shelf. A finish approved once is a finish that repeats.
The Prototype Finish Budget Follows the Risk
How much to spend finishing a prototype should follow the risk of the mismatch. A prototype that must pass a customer’s sign-off, a design review, or a marketing shoot justifies the full production finish; a prototype that tests a mechanism does not. The decision is about what the prototype must prove, and the budget follows it. Matching the finish where the appearance is on trial, and skipping it where it is not, spends the money where it changes the outcome and saves it where it does not.
Handling the Finish Mismatch Gracefully
When a prototype cannot carry the full production finish, be explicit about the gap rather than hiding it. State what the prototype shows and what it does not: the color is right but the texture is not; the geometry is right but the anodize is the prototype route. An honest note that the production finish is yet to be verified protects the review from assuming a match that was never claimed. The mismatch is a planning detail, not a secret, and naming it keeps the decision accurate.