

What an Electroplating Service Actually Does
An electroplating service is an electrochemical process that deposits a thin, cohesive metal layer onto a conductive substrate using a controlled direct current. The part being plated acts as the cathode, the plating metal as the anode, and the two are connected through an aqueous electrolyte bath carrying dissolved metal salts. When current flows, metal ions are reduced at the cathode and bond to the substrate at the atomic level. For non-conductive parts such as 3D-printed polymers or molded plastics, the surface is first made conductive with an electroless strike or palladium activation before standard electrodeposition can begin.
The layer thickness is the first specification that matters. Plating is commonly specified in micrometers or microinches, and the practical range for most functional work is roughly 0.0001 to 0.020 inches (2.5 to 500 micrometers); decorative coatings sit at the thin end, while hard chrome and nickel for wear or restoration sit at the thick end. The thickness requirement drives the process time, the racking, and the cost, so it should be stated on the drawing rather than left to the plater’s default.
Electroplating earns its place in a manufacturing program for four reasons: corrosion protection, wear and friction control, electrical and signal performance, and dimensional restoration. Each reason selects a different metal. Zinc and nickel protect against corrosion, hard chrome and electroless nickel resist wear, gold and silver deliver low contact resistance and solderability, and nickel or chrome can build a worn surface back to print. The mistake is treating “plating” as one finish; the metal, the undercoat, and the thickness are separate engineering decisions.
Plating Methods and How They Change the Part
The choice of method follows the geometry, the volume, and the tolerance requirement. Barrel plating tumbles small parts in a rotating drum, which suits high volumes of fasteners and small hardware but produces less uniform thickness and leaves contact marks. Rack plating hangs parts on a fixture, giving better control of thickness and finish on complex or large parts, at a higher labor cost. Reel-to-reel plating runs continuous strip for connectors and stamped parts, keeping thickness consistent across long production runs. The method is usually visible in the quote, and the buyer should ask which one applies to the part, because a barrel-plated part cannot hold the same thickness distribution as a rack-plated part.
Geometry drives uniformity more than the method name. Current density concentrates at sharp edges and projecting corners, and drops inside recesses, threads, and blind holes, producing the “dog-bone” effect where edges are thick and internal features are thin. Custom racking, auxiliary anodes, and shields compensate for geometry, and parts with complex internal features often need them before the process can hold tolerance. Designers can help by adding appropriate radii instead of sharp corners, which is one reason DFM review is worth doing before the finish is specified. The surface finishing service at 6CProto reviews the part geometry and the coating requirement together.
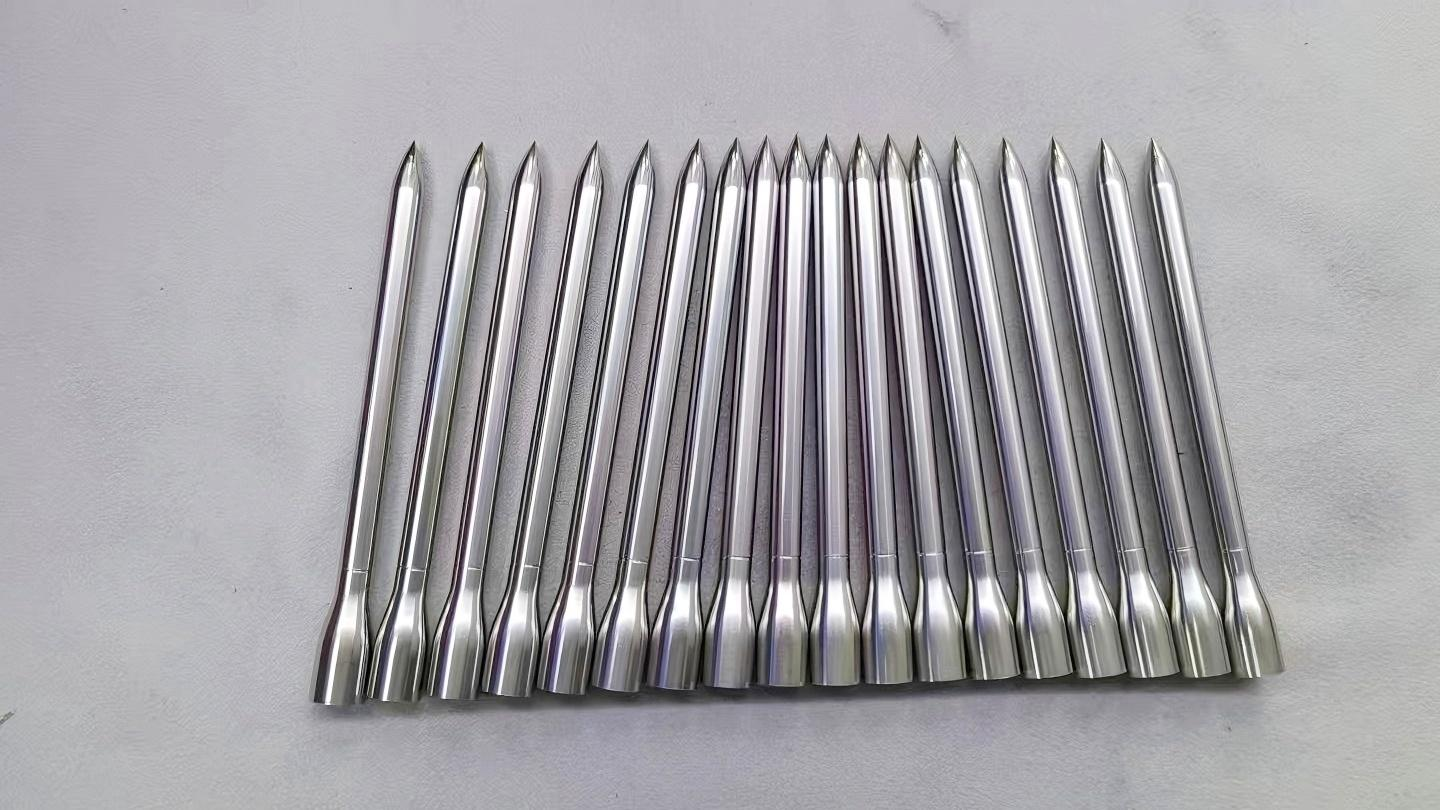
Material Selection for the Coating
| Coating | Primary function | Typical applications | Main limitation |
|---|---|---|---|
| Zinc | Corrosion protection | Fasteners, brackets, hardware | Wears fast; needs passivation |
| Nickel | Corrosion, wear, restoration | Worn parts, undercoats | Thickness control on edges |
| Hard chrome | Wear and friction | Hydraulic rods, tooling | Hydrogen embrittlement on hard steel |
| Gold | Electrical contact | Connectors, semiconductors | High material cost |
| Silver | Conductivity | RF parts, high-power switches | Tarnishes |
The substrate matters as much as the coating. High-strength steels risk hydrogen embrittlement, which requires a stress-relief bake after plating, typically within hours at 190–220°C; aluminum needs a zincate pre-treatment before most metal plating; and castings with surface porosity can trap chemistry and blister later. The plater should be told the base material, the hardness or heat-treatment state, and the final requirement, so the pre-treatment and post-treatment are planned instead of improvised.
Why Electroplating Fails in Production
The most common failures trace back to preparation and process control, not the chemistry. Surface contamination from cutting oil, scale, or oxides prevents a true metallic bond, producing porosity that traps moisture and later blisters or peels. Inconsistent current density, from poor racking or wrong anode placement, creates thick edges and thin recesses that fail the thickness callout even though the part looks plated. Hydrogen entrapment in high-strength steel can cause delayed cracking under load if the relief bake is skipped or delayed.
Each failure has a spec that prevents it. The drawing should state the base material and heat-treatment condition, the required thickness range, the acceptable edge condition, and any post-plate bake or sealing requirement. The plating supplier should confirm the pre-treatment sequence and the expected thickness distribution for the geometry before production, and the inspection should verify thickness at the locations that matter, not just in an easy-to-measure spot. For critical parts, the same inspection discipline that verifies machined dimensions should cover the plated layer.
How to Source an Electroplated Part
Sourcing electroplating well means choosing the responsibility boundary. A dedicated plating shop knows its chemistry lines but may have no upstream machining, so parts move between suppliers and traceability thins at the handoff. A broker passes the part down a chain with limited process control. An integrated manufacturer keeps machining and finishing under one quality system, which shortens lead time and keeps the records attached to the order. The right choice depends on the part: a simple fastener can travel to a specialist, while a precision assembly with a critical finish benefits from single-source accountability.
The documents matter. Ask for the coating thickness report, the pre-treatment and any bake record, and the specification reference, and confirm they cover the actual lot. For electronics, automotive, or medical parts, the compliance records should match the materials used, and the material selection and tolerance guidance on the site frame the choices before the finish is committed.
Alternatives Worth Comparing
Electroplating is not the only way to get a metal layer, and the alternatives often win on specific requirements. Electroless nickel deposits without current, giving uniform thickness on complex geometry and better corrosion performance, at a higher chemical cost. Anodizing is the default for aluminum, converting the surface rather than adding a layer, and it suits corrosion and cosmetic needs without the adhesion issues of plating on aluminum. Physical vapor deposition (PVD) produces thin, hard, decorative coatings at lower temperatures. The comparison belongs in the DFM review, because the choice changes the drawing callouts, the tolerance, and the inspection method.
Plating for Electrical and Signal Performance
Where the plated layer is part of the electrical system, the coating selection changes the design completely. Gold is the standard for contacts that must stay low-resistance across thousands of insertions, because it does not oxidize and presents a stable contact surface; silver offers the highest conductivity but tarnishes, which is acceptable in sealed or inert environments and a risk in open ones. Tin and tin-lead are chosen for solderable surfaces and cost, at the price of lower corrosion resistance and a surface that can grow whiskers under certain conditions. The plating thickness on a contact, often specified in microinches of gold over nickel, is a performance parameter, not a cosmetic one, and it should be selected with the expected cycle count and the mating material.
Electroless nickel deserves separate mention in electrical work because it deposits uniformly on complex geometry and on non-conductive surfaces after activation, and it provides a hard, corrosion-resistant base for a top coat. Many connectors use a nickel underlayer with gold on top, because the nickel blocks copper migration and hardens the surface while the gold provides the stable contact. The stack-up, nickel thickness, and gold thickness are defined together on the drawing, and the inspection verifies all three rather than the final layer alone.
Quality Records and Compliance
The compliance requirements attach to the materials in the bath, not to the finished part name. RoHS restricts substances such as lead, cadmium, and hexavalent chromium, and the certificate must reference the specific coating chemistry and thickness used on the part. For aerospace, medical, and defense work, the conformance records extend to the pre-treatment, the bath control, and the thickness report, and every lot should be traceable to the coating certificate. Asking for these records up front is cheaper than discovering their absence during an audit.
Buyers should also confirm the measurement plan. Thickness should be measured at the locations that carry the requirement, and the measurement method, X-ray fluorescence, cross-section, or a calibrated gauge, should be stated because methods do not agree to the same precision. The inspection plan and the tolerance guidance and the measurement practice maintained by NIST should cover the plated part the same way they cover the machined substrate, so the finish is controlled rather than assumed.
FAQs
What is the difference between barrel and rack plating?
Barrel plating tumbles small parts in a drum for high-volume, low-cost work, with less thickness uniformity and contact marks. Rack plating holds parts on fixtures for better thickness control on complex or larger parts, at higher cost.
How is plating thickness specified and measured?
Thickness is specified in micrometers or microinches on the drawing, and measured by X-ray fluorescence, cross-section, or a calibrated gauge at the locations that matter to the function. The measurement position should be stated with the requirement.
When does hydrogen embrittlement matter?
For high-strength steels, typically above about 40 HRC, plating creates a risk of delayed cracking under load. The standard control is a post-plating bake, and the requirement should be on the drawing with the material and hardness.
Can plated parts be machined after finishing?
Yes, but post-plate machining removes the coating at the machined surfaces. If a fit dimension must stay plated, it should be plated to spec after machining or machined with an allowance and then re-plated locally.