

A batch of anodized aluminum parts comes back with light spots at two corners — exactly where the parts hung on the rack during processing. The spots are not a coating defect; they are rack marks, and they were designed in when the drawing did not say which surfaces could carry contact points. Plating and anodizing are line processes: parts are racked, current flows to edges faster than recesses, and every masked or contacted surface tells a story. Designing the part with the finish line in mind — edges, threads, holes, and contact points — is what separates parts that finish cleanly from parts that finish with surprises.
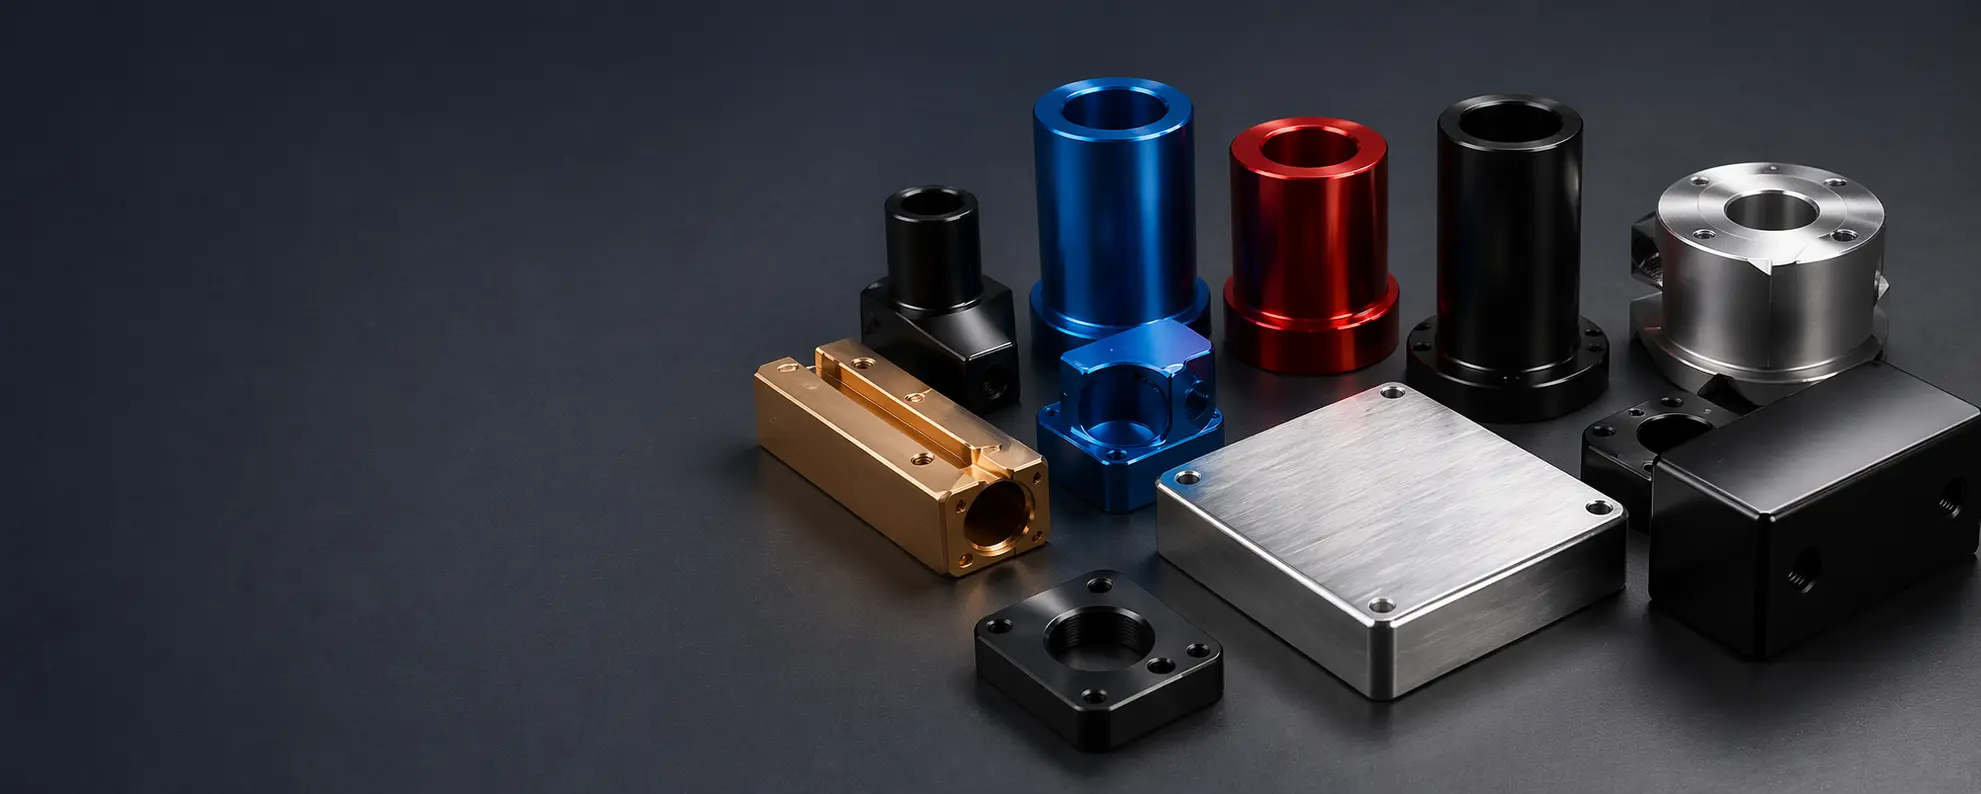
How finishing changes part geometry: edges, holes, and threads
Finishing changes dimensions and surface behavior in predictable ways. Anodic coatings grow from the surface and change the size of holes, threads, and fits; plated deposits add thickness that varies with current density; and coatings can close small holes or round sharp edges. The drawing should state which dimensions are measured before or after finishing, and the design should carry allowance for the features that matter. A hole that must accept a pin after anodizing needs a pre-coat size that accounts for the coating, and a thread that must accept a screw needs the same planning on the pitch diameter.
Sharp edges concentrate current in plating and build thicker deposits; in anodizing they can show different coating behavior and are prone to chipping. Where the part geometry allows, break edges deliberately and state the edge condition, so the finish does not decide the edge for you.
Racking and contact marks: designing for them
Parts must hang in the line, and the contact points leave marks: light areas where the rack shielded the surface, or small uncoated spots where the part touched the rack. The drawing should state which surfaces are functional and which may carry rack marks. If every surface is cosmetic, the finisher must use contact points that are later hidden or touched up, which adds cost; if the drawing allows rack marks on non-visible faces, the process is simpler and cheaper. Designers who never think about racking discover it at the first batch, when the visible face carries the mark.
For critical cosmetic parts, specify the allowed contact locations or require secondary masking and touch-up, and review the racking plan with the finisher before production. Rack marks are not defects when the drawing anticipated them; they are defects only when the drawing did not.
Current density and edge effects in plating
Electroplating deposits faster where current density is higher — typically on edges, corners, and protruding features — and slower in recesses and blind areas. The result is a thickness gradient that the part’s geometry controls: a sharp corner can build a heavy deposit while an internal corner plates thin. Designing for plating means avoiding extremes where possible, specifying the coating thickness at the functional location, and confirming the measurement point with the plater. If a recessed surface must be plated to a minimum thickness, the edges will be thicker, and the part should be designed to tolerate the difference or the process adjusted with shielding or anodes.
Anodizing is less current-density-sensitive than electroplating, but edges and high points still behave differently, and the coating on sharp edges can be less uniform. The finish requirement should be written for the functional surface, not as an average over the whole part.
Threads and close fits: coating allowance
Threads and close fits are where finishing allowances are most often forgotten. An internal thread that is tapped to size and then plated or anodized closes in and may reject the mating screw; an external thread grows beyond its class. The standard solution is to plan the allowance before cutting, mask the threads entirely, or chase them after finishing. The drawing should state which threads are coated, which are masked, and whether the fit is verified before or after coating. The same logic applies to press-fit diameters, bearing seats, and any surface with a controlled fit.
| Feature | Finish effect | Design response |
|---|---|---|
| Internal thread | Closes in with coating | Allowance, masking, or post-coat chase |
| External thread | Grows beyond class | Pre-plate undersize or mask |
| Press-fit bore | Size changes after coating | State before/after basis; allowance |
| Sharp edge | Heavier deposit or chipping | Break edges deliberately |
| Cosmetic face | Rack marks if contacted | Define allowed contact or masking |
The table is the design checklist for any coated part: name the feature, know the effect, and plan the response before the drawing is released.
Drainage, blind holes, and masking notes
Blind holes and closed volumes trap process fluids. A blind hole that is not drained can hold solution through rinses, contaminating later steps or leaving stains; a sealed internal volume can do the same. Design for drainage where possible — orient the part so holes drain, or add a small vent — and tell the finisher which holes must be clean and dry. Masking is the other half: features that must stay uncoated need a masking plan, and the drawing should list them so the finisher can price and plan the work. Masking compound left on a thread or a fit surface is a defect, so the removal step belongs in the process spec.
If the part is an assembly that will be finished as components and joined later, state which surfaces must stay bare for bonding, welding, or electrical contact. The finish line cannot read your assembly notes unless they are on the drawing.
A connector housing example shows the finish-aware design in practice. A machined aluminum housing will be anodized black, with threaded holes for the lid, a press-fit bore for a bearing, and a visible front face. The design review marks the front face as the cosmetic surface with the rack contact on the back, breaks the edges on the front, taps the threads with an anodize allowance or plans to chase them after coating, and sizes the press-fit bore with the coating growth in mind. The anodizer racks the part on the back face, masks the threads and the bore, and the finished part passes the fit checks without rework. The same housing designed without those notes would arrive with rack marks on the front, threads that reject the lid screws, and a bore that binds on the bearing — three defects from one finish step, each traceable to a missing note on the drawing. The example shows why finish design is part of the drawing: the edge break, the rack location, the masking list, and the coating allowance are all design decisions that the finisher cannot invent correctly. When the drawing carries them, the finish step is a controlled process; when it does not, the finisher makes the decisions by default, and the defaults rarely match the function. The housing that finishes cleanly is the one whose geometry and notes anticipated the line it would run on.
Before release, run the finishability review: mark the cosmetic faces and allowed rack locations, break the edges that will be coated, list the masked threads and bores, state the coating allowance on fits, and plan the drainage of blind holes. Send the review with the drawing so the finisher prices the masking and the process from the same list. The five notes are the difference between a part that finishes cleanly and a part that finishes with a dispute.
Frequently asked questions
Can anodizing be stripped and redone if the color is wrong?
Yes, anodic coatings can be stripped, but the process removes a small amount of material and can change the surface, so it is not free. Stripping is practical for rework on valuable parts; for a color problem, understand whether it is the alloy, the batch, or the process before replating, because the same result will repeat if the cause is unchanged.
Should sharp edges be rounded before plating?
Usually yes. Sharp edges concentrate current and build heavy, sometimes brittle deposits, and they are prone to chipping in handling. Break the edges to a controlled radius or chamfer, state the edge condition on the drawing, and the finish will be more uniform and durable. The edge break is a design decision, not a shop courtesy.
How do you specify which surfaces are masked?
Mark them on the drawing or in a finish note: list the threads, bores, datum faces, or contact surfaces that must remain uncoated, and state why. The finisher prices the masking and the risk from that list, so an accurate list produces an accurate quote. Unspecified masking is the most common source of finish disputes.
The finishable part in one paragraph
Design the part for the finish line: break the edges, plan the coating allowance on threads and fits, decide where rack marks can live, drain the blind holes, and list the masked surfaces. Finishing is not a magical last step that adapts to any geometry — it is a process with contact points and thickness gradients, and the parts that finish cleanly are the ones whose drawings anticipated them.
If you are designing a part that will be plated or anodized, the 6CProto surface finishing team can review the geometry, the allowance, and the masking plan before the drawing is released.