

Five-axis machining is a capability, not a badge of quality. For simple parts, it is usually the more expensive way to get the same result, and choosing it out of preference or habit raises cost, lead time, and programming need with no return. This article makes the case for when not to use 5-axis: which parts are better off on a 3-axis machine or a simpler route, what the real cost structure is, and how to decide based on the part instead of the machine.
5-Axis Solves a Specific Problem
Five-axis machining earns its cost when the geometry needs continuous tilt or when one setup must reach several faces. Its benefits are fewer setups, better tool engagement on contours, and the ability to reach complex features. If the part does not need these, the machine’s advantages do not appear and its costs do.
The Cost Structure of 5-Axis
A 5-axis machine costs more per hour, and complex toolpaths cost more in programming and simulation. For a simple part, that higher hourly rate is pure premium: the part takes the same or longer than its 3-axis equivalent, and the program cost is amortized over few parts. The comparison is per delivered part, and simple parts lose on 5-axis.
What Simplifies Onto 3-Axis
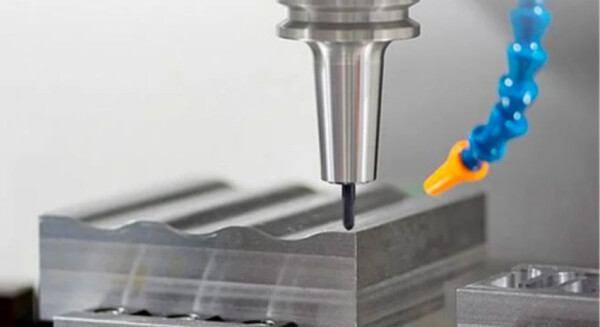
Parts that are mostly one or two faces, parts that need no tilt, and parts with prismatic geometry usually machine at lower cost on 3-axis. One or two setups, straightforward programming, and standard tooling make 3-axis the sensible default. The exceptions are the parts that specifically need the fifth axis.
Warnings: Cost, Lead Time, and Fixturing
Using 5-axis on simple parts raises the quote and often the lead time, adds simulation and fixture complexity, and uses capable machine time that could be making parts that need it. If the geometry is simple, ask why the recommendation is 5-axis before accepting it. A supplier that recommends the right machine for the part, even when it is simpler, is the partner to keep.
A Decision Test
- How many setups does the part need on a 3-axis machine?
- Does any feature require continuous tilt or a reach a fixed axis cannot make?
- Is the extra programming and machine time worth the part’s geometry?
If setups are few, the feature reachable with a fixed axis, and the program simpler, the part does not need 5-axis.
The Bottom Line
5-axis machining is the right answer when the geometry asks for it, not when the capability is available in the building. For simple parts, a 3-axis machine or a conventional route gives the same quality at lower cost and less lead time. Ask the process question honestly, let the part decide, and reserve the five-axis hours for the parts that genuinely need them. That is how the cost-benefit works out in your favor.
Note: costs and capability vary by shop and part; confirm the process recommendation and why with the supplier before committing tooling time.