

What Defines a High-Speed Spindle
High-speed spindles are motorized machining units that rotate cutting tools at 20,000–60,000+ RPM to enable fine finishes, small-diameter tooling, and faster feeds on softer materials. They excel in mold finishing, micro-machining, and precision prototyping where surface quality and detail outweigh heavy material removal.
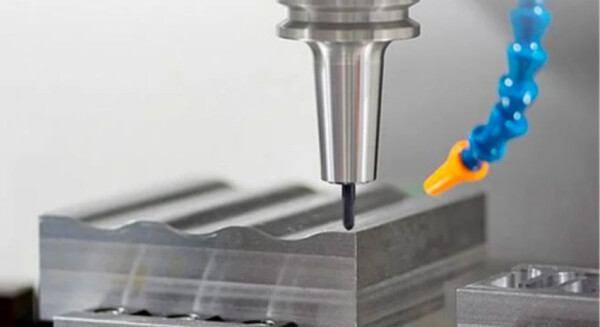
A high-speed spindle is an integrated motor-spindle unit designed for 20,000–60,000+ RPM, using hybrid ceramic bearings, HSK tooling, and active cooling to maintain accuracy at speed. Conventional spindles often rely on external motors with belts or gears to deliver high torque at lower speeds, typically under 12,000 RPM. The high-speed design integrates the motor directly around the spindle shaft, reducing mass and inertia for faster acceleration and tighter control. This sacrifices low-speed torque but enables consistent performance with small tools that would chatter or break on slower machines.
Key technical distinctions include:
- Bearings. High-speed units use silicon nitride ceramic balls to reduce heat and friction, where conventional spindles often use steel bearings.
- Cooling. Liquid cooling jackets are standard to dissipate motor and bearing heat; conventional spindles may rely on air or intermittent cooling.
- Toolholding. HSK (Hollow Shank Taper) is common for its rigidity and balance at high RPM, while CAT or BT tapers dominate conventional setups.
- Power curve. High-speed spindles deliver power through speed rather than torque, which requires lighter depths of cut and higher feed rates.
Applications Where High-Speed Spindles Deliver
High-speed spindles give the greatest advantage in mold and die finishing, micro-machining, aerospace brackets, medical implants, and electronics housings, where fine surface finishes and tight tolerances matter more than material removal rate. Typical use cases include:
- Mold and die finishing. Semi-finishing and polishing of aluminum or pre-hardened steel molds with ball-nose end mills under 6 mm diameter.
- Micro-machining. Drilling holes under 1 mm or milling fine features in medical devices and micro-electronics.
- Aerospace. Machining thin-walled aluminum or titanium components where chatter must be minimized.
- Prototyping. Rapid iteration of detailed parts in plastics, aluminum, or composites with minimal post-processing.
High-speed spindles are not ideal for every scenario. Roughing a large steel forging or cutting deep slots in titanium favors a high-torque spindle that can sustain heavy cuts at lower RPM. The choice follows the speed-torque profile matched to the material, tool size, and desired surface finish. For finishing work on parts that need tight tolerances, the precision machining route at 6CProto uses such spindle and process selection as a starting point for the tolerance plan.
Selecting Speed and Torque for the Material
Select spindle speed and torque by calculating the required surface speed for the material, then matching it to the tool diameter and available RPM, while ensuring the spindle can deliver enough torque to avoid stalling under load. The basic relationship is: RPM = (SFM × 12) / (π × tool diameter in inches).
For aluminum, typical SFM ranges from 1,000–2,500; for steel, 200–600; for titanium, 100–300. A 3 mm (0.118 in) end mill in aluminum at 1,500 SFM requires roughly 48,000 RPM, well within high-speed spindle territory. The same tool in steel at 400 SFM drops to about 13,000 RPM, where torque becomes more critical. In practice, the tool diameter drives the decision: as tool diameters fall below 6 mm, the RPM required to reach the recommended surface speed climbs, and only a high-speed spindle can deliver it.
Practical selection steps: identify the material and its recommended SFM from tooling charts; calculate the target RPM from the tool diameter; verify the spindle’s torque curve at that RPM can sustain the chip load; then adjust feed rate and depth of cut to stay within the spindle’s envelope and the tool’s limits. The strategy on the machine differs from convention: shallower depths of cut at higher feed keep chip loads reasonable, because a high-speed spindle removes material by edge speed, not by force.
Spindle Types and Their Trade-offs
Integral motor spindles dominate production CNC machines and rapid prototyping services, where consistency and uptime matter. Air turbine spindles are niche tools for specialized micro-work such as engraving, PCB drilling, and ultra-fine finishing, but they are not suitable for heavy cuts and need clean, dry air. High-frequency belt-driven units from 12,000–40,000 RPM offer better low-end torque than integral designs and suit prototyping and mixed-material shops, at the cost of more vibration and belt maintenance. Belt-driven units can also introduce more runout and require periodic tensioning, so the choice between them is a trade between torque, runout, and service.
Thermal Management Is Part of Accuracy
High-speed spindles generate significant heat in the motor windings and bearings, which causes expansion, runout drift, and loss of accuracy if not controlled. Without active cooling, thermal growth can exceed 10–20 microns over a shift, which is enough to ruin a tight-tolerance part. Liquid cooling systems circulate chilled water or glycol through jackets around the motor and bearing housing to maintain a stable temperature, typically within ±1°C of a setpoint. Some advanced spindles monitor bearing temperature and adjust coolant flow dynamically.
Neglecting cooling leads to premature bearing wear from lubricant breakdown, spindle nose expansion that changes tool runout mid-job, and motor insulation degradation that ends in failure. In rapid prototyping, where jobs change frequently and cycle times are short, consistent thermal performance keeps the first part and the fiftieth part within the same tolerance.
Bearing and Toolholding Choices
Hybrid ceramic bearings and HSK toolholding minimize runout and imbalance at high RPM, directly extending tool life and improving surface finish. Ceramic bearings reduce friction and heat, allowing higher speeds with less lubrication, and they resist deformation under centrifugal force. HSK toolholders use a hollow, short taper with face-contact design that centers the tool more accurately and resists pull-out under high centrifugal loads.
Typical runout targets are 3–5 microns at the nose for standard CAT40, 1–2 microns for HSK-E32/40, and under 1 micron for precision HSK with balanced holders. Even 2 microns of runout can double the load on one flute of a 2 mm end mill, causing chipping or breakage. For micro-machining, shops invest in balanced shrink-fit HSK holders and inspect runout with a test bar before critical jobs.
Validation Before Production Runs
Before production, validate spindle runout, thermal stability, and toolholding accuracy with a test bar, dial indicator, and temperature monitoring. A recommended workflow: warm up the spindle per manufacturer guidelines, often 10–15 minutes at moderate speed; mount a precision test bar and measure runout at the nose and 100 mm out; run a short test cut and measure part dimensions with a CMM or micrometer; monitor spindle temperature during a 30-minute continuous run to check for drift; then inspect tool wear and surface finish on the test part.
If runout exceeds 2 microns at the nose for fine work, investigate toolholder seating, taper cleanliness, or bearing preload. Thermal drift beyond 5 microns over 30 minutes may indicate inadequate cooling or ambient temperature swings. In rapid prototyping, where first-part correctness is crucial, these checks prevent costly rework and missed deadlines. The inspection side of such validation follows the same logic as any critical-dimension part: the measurement method is agreed before the run, not after the nonconformance. For that framework, the 6CProto CMM inspection article describes how scope and evidence are agreed for critical machining.
What to Ask When Sourcing a Spindle
Consult spindle manufacturers, machine tool integrators, and process engineers who understand your material mix and tolerance requirements. The conversation should start with the part, not the catalog: the tolerance, the tool diameter, and the material define the envelope the spindle must cover. Ask about torque curves, cooling specifications, bearing life, service intervals, and compatibility with your existing tooling and controls. Key questions include: what is the continuous and peak torque at my target RPM range; what cooling system is required and what happens if coolant flow is interrupted; what bearing life is expected under my duty cycle and how is it monitored; which toolholding standards are supported and what runout can I expect; and how is the spindle specified for thermal stability between runs?
There is no standardized industry-wide definition of “high-speed” for spindle ranges, so the specification belongs on the machine, not in the marketing material; the external reference for dimensional accuracy conventions in machining is the standards catalog at NIST.
Frequently Asked Questions
What RPM range qualifies as high-speed for spindles?
High-speed spindles typically operate from 18,000 RPM up to 60,000+ RPM, with some air turbine units exceeding 100,000 RPM for specialized micro-machining. Conventional spindles usually stay below 12,000 RPM.
Can I use a high-speed spindle for heavy steel roughing?
Not effectively. High-speed spindles lack the low-end torque needed for aggressive material removal in hardened steels. Use a high-torque spindle for roughing, then switch to a high-speed unit for finishing if needed.
How often do high-speed spindle bearings need replacement?
Bearing life depends on speed, load, and cooling, but typical service intervals range from 5,000 to 15,000 hours. Monitoring temperature and vibration helps predict end-of-life before catastrophic failure.
Is HSK toolholding mandatory for high-speed spindles?
Not mandatory, but strongly recommended. HSK provides better balance, rigidity, and runout control at high RPM compared to CAT or BT tapers, especially for tools under 6 mm diameter.