

Explore 3D Printing Design, Materials & Finishing
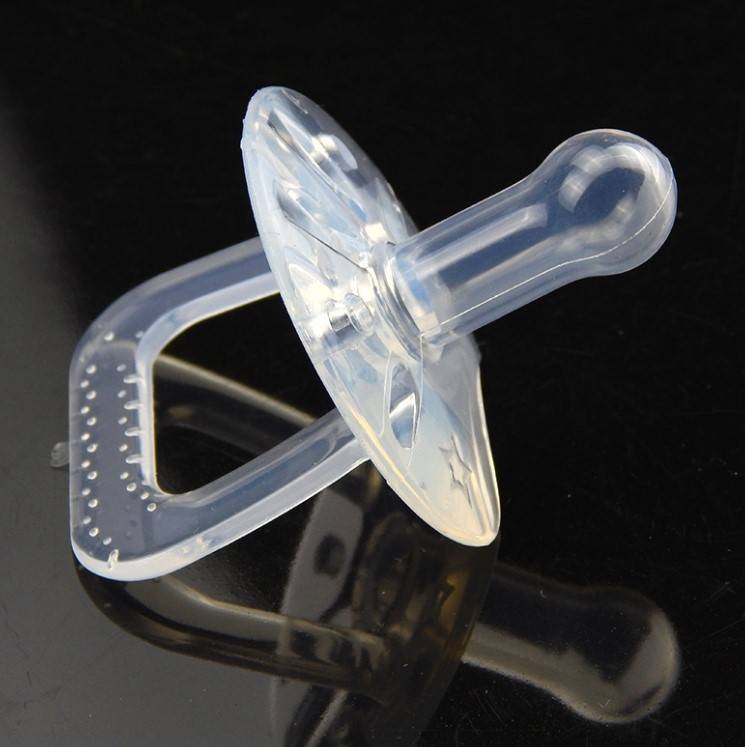
A housing that needs a sealing lip, a handheld device that needs a soft grip, or a wearable that must flex thousands of times without tearing—these are the parts where rigid printing reaches its limit and thermoplastic polyurethane (TPU) starts. TPU prints parts that bend, compress, and spring back, which changes the design conversation completely: instead of stiffness and strength, the engineer thinks in hardness, tear resistance, and abrasion resistance. The payoff is custom geometry without tooling—a seal shaped exactly to a housing, a gasket with integrated features, a soft-touch cover matched to a specific product—produced directly on a printer and ready for iteration with the design.
Flexible Printing Is a Different Material World
Designing for flexible printing means thinking in elasticity. The part must bend without breaking, compress and recover, and survive repeated use—and the design decisions (hardness, wall thickness, geometry) control how it behaves. The opportunity is custom geometry: where molded elastomers need tooling to justify their per-part economics, printed TPU produces the part directly, which makes it the fast route for custom flexible parts at any quantity. What matters is that the buyer names the application before the material is chosen. A seal needs compression and recovery; a gasket needs a specific hardness and fit; a soft-touch cover needs feel and durability. The TPU grade and the wall design follow the application, not the other way around.
Three properties define a flexible part. Hardness, often measured on the Shore scale, sets how the part feels and how much it deflects under load. Tear resistance sets how it survives cuts and repeated bending. Abrasion resistance sets how it wears in contact. The selection follows the job: a soft-touch cover wants a soft durometer, a gasket that must seal under compression wants the right balance of hardness and recovery, and a protective bumper wants tear and abrasion resistance. The material data sheet is the starting point, but the part’s own test is the evidence—a seal that is pulled and stretched, a cover that is handled daily, and a bumper that is scraped should each be tested for the critical behavior rather than trusted to a datasheet.
How TPU Prints: Process and Material Forms
TPU enters the additive workflow in two common forms, and the choice affects what the part looks like and how it behaves. Filament-based printers push a TPU filament through a heated hotend and lay the melted material down in layers—simple, low-cost hardware that suits prototype seals and soft-touch covers where layer lines are acceptable. Powder-bed systems, by contrast, fuse fine TPU particles layer by layer, which produces denser, more uniform parts with finer feature detail; because the process can leave unfused powder inside enclosed cavities, the geometry must allow the powder to be removed after printing. The first question for any flexible part is therefore not "can you print TPU?" but "which TPU form and which printer class matches the part’s accuracy, surface, and post-processing needs?" The polymer materials overview is a useful starting point for that comparison.
Print orientation matters more for flexible parts than for rigid ones. A seal printed standing on edge will have layer lines running across the sealing face, which can create microscopic leak paths along the layer boundaries; the same seal printed flat may seal better but need more support structure. Because TPU is soft, layer fusion is influenced by temperature and layer time, and thin walls can delaminate if the previous layer cools before the next is deposited. The printability review should therefore confirm the orientation, the minimum wall the material can fuse reliably, and the support removal plan before the first part is made.
Seals and Gaskets That Work
Printed TPU seals and gaskets earn their place in prototypes and low-volume applications: custom shapes that match the housing, integrated features like locating ribs or crush zones, and quick revision when the design changes. The seal’s function depends on three things: compression, recovery, and dimensional fit. The seal is compressed against a mating surface to create sealing force, and compression set—how much the material recovers after the squeeze—determines long-term sealing. The design should set the compression level explicitly and test recovery on the actual part.
The limits are printing tolerance and material behavior. A printed seal holds a custom shape but may not match the surface finish or consistency of a molded seal, and a seal that is too thick or too thin changes the compression and therefore the sealing force. Buyers should specify the fit and tolerance, and confirm the print tolerance on the actual geometry—adjusting the part where needed. For high-volume or high-performance sealing, molding returns; the printed version is the fast, custom answer, and the transition happens when the design stabilizes and the quantity grows. That handoff is a design transfer: the printed part serves as the reference for the mold, so print-friendly geometry should be reviewed for draft, parting lines, and wall changes before the move to casting.
Soft-Touch and Wearable Parts
Soft-touch parts add a flexible layer to products—handles, covers, and wearable components that must feel comfortable and grip well. Printed TPU produces these directly in the product’s shape with the hardness tuned to the feel. The wearable consideration is durability: repeated flexing, washing, and contact. TPU survives these better than many rigid materials, but the design should avoid sharp corners and thin sections that concentrate stress, and the material should be chosen for the fatigue it will actually see. The feel is validated on the prototype—the hardness, texture, and fit are judged in the hand—so the buyer should test the prototype with real users before volume, because the feel is the product. When production volume grows, the same design often moves to molding, which is where the material comparison between printed and molded flexible routes becomes a quantity decision.
Printing Limits: Supports and Overhangs
Flexible materials print within the same geometric physics as rigid ones, plus added behavior: soft TPU can be difficult to support and remove, and thin flexible sections may sag or deform. The practical rule is to design conservatively—adequate wall thickness, support-friendly geometry, and margins for the material’s softness. Overhangs that a rigid material bridges will droop in a soft one, and supports that snap off a stiff part cleanly can tear or leave witness marks in a flexible part. The printability review is worth the time; a few minutes of geometry review before the build avoids a failed print and a redesign cycle. For complex flexible parts, this is where experience with TPU printing matters more than with rigid polymers, because the failure modes are different.
Durability Testing: Tear, Abrasion, and Compression Set
A flexible part earns its place through repeated use, and three tests capture the failure modes that matter. Tear testing measures how the part survives cuts, notches, and repeated bending—critical for a seal that is stretched over a lip or a cover that is handled daily. Abrasion testing measures surface wear in contact, which decides whether a grip stays grippy after months of use. Compression set testing answers the sealing question directly: it compresses the material for a defined time and temperature, then measures how much the part recovers, with the method referenced in ASTM elastomer testing standards. A gasket that loses 50 percent of its thickness after compression will not seal tomorrow even if it sealed today. The datasheet gives a starting point for each property, but the part’s own test is the evidence—the geometry, infill, and layer structure of a printed part can change the effective property from the datasheet value.
Temperature changes the picture. TPU behaves differently across its service range: the material stiffens in the cold and softens in the heat, and the compression set and tear results shift with it. A seal that works at room temperature may leak in a cold warehouse or squeeze out in a hot enclosure. The buyer should state the operating temperature band and test the critical behavior at the relevant end of that band, rather than assume room-temperature performance carries over. That is why the engineering conversation should start with the flex, load, and environment the part will actually see—the same three inputs a supplier needs to recommend a TPU grade or recommend casting instead.
TPU Printing vs. Silicone Casting
| Factor | TPU printing | Silicone casting |
|---|---|---|
| Tooling | None | Mold required |
| Speed | Fast for one-off | Mold build time, then fast per part |
| Material range | TPU grades | Silicone and PU grades |
| Surface quality | Printed texture | Molded smoothness |
| Quantity | Single digits | Tens to hundreds |
The cost comparison should include tooling and per-part lines: printing has no tooling and a higher per-part cost, while casting adds the mold and reaches a lower per-part cost. The crossover follows the quantity, so the buyer should compare the totals at the actual volume rather than assume one route wins. The casting route’s advantages are surface quality and material range, and the economics improve as quantity grows. The transition from print to cast is a design transfer—the printed prototype validates the geometry and feel, and the cast version reproduces them—so the geometry should be reviewed for draft, parting lines, and wall changes before the move. For flexible parts produced in single digits, the printed route is almost always the faster, cheaper answer; at tens to hundreds of parts, urethane casting services take over.
FAQs
What can TPU printing produce?
Seals, gaskets, soft-touch covers, custom dampers, and wearable parts—anything that needs to bend, compress, and recover in a custom shape.
How do I choose the TPU hardness?
Match the hardness to the job: soft for touch and conforming seals, firmer for structural flex and wear. Tear and abrasion resistance follow the use case, and the part’s own test—not just the datasheet—should confirm the choice.
When should I cast instead of print a flexible part?
When the design stabilizes and the quantity grows. Silicone casting offers better surface quality and a wider material range at tens to hundreds of parts; printing wins the first custom part.
What are the printing limits for TPU?
The same geometry physics as rigid printing, plus soft-material behavior: supports can be hard to remove, and thin sections may sag. Design conservatively and confirm printability before the build.