

Explore Injection Molding Design & Tooling
An indexing cam on a packaging line looks correct in CAD and jams on the first test build. The mechanism that looks right in the model — linkages, cams, gears, and actuators — reveals its real behaviour only when it moves, and the failure is expensive if it is discovered after tooling. Rapid prototyping validates mechanisms before the tooling investment: functional prototypes in production-like materials, tested for motion, interference, and load. This guide covers the method, the materials, and the checklist that gates tooling.
Mechanisms Fail on Paper, Then Again in Steel
A mechanism’s behaviour — friction, compliance, backlash, and failure modes — is not fully predictable from a model. Paper analysis finds the obvious problems; the subtle ones appear when parts move against each other. Discovering them after tooling means a mold or die revision, which is the expensive discovery.
Rapid prototyping moves the discovery earlier: the mechanism is built in prototype materials, run through its motions, and tested for the failure modes that matter. Tooling is committed only after the mechanism has proven itself in motion. The prototype is a system test — the linkage, cam, gear, and actuator are assembled and run together, because the behaviour emerges in the assembly. Prototype the system, not the individual parts, and run the mechanism through its envelope, because the failure modes are the design’s information.
Prototyping Linkages and Cams
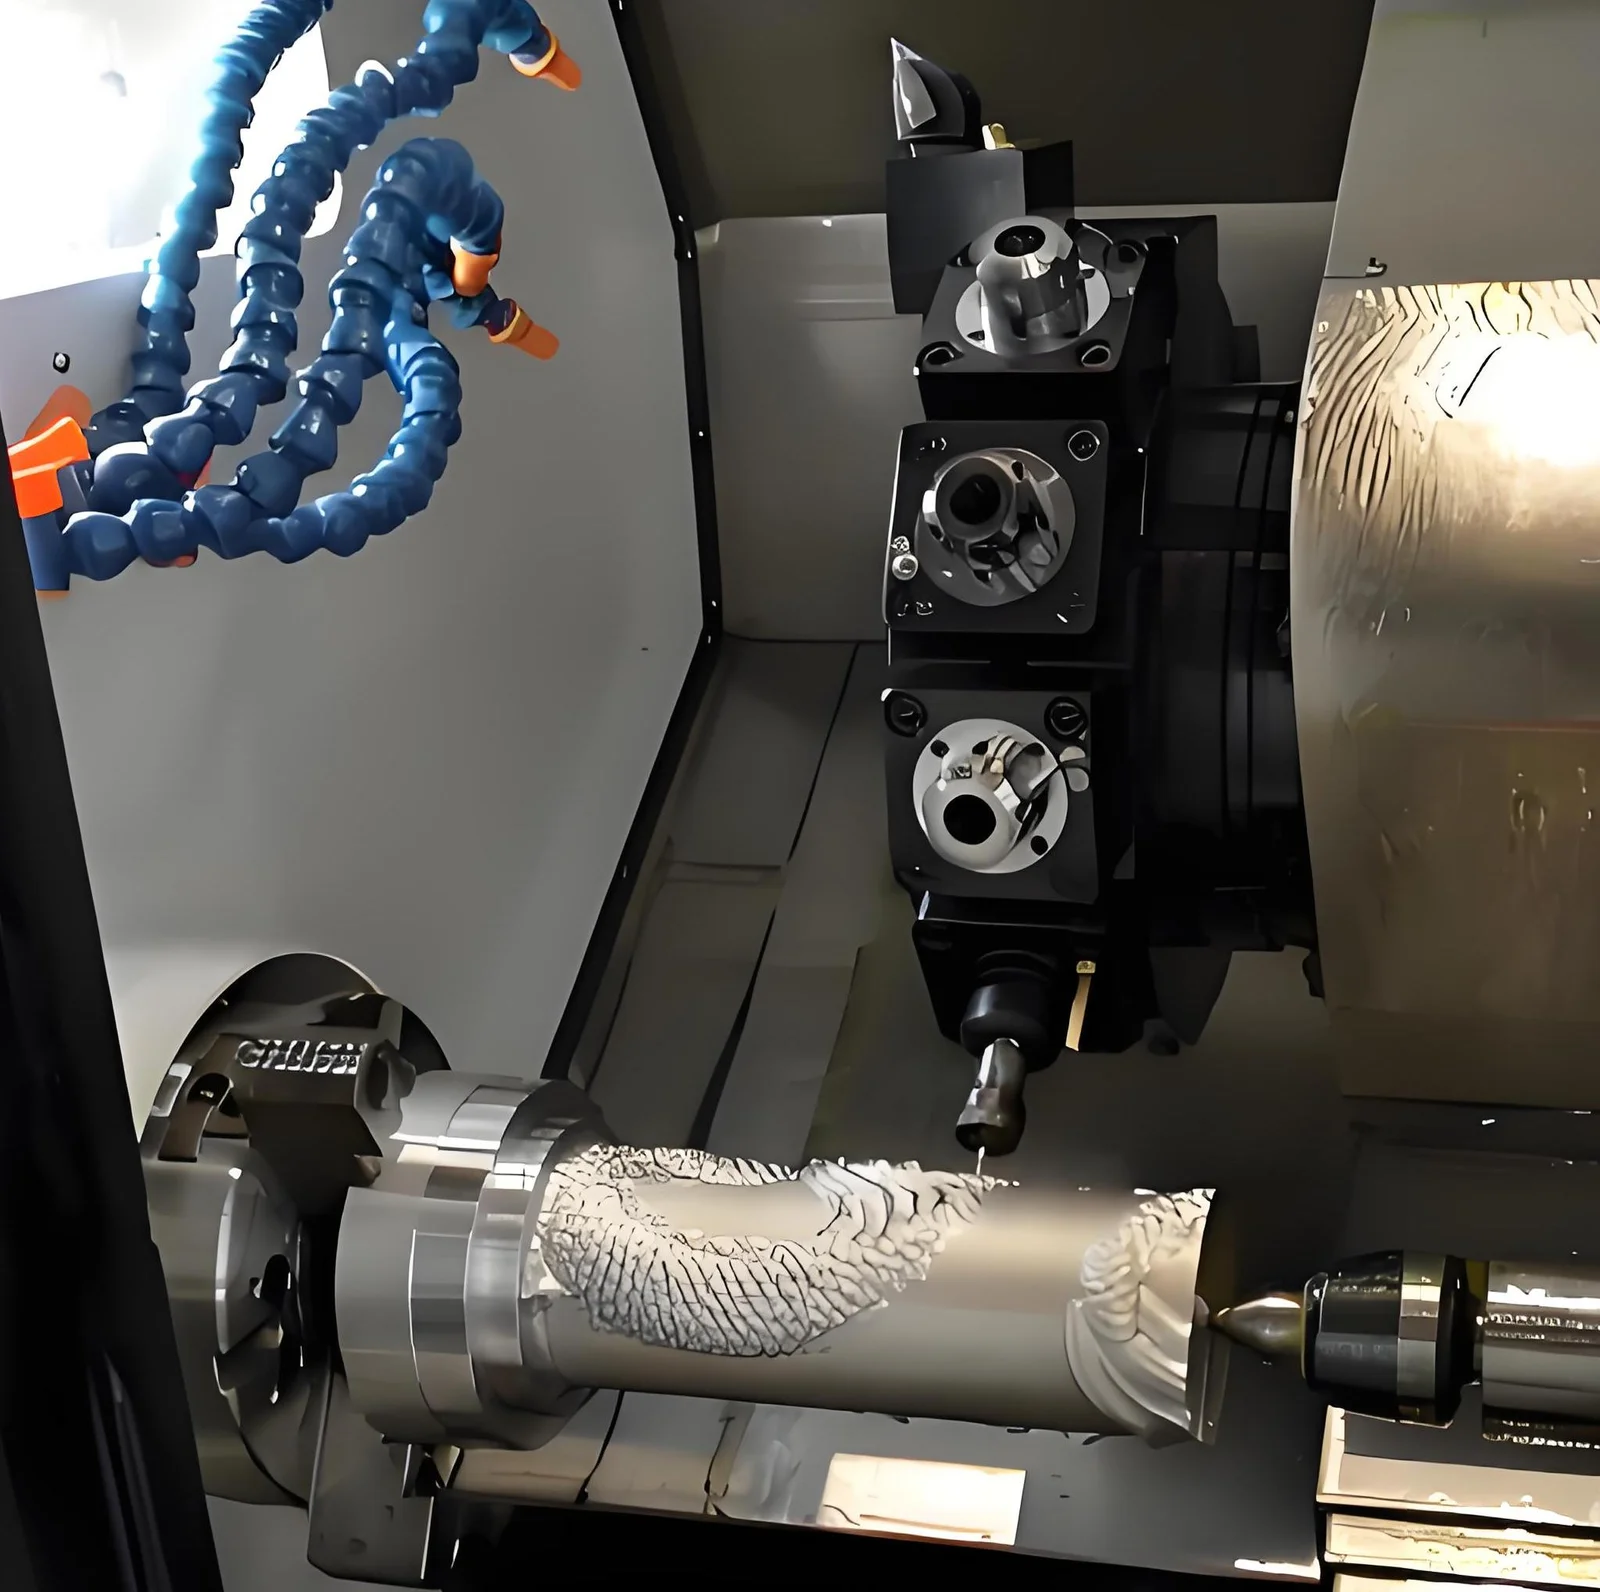
Linkages and cams translate motion, and their prototype validates the kinematics: travel, timing, and force. The prototype parts must hold the geometry — link lengths, cam profiles, pivot positions — because the motion depends on them. A 0.2 mm error in an effective link length shows up as a phase error at the output, so geometry fidelity is a test-validity requirement, not a cosmetic one.
The materials for motion testing need the stiffness and wear behaviour of the production part, or close enough for valid results. Machined or printed parts in engineering materials carry the loads and reveal behaviour the CAD model could not. The linkage prototype’s joints are the test points: pivot friction, bearing clearance, and compliance are measured and compared with the model, because the mechanism’s feel is in its joints. The cam prototype’s profile is the machining detail: the cam is machined or printed to profile, the follower’s motion is tested against the design, and the profile is corrected where it deviates.
The kinematic test needs a defined envelope. Record travel at the input and output, measure timing against the cycle, and check the force at each dwell point rather than only at the extremes. A cam with a tight rise segment, for instance, accelerates the follower through the transition; if the spring or return force in the prototype cannot control the follower, the production part will chatter at the same transition point. The improvement that comes out of the test is usually a profile revision or a spring-rate change — both cheap before tooling, both expensive after it.
Gear and Transmission Mock-Ups
Gears and transmissions test meshing, backlash, and load capacity. A prototype gear set shows how the teeth engage, where noise comes from, and how the assembly behaves under load — and the prototype material must survive the running-in and the test loads. The validation value is the failure data: a gear that wears early, a mesh that binds, or backlash that is too large all appear in the prototype run. Fixing the design before tooling is the entire point.
Run the set at operating load and speed, and observe wear and temperature. That data is the capacity evidence. Where the transmission will see duty cycles rather than constant load, the test should mirror the real profile — a repeat-start, reverse, or shock-load segment changes the wear picture completely. A prototype that passes at 50% load may fail at the real load, so specify the load with the test.
Backlash deserves its own measurement. Backlash tolerance is an assembly property as much as a tooth-geometry one: it depends on centre distance, tooth tip clearance, and how the gear set is mounted. Measure it at the slowest speed where it is worst, then confirm it under load, because loaded backlash differs from static backlash. If a gear set needs machined blanks to carry that load, our precision machining service produces the functional gear prototypes that survive running-in; the robotics industry page shows these components in actuated systems.
Functional Materials for Motion Testing
Motion testing depends on materials that behave like production. Nylon prototypes carry loads and wear in useful ways; machined metal prototypes match production behaviour closely; printed parts validate geometry and mechanism concept. The material choice follows the test: what the mechanism must survive and what the results must prove. The rule is to state the test requirement and choose the material that makes the result valid — a mechanism tested in a material far from production produces misleading data.
Machined metal shares the stiffness and friction of the production part, which is why functional linkage and cam tests usually start there. Nylon earns its place in contact mechanics: it has a low coefficient of friction against steel, so a nylon-on-steel joint tells you whether the geometry will bind before surface wear dominates the result. Printed parts earn their place in geometry and interference checks, where surface behaviour is secondary. The material’s data should be confirmed with the supplier — grade, condition, and behaviour — so the prototype represents the production part. The rapid prototyping service page explains how prototype material selection is matched to the test plan.
Interference and Assembly Checks
Mechanisms are assemblies, and assembly is where interference appears: parts that collide, fasteners that bind, and clearances that vanish under load. The prototype assembly check runs the full mechanism together, verifying motions and clearances. The check is both static and dynamic — assembled clearances at rest, and clearances under motion and load. The failures it finds, a link that hits a housing or a pin that walks out, are the classic tooling surprises, caught early.
Treat the assembly check as a fixture-and-datum exercise. Parts are assembled on their locating features, and clearances are measured against the assembly datums, which also verifies the assembly logic itself. Where the industrial design uses sheet-metal shrouds or brackets around the mechanism, verify those clearances too — a housing that is 0.5 mm too close to a moving link is a binding failure at speed. Run the dynamic check at the mechanism’s real speed as well as its slow crawl: clearance that looks generous statically can vanish under an accelerating link, and resonance appears only in a speed sweep. The sheet metal fabrication service covers the housings, brackets, and guards that surround the mechanism, and the design-for-manufacturing checklist helps catch geometry that will fight the process later.
The Before-Tooling Validation Checklist
Before committing tooling for an industrial mechanism, work through the checklist:
- Has the mechanism run through its full range of motion in prototype?
- Are the loads and speeds tested at the real operating values?
- Have interference and clearances been checked in assembly, statically and dynamically?
- Have the wear and failure modes been observed and recorded?
- Have the functional materials matched production behaviour?
- Have the findings been fixed and re-tested?
The checklist is the gate between a validated mechanism and the tooling investment, and it doubles as the evidence package for the tooling RFQ. Validation results, fixed findings, and re-test data accompany the request, and the supplier reviews them before committing tooling. A gate that is shared is a gate that is sound.
Plan the validation as a schedule with the tooling date on it. Each design revision triggers a re-run of the motion and interference checks, so the milestone plan should budget time for the fix-and-re-test loop rather than assuming one pass. Recording the findings matters beyond the current project: the measured friction and wear data becomes the input for the next mechanism with the same architecture, which is why the record should note the material, the load, the speed, and the failure mode together.
Validate Your Mechanism
Industrial equipment rewards mechanism validation before tooling. Linkages, cams, gears, and assemblies prove themselves in prototype, and the failures discovered there are the ones that save the tooling budget. The industry context for these parts is covered on the industrial equipment manufacturing page, and the guide to planning a prototype program helps sequence the validation milestones against the tooling date.
Conclusion
The mechanism’s prototype is a system test: linkages, cams, gears, and assemblies run, hunt for failures, and fix the design while changes are cheap. The validated mechanism is the gate to tooling. Define the test loads and motions, choose the prototype materials, and run the validation checklist — with findings fixed and re-tested — before committing tooling, and keep the evidence record as the basis for the tooling decision. The ISO standards library is a useful reference when writing the test and documentation requirements for the tooling contract.
FAQs
Why prototype a mechanism before tooling?
Because behaviour — friction, backlash, compliance, and failure modes — appears only in motion. Finding problems in prototype is cheap; finding them in tooling is expensive.
Which materials suit motion testing?
Production-like materials for valid behaviour: machined metal or nylon for load and wear, printed parts for concept and geometry. The material must make the test results meaningful.
What should the prototype assembly check?
Interference and clearances, statically and under motion and load. Run the dynamic check at real speed as well as at crawl speed, because clearance that looks generous statically can vanish under an accelerating link.
What is the gate before tooling?
The validation checklist: full motion range tested, loads and speeds at real values, interference checked, failure modes observed, materials matched, and findings fixed and re-tested.