

Explore 3D Printing Design, Materials & Finishing
Metal 3D printing is expensive in time, not just in powder. The powder is the visible cost, but machine hours, support removal, heat treatment, and inspection usually cost more than the material. Understanding the four cost blocks — powder, machine time, post-processing, and inspection — explains why complex geometry costs more, and when metal printing beats machining. All figures here are illustrative scenarios, not quotations.
Metal Printing Is Expensive in Time, Not Just Powder
The common assumption is that metal powder drives the price. In practice, machine time dominates for most parts: each layer is built slowly, the build is limited to what fits the machine, and the part’s height drives the hours. Powder matters, but the clock matters more.
Machine time is a layer-count story. Build height sets the number of layers, and each layer takes time to scan and fuse; a tall part costs more than a short one even when the volume is similar. Build volume is also a constraint: the part must fit the machine with supports and clearance, and packing multiple parts into one build spreads the machine time across them. Height and packing are the main levers on the machine-hour cost, which is why quoting a print normally starts with a build simulation rather than a simple volume calculation.
Build-plate economics follow from that. A build that runs overnight carries the same machine time whether it holds one part or several, so packing multiple parts into one build lowers the per-part machine cost. Buyers who plan quantity and part sizes together can pack the builds efficiently. That is why the cost conversation is really a geometry conversation — a part that is tall, dense, or poorly packed takes more machine hours, while a part designed for the process costs less.
The Four Cost Blocks of a Metal Print
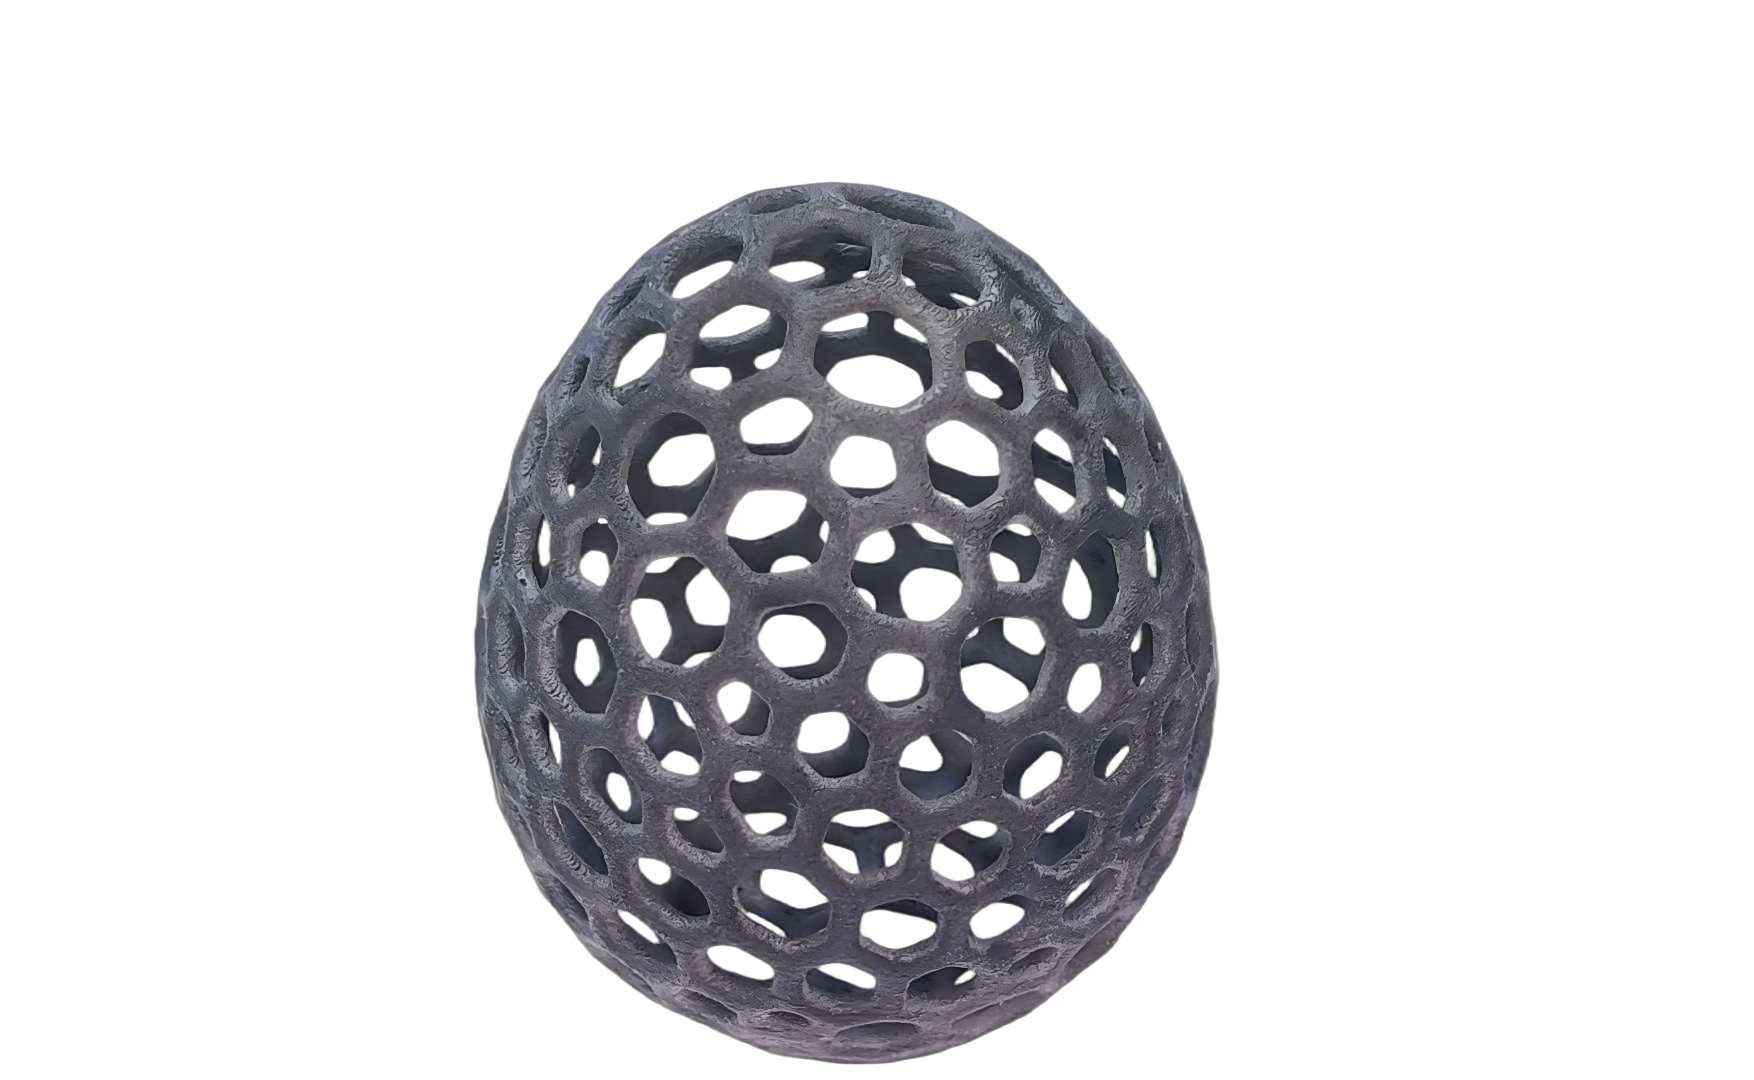
The cost of a metal-printed part sits in four blocks: powder and material, machine time, post-processing, and inspection. The blocks behave differently. Powder is proportional to volume and material; machine time follows build height and packing; post-processing follows the geometry’s complexity; inspection follows the tolerance and the application. Reading a metal-printing quote means seeing all four.
Powder cost includes the material and its recovery. Unfused powder is sieved and reused, and the recovery rate and powder quality affect both cost and part quality. A part that uses powder efficiently — hollow sections, optimized geometry — costs less in material and machine time. Do not assume the powder is a fixed line; the design controls it.
The inspection block grows with the application. A metal print for a critical application carries CT or density checks, dimensional verification, and material testing, and each adds cost. State the inspection scope with the order, because the metal part’s quality evidence is part of its price. A quote that separates inspection is a quote that can be compared, because the verification scope is explicit rather than buried in the part price.
Post-processing is where metal printing’s cost curve climbs. Support removal, heat treatment, and machining of critical faces add the operations that turn a printed part into a finished part. The quote should list them — a part that looks cheap in the build looks different once the post-processing column is filled in. The 3D printing service page covers metal processes such as SLM with titanium, aluminium, stainless, and Inconel options, and the 3D printing materials page compares powder options by property and cost.
Geometry That Multiplies Cost
Certain geometry multiplies the cost blocks: tall parts that consume build height, dense solid sections that use material and time, internal channels that are hard to clean, and thin features that need careful support and risk failure. The design response is to minimize them: orient the part for the shortest build, hollow solid sections where possible, and design for easy support removal.
Internal channels are a defining case. A drilled hole through a machined part is near-free; a printed channel that needs support removal and internal cleaning is a post-processing project. The same geometric feature sits at completely different costs in the two routes. Thin fins or lattice walls need a support strategy per feature, because a collapsed thin wall wastes the build and the material. Tall parts interact with the printer’s z-axis limits and the recoater cycle, so reorienting a part from standing to lying can cut several hours out of a build while costing nothing in design intent. Design-for-cost rules for metal printing are the same physics as design-for-print rules: shorter builds, lighter sections, and accessible features.
When Metal Printing Beats CNC Machining
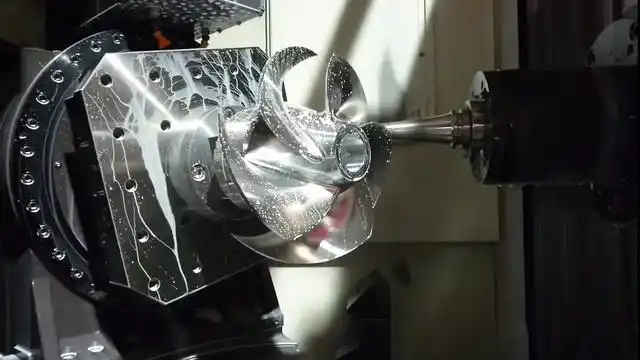
Metal printing earns its cost where machining struggles: internal channels that cannot be drilled, lattice structures, complex internal geometry, and parts where design freedom saves weight or assembly. The crossover with machining depends on geometry and quantity — printing wins on complexity, machining wins on simple geometry and higher volumes.
The comparison should be made per part: quote the machining route and the printing route for the same function, including post-processing, and let the geometry decide. An impeller with internal cooling channels is a printing part; a flat bracket is a machining part. The comparison should also include inspection and qualification — a printed part for a critical application carries material and density evidence that a machined part from certified stock may not need. Compare the full routes, not just the printing and machining lines.
Quantity moves the crossover. A complex part that is expensive to print may be economical at one-off and prototype quantities; the same part at production volume may favour a hybrid — printed for the complex core and machined for the interfaces. The printing route pays its setup once and repeats machine time per part, while machining spreads its setup across the batch, so the crossover price moves with the volume under consideration. The deeper comparison between the routes is covered in metal 3D printing vs. CNC machining, which walks through the same decision per part.
A Cost-Planning Table for Buyers
| Cost block | What drives it | Planning question |
|---|---|---|
| Powder / material | Volume, alloy, recycling | Can the section be hollowed or lightened? |
| Machine time | Build height, packing, layers | Can the orientation shorten the build? |
| Post-processing | Supports, machining, heat treatment | Can geometry be designed for easy support removal? |
| Inspection | Tolerances, application, reports | Which dimensions truly need verification? |
The table turns the quote into a design review, which is where the saving happens. Walk the part against the four blocks — where the volume can be hollowed, where the orientation can shorten the build, where supports can be reduced, and where inspection can be scoped — and the review produces the design changes. Make those changes before the quote, not after.
Use the table per part, not per program. Two parts in the same envelope can sit at opposite ends of the cost profile: one tall and dense, the other short and hollow. Priced together, the average hides both the opportunity and the risk. The same discipline applies to the material spec — powder size distribution and alloy choice are quoted inputs, and changing them after the first build changes the cost block, so settle material and orientation before requesting the quote.
Requesting a Comparable Metal 3D Printing Quote
The final input is the RFQ itself. Material, quantity, critical surfaces, and inspection scope belong in the RFQ because they set the four blocks. A complete RFQ gets a complete cost plan; one with gaps gets a quote full of assumptions. For a head-to-head route comparison, the CNC machining quote should be requested against the same drawing and the same post-processing scope, so the two routes are priced on equal terms. Material property references such as ASTM standards help define the verification and qualification scope before the quote, so the inspection block is priced on the same basis by both routes.
Conclusion
Metal 3D printing costs sit in four blocks, and geometry drives the expensive ones. Machine time follows the build, post-processing follows the design, and inspection follows the application. When the comparison with machining is made per part, the geometry decides — complexity belongs to printing, simplicity to machining. Document the function and quantity, ask for both routes, and review the cost plan against the geometry.
FAQs
Why is metal 3D printing expensive?
Because machine time, post-processing, and inspection cost more than the powder. Build hours follow the geometry, so complex or tall parts carry the cost.
How can I reduce metal printing cost?
Design for the process: shorten the build by orientation, hollow solid sections, reduce supports, and specify inspection only where it matters.
When does metal printing beat CNC machining?
For internal channels, lattices, and complex internal geometry that machining cannot produce. The crossover depends on geometry and quantity, so compare both routes per part.
What post-processing do metal prints need?
Support removal, machining of critical surfaces, and heat treatment such as annealing, ageing, or HIP for demanding applications. The plan is part of the cost and schedule.