

Explore Sheet Metal Processes & Supplier Selection
A product is rarely one process. The enclosure may be sheet metal, the internal parts machined, the small components printed, and the whole finished and assembled — and each process is an interface that can fail. Multi-process low-volume manufacturing puts the processes under one program: one supplier coordinating CNC, sheet metal, finishing, and assembly, with the quality documentation unified. Fewer interfaces mean fewer failure points. This guide covers when the approach helps and how to manage it.
Fewer Interfaces, Fewer Failure Points
Every supplier boundary is a failure point: the part that does not fit the next process, the finish that does not match the sample, the schedule that slips between vendors. Multi-process manufacturing removes the boundaries by keeping the processes in one program.
The value is coordination. The supplier owns the transitions — where machining meets sheet metal, where finishing meets assembly — and the buyer owns one relationship instead of three. The trade is trust in a single partner, which is why the partner’s process management matters. Verify the CNC, sheet metal, finishing, and assembly range before the order, and agree how transitions, schedules, and issues are communicated across the stages.
Common Process Combinations
The common combinations follow the product: an enclosure project combines sheet metal fabrication with machined brackets and finishing; a device project combines machined internal parts with printed components and assembly; a production program combines CNC, finishing, and inspection under one flow. The supplier’s range — CNC, sheet metal, printing, casting, finishing — determines how much of the product can stay in the program. List the parts and their processes, confirm the product’s coverage, and sequence the stages for assembly.
Managing Transitions Between Processes
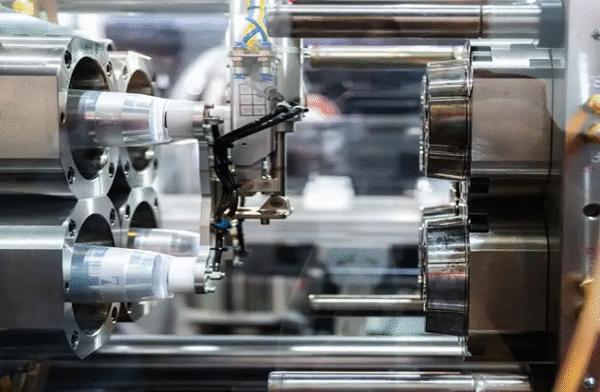
The transitions are where multi-process work is won or lost. A machined part that must fit a sheet-metal assembly needs its tolerance defined against the assembly; a printed component that receives a finish needs the surface prep coordinated. The transitions are engineering decisions, not handoffs.
Define the interfaces on the drawing: which dimensions mate across processes, which finishes apply where, and which tolerances the assembly requires. The program manages the transitions because it owns both sides. Check the assembled fit at the transitions — the verification that is done is the one that protects. A tolerance defined for a single part but never checked against the next process will fail at assembly, not at inspection.
Maintaining One Quality Thread
Multi-process work needs a unified documentation set. The material certificates, inspection reports, and finishing records should be tied to one order and one traceability thread, so an audit can follow a part from raw stock through machining, sheet metal, finishing, and assembly without re-asking at each step. Define the documentation scope at RFQ — which certificates, which dimensions, which revision — because the cost and the process follow the scope.
Planning the Schedule and Communication
The program lead time is the longest chain, and coordination makes it visible. Each stage carries its own window, and the program schedule joins them at the assembly and finishing points. Review the chain with the program manager before the order starts, so the critical path is known in advance. Plan a buffer where the processes meet — the handoff between stages is where delay appears — rather than padding the end of the schedule. Set communication milestones: what is reported, when, and by whom, so issues surface while they are still cheap to fix.
A Program-Management Checklist
- Are the processes defined and the interfaces on the drawing?
- Is the process sequence planned with overlaps?
- Is the documentation set unified across the processes?
- Are the tolerances between processes defined?
- Is the program timeline confirmed at quoting?
- Is a single owner accountable for the program?
Combine Your Processes in One Order
Multi-process low-volume manufacturing removes the interfaces that fail. CNC, sheet metal, finishing, and assembly coordinated under one program, with unified documentation and a coordinated timeline, deliver the product as one effort. 6CProto’s low-volume manufacturing service, CNC machining service, and sheet metal fabrication service cover the process range, and the program can be structured as one order. When you request a quote, describe the product, its processes, and the timeline, and the engineering team can confirm the program structure and documentation.
Conclusion
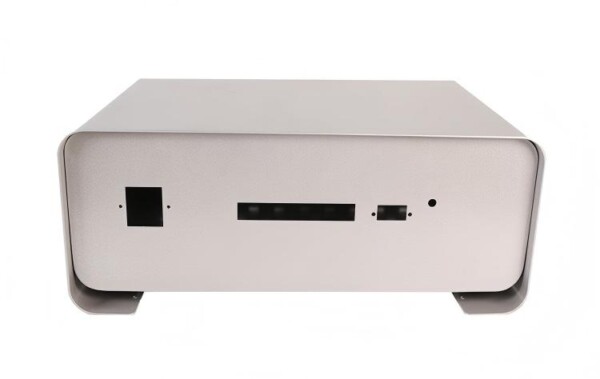
Multi-process low-volume manufacturing removes the interfaces that fail: the processes are coordinated under one program, the documentation is unified, and the timeline overlaps. Fewer interfaces mean fewer failure points — when the transitions are engineered. The next step is to define the processes, the interfaces, and the timeline, and request the program as one coordinated order.
FAQs
Why combine processes under one supplier? Because every supplier boundary is a failure point. One program owns the transitions between processes, the documentation, and the schedule, reducing interfaces and coordination risk.
Which processes are commonly combined? Sheet metal with machined parts and finishing for enclosures; machining with printing and assembly for devices; CNC with finishing and inspection for production programs.
How are multi-process lead times coordinated? By overlapping the processes — machining while sheet metal runs, finishing when parts arrive — so the program time is less than the sum of the processes. Confirm the timeline at quoting.
What documentation should a multi-process order carry? A unified set covering the whole product: material certificates, inspection reports, and finishing records for the parts and processes, tied to one order and one traceability thread.