

Specifying sheet metal tolerances means defining acceptable dimensional variation for cut, formed, punched, and welded features so parts assemble reliably without paying for precision the design does not need. Tolerances are a cost budget, not a quality score: every tightened number carries tooling, setup, cycle-time, and inspection cost, and the relationship between tolerance and cost is exponential rather than linear. The discipline is to apply realistic defaults broadly and tighten limits only where function demands it. This article walks through process capability bands, bend-related stack-up, standards, and the shop-floor controls that hold the numbers.
What Tolerances Exist for Each Fabrication Process
Tolerance capability depends on the process, because each process adds its own error sources. The comparison across processes applies the same logic to machining and other routes, not just sheet metal. Machining removes material from a rigid block; sheet metal bends and stretches thin stock across multiple machines, accumulating stack-up error at every step. Practical bands for a well-run shop:
- CNC machining: about ±0.13 mm standard, ±0.025 mm precision; limited by tool deflection and thermal drift.
- Laser cutting: ±0.13 to ±0.25 mm standard, ±0.05 mm precision; thinner stock holds tighter kerf edges than thick plate.
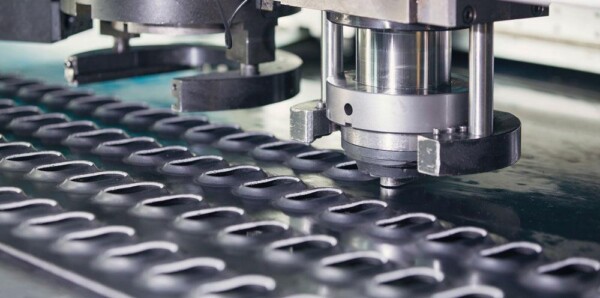
- Punching and stamping: about ±0.25 mm standard, ±0.10 mm precision; die wear dictates long-run drift.
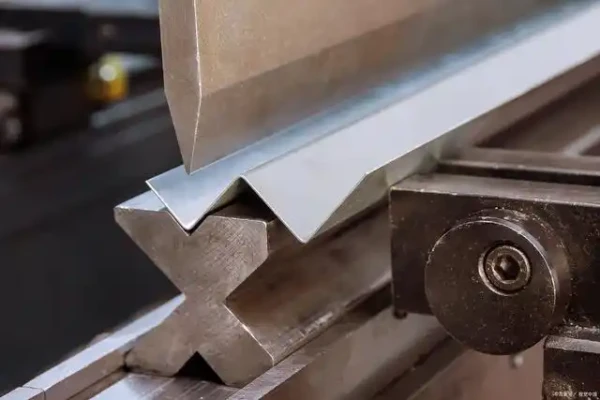
- Sheet metal bending: ±0.25 to ±0.50 mm standard, ±0.10 to ±0.20 mm precision; springback dominates and varies with grain orientation.
- Waterjet cutting: about ±0.25 mm standard, ±0.08 mm precision; a cold cut avoids thermal distortion.
- Plasma cutting: ±0.76 to ±1.50 mm standard; a wide kerf and large heat-affected zone make it unsuitable where precision matters.
- Welding and assembly: ±0.76 to ±1.50 mm standard; localized heat causes warpage unless parts are clamped.
These bands are the baseline conversation. Typical feature-level expectations follow the same logic: overall linear length at ±0.20 to ±0.50 mm standard, hole diameter at ±0.10 to ±0.20 mm, hole-to-hole spacing on one plane at ±0.13 mm, bend angle at ±1°, and flange length at ±0.25 to ±0.40 mm. Precision versions of each cost more and are justified only at functional interfaces. Note the difference against machining: CNC machining tolerances run tighter because one rigid setup eliminates the bend-related error chain that sheet metal accumulates.
Single-Surface versus Multi-Surface Tolerances
The single most useful tolerance concept in sheet metal is the difference between features on one flat surface and features that cross bends. Features cut in a single setup—the flat 2D laser bed or punch press—share the machine’s reference, so edge-to-edge, edge-to-hole, and hole-to-hole relationships on one surface typically hold about ±0.13 mm. The same relationship measured across a bend does not, because every bend adds springback variation, thickness effects, and angular error into the dimensional chain.
The practical mapping for formed parts: a one-bend step runs about ±0.38 mm between bends; multi-bend relationships, opposing-plane features, and enclosure-spanning measurements grow to ±0.76 mm, with roughly ±1° of angular stack added per bend. A hole located relative to a bend perches on both error sources at once. This is why “tolerance ±0.13 mm” on a drawing is nearly meaningless by itself—the question is which features it is referenced to. Dimension features from functional datums such as locating tabs or hole clusters, not from vague outer corners that shift during forming.
Stack-Up Analysis Prevents Assembly Failure
Tolerance stack-up analysis calculates the cumulative variation of interconnected features and answers one question: will the parts fit in the worst case? The classic failure is an enclosure lid held to ±0.13 mm hole-to-hole on its flat surface mating to a chassis box whose mounting holes cross two walls and multiple bends, accumulating ±0.76 mm of error plus angular stack. The round clearance holes in the lid cannot absorb that variation, and the assembly fails with bolt binding or forced distortion—not because any single feature was out of tolerance, but because the tolerance chain was never budgeted.
The engineering fixes are simple and cheap when applied early: oversize the clearance holes to absorb the stack, elongate one hole into a slot, or use floating clinch nuts inside the chassis. A stack-up spreadsheet run before cutting metal turns a guaranteed assembly problem into a non-event.
Using Standards and GD&C to Communicate
Two standards frameworks keep prints clean. ISO 2768 defines general tolerance classes—f (fine), m (medium), c (coarse), and v (very coarse)—that apply automatically when specific callouts are omitted. A title block line such as “General Tolerances ISO 2768-m” sets the default for everything, so the drawing carries numbers only where they are needed. ASME Y14.5 and GD&T add the geometry-level controls: true position defines a cylindrical tolerance zone for hole patterns, flatness controls warpage on sealing faces, and perpendicularity regulates bend angles between panels. The result is prints that say the same thing to the designer, the fabricator, and the inspector. Standards do not replace judgment—an ISO class is a baseline, and the functional interfaces still get individual callouts where sealing or structural performance demands them. The governing standards themselves are maintained and published through organizations such as the ASME codes and standards program.
Material choice changes what is achievable. Carbon and stainless steel hold dimensional stability well; stainless work-hardens and raises tool wear during punching. Aluminum machines easily but expands with heat, so warpage must be managed. Copper smears at edges instead of shearing cleanly and needs sharp tooling, while free-cutting brass holds reliable control. Titanium concentrates heat at the cutting edge and accelerates tool wear, yet springs back minimally once formed. The material column belongs in the tolerance conversation from the start, and the material data sheet should accompany the drawing when the band depends on it.
Prototype Tolerances versus Production Tolerances
Early prototypes and production runs should not carry the same tolerance scheme. A functional prototype exists to validate fit, stiffness, and assembly, so standard ISO 2768-m bands and a short list of critical dimensions are usually the right level: they are fast to inspect and cheap to revise. The same part moving to volume production can hold tighter bands on the features that matter, because tooling and process control justify and pay for the inspection. Tightening early adds cost exactly when the design is most likely to change.
The transfer works the other way too: prototypes are the chance to prove which dimensions actually need precision. Watch where the real assembly stresses appear, which holes find the fasteners, and which faces seal. Those observations become the red callouts on the production drawing, while the thousands of other dimensions stay under the general note. Tolerance is a budget, and the prototype program is where the budget gets spent wisely.
Shop-Floor Control That Holds the Band
Tolerances are written on the drawing but earned on the floor. The control loop runs: verify incoming sheet stock thickness and mill certificates, lock tooling codes and program parameters in setup, run a first-article CMM inspection against CAD datums before production, record the frozen setup in job routing, hold in-process gauge checks across the run, and audit the finished parts before shipment. Each step catches a different failure class: stock thickness variation overbends or binds flanges, uncalibrated fixtures and worn tooling drift dimensions, and skipped first-article checks let a bad setup run for an entire batch. For flat-sheet features such as hole patterns, laser cutting keeps accuracy consistent across the whole pattern instead of decaying with tool wear.
A practical drawing strategy keeps this loop affordable. Use red callouts for critical interfaces such as sealing faces and primary mounting holes, yellow for structural flanges and alignment tabs, and green for cosmetic edges governed by the general note. Dimension from functional datums, avoid redundant chain dimensions so one non-critical feature absorbs cumulative variation, and consolidate defaults in the title block. A flange at ±0.10 mm that locates a fluid gasket is engineering; the same number on a decorative cover edge is waste. The fabrication route itself should be matched to the forming method early, so the called-out band and the process capability agree before the first bend.
In practice, the best tolerance scheme is the one the shop can hold and the inspector can verify. Everything else—the standards, the classes, the bands, and the shop-floor checks—exists to make that agreement explicit before the metal is cut, and to keep the parts within it.
Frequently Asked Questions about Sheet Metal Tolerances
What general tolerance should I use for typical parts?
ISO 2768-m (medium) is the practical baseline for most industrial and consumer applications: cost-effective limits that hold adequate alignment for general assemblies. Add tighter bands only to specific functional interfaces.
Can I rely on one global tolerance note?
For simple flat parts, yes. For formed assemblies with critical hole patterns or sealing faces, a global note invites misaligned mounting features or unnecessary cost. Use the global note as the default, then call out the interfaces that need tighter control.
Do tighter tolerances mean higher quality?
No. Quality means meeting functional requirements reliably. Over-tight specifications on non-critical features increase cycle time, tooling wear, inspection overhead, and scrap without improving the product—the classic over-spec failure.