

Two acronyms, one machine family, and a specification conversation that often goes nowhere useful. Engineers comparing DMLS and SLM usually already know that both melt metal powder with a laser; what they need is the set of decisions that actually differ on a purchase order, and the language to compare two quotes without being misled by the label each supplier prefers. This comparison covers the origin of the two terms, what changes in practice on layer thickness, surface finish and material range, how tolerance and post-machining allowances are affected, and what to ask before awarding a job.
Are DMLS and SLM the same process?
In practice, yes – both are laser powder bed fusion.
Both labels describe one build mechanism, and machines in both camps consolidate powder into a dense part.
The distinction originated in marketing and patent language rather than in a process boundary. Direct metal laser sintering was the term popularised by one equipment line, and selective laser melting by another, at a time when the degree of melting was a genuine differentiator. Today the machines used for production parts melt the powder in both cases, and the resulting density is comparable when parameters are set correctly.
What that means for a buyer is straightforward: asking whether a supplier runs DMLS or SLM tells you very little. Asking which alloy, which layer thickness, which machine platform, how powder is managed across build cycles, and which operations are included in the price tells you almost everything. Those answers determine whether the part meets its drawing, and they are the same questions regardless of which acronym appears on the quote.
The vocabulary itself is maintained through the standards work coordinated by ASTM committee F42 on additive manufacturing, and the measurement side of the same field is described in the NIST additive manufacturing program.
Where do the terms come from, and how are they used today?
From machine marketing, now used interchangeably.
The terms once described different levels of consolidation; today both are shorthand for the same process family.
The terminology matters in one practical situation: comparing quotes or reading a supplier’s capability statement. A shop that advertises DMLS and another that advertises SLM may be describing the same equipment, the same alloys and the same achievable result. Treating the labels as different technologies leads to comparisons that have no meaning, and sometimes to a supplier being excluded for using the wrong word.
Related terms appear in the same way. Laser powder bed fusion is the umbrella description used in current standards, and it covers both labels. Where a specification or a customer’s quality system uses one term, the useful response is not to argue about the name but to confirm the parameters behind it: the alloy grade and powder specification, the layer thickness, the build orientation, the heat treatment, and the machining allowance.
Written into a drawing, the process name alone carries little information. A note that names the alloy, the required density or inspection method, and the surfaces to be machined conveys far more, and it survives a change of supplier without being renegotiated.
What changes in layer thickness and surface finish?
Layer thickness trades build time against surface quality.
Thinner layers produce a smoother as-built surface and more accurate detail at the cost of machine time, while thicker layers build faster and leave a coarser finish that finishing operations have to remove.
Layer thickness is one of the few parameters that changes the outcome in a way a buyer can see. A thinner layer reduces the visible stepping on angled and curved surfaces, improves the resolution of small features, and increases the number of passes required, which extends build time. A thicker layer does the opposite: faster build, coarser surface, and a greater likelihood that a fine feature needs machining rather than printing.
The consequence for a drawing is that surface finish and build time are linked, and specifying both loosely leaves the supplier to choose. Where a face is cosmetic or functional, it is cheaper to machine it than to print it finely, because machining reaches a defined finish with a predictable allowance. Where the face is internal or hidden, the as-built surface is usually acceptable, and the coarser layer setting saves time.
Upward-facing and downward-facing surfaces behave differently at the same layer thickness, because adhesion of partially melted powder is worse on the underside of a part. That is one more reason to place critical faces in the build orientation where they are least affected, and to leave machining allowance on any face that cannot be positioned well.
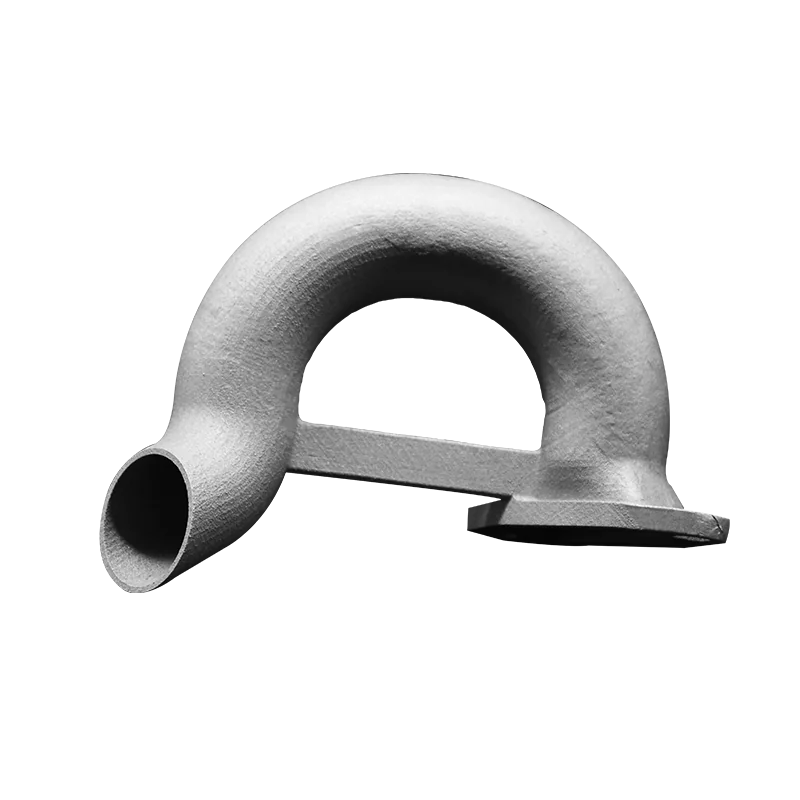
Does the material range differ between them?
In principle no; in practice it depends on the supplier.
Both labels describe machines that run the same alloy families, and which alloys are actually available depends on what the supplier stocks, validates and can machine afterwards.
The alloy families used in laser powder bed fusion are consistent across the industry: aluminium alloys for lightweight parts, stainless steels for corrosion resistance and general engineering, titanium alloys where strength-to-weight matters, nickel superalloys for high-temperature service, and tool steels for conformal-cooled mold inserts. Which of those a given shop offers is a commercial and technical decision, not a consequence of the process name, and the grades 6CProto runs for metal printing are listed on the metal 3D printing service page.
Two practical questions follow. First, what is the powder specification and how is powder managed across build cycles, since recycled powder behaves differently from fresh material. Second, what supporting operations are available in-house, because heat treatment and machining capacity determine whether the part can be delivered finished rather than as a near-net shape that the buyer has to route elsewhere.
| Comparison point | What to ask | Why it changes the part |
|---|---|---|
| Alloy and powder | Exact grade, powder specification, recycling policy | Behaviour and traceability |
| Layer thickness | Value used for this geometry | Surface finish, detail, build time |
| Orientation | Build angle and support plan | Distortion and support scars |
| Heat treatment | Cycle and whether it is included | Residual stress and dimensional stability |
| Machining | Which faces are machined and to what callout | Fit, sealing and function |
| Inspection | What is measured and what documentation follows | Acceptance and traceability |
How do tolerance and post-machining allowances differ?
Not by label; by orientation and machining plan.
As-built tolerance depends on geometry, orientation and thermal history, so the machining allowance is a design decision.
Two effects move a metal part away from nominal. Thermal distortion accumulates during the build and is partly released when the part is cut from the plate. Surface adhesion adds material on downward-facing and vertical surfaces, where partially melted powder bonds to the skin. Both effects vary across a single part, which is why a blanket tolerance on an as-built metal part is unreliable.
The response is to leave machining allowance on the faces that will be cut, and to keep that allowance generous enough to absorb both effects. That decision belongs in the model and the drawing, and it should be confirmed with the supplier, because the amount needed depends on the geometry and the orientation rather than on a standard figure. Faces that must not be machined, such as an internal channel surface, need to be positioned and supported so that the as-built condition is acceptable.
The framework for how those callouts are handled across processes is set out on 6CProto’s standards and tolerances page, and the geometry rules that keep a part machinable after printing are collected in the 3D printing design tips library.
How do cost and lead time compare?
They follow the plan, not the acronym.
Build time scales with part height and layer count, alloy price varies between stainless and nickel grades, and post-processing is usually a separate line.
For two quotes describing the same part, the differences that change the price are usually identifiable. A thinner layer setting increases machine time. A denser support structure increases removal labour. A machining operation on four faces costs more than one on two. Heat treatment and pressing add both cost and lead time. And an exotic alloy adds material cost plus machining time, because titanium and nickel alloys are harder to cut than stainless.
Lead time follows the same structure, with one addition: whether the powder is in stock. A grade that has to be ordered in extends the schedule before the build even starts, which is worth confirming against a launch date rather than assuming. Where a program runs repeat orders, the more useful question is how the shop sequences work, since a part that can share a build plate with other jobs is scheduled differently from one that needs a dedicated plate.
How should the process be specified on a drawing?
By alloy, requirement and machining plan, not by acronym.
A useful note names the alloy and its powder specification, the machined surfaces and any post-processing, leaving the process label to the supplier.
That structure removes the ambiguity that the two labels create. Instead of asking for DMLS or SLM, the drawing states what the part must be: this alloy, these interfaces machined to these callouts, this surface finish, this inspection documentation, and this heat treatment. A supplier can then respond with the platform, layer thickness and orientation that meet the requirement, and the comparison between two quotes becomes a comparison of scope rather than of vocabulary.
It also protects the buyer during a supplier change. A specification written around requirements can be quoted by any capable shop, whereas one written around a proprietary process name narrows the field for no technical reason. Where a customer’s quality system requires a specific term in the documentation, the requirement and the label can both appear, with the requirement carrying the technical weight. The engineering context for metal printing as a production route is summarised on the ASME additive manufacturing topic page.
What should be asked before awarding a metal AM job?
Six questions that decide whether the part will fit.
Ask about powder management, layer thickness, orientation and support plan, heat treatment, which faces are machined, and what inspection documentation is included, then compare quotes against those answers.
The first three questions determine the part’s as-built condition. Powder management affects density and repeatability; layer thickness affects finish and detail; orientation and supports determine distortion and which surfaces carry scars. A supplier that answers these concretely is describing a plan rather than a capability.
The last three determine whether the part is usable when it arrives. Heat treatment is required for dimensional stability; the machining plan converts a near-net shape into a functional component; and inspection documentation ties the result to the requirement. Where a part serves a regulated application, the evaluation extends to material, process and cleaning together, which is the framework described in the FDA guidance on technical considerations for additive manufactured medical devices. Independent verification, where needed, is offered by bodies such as UL.
Answering the acronym question
DMLS and SLM describe the same family of machines, and the differences that affect a part come from parameters and planning rather than from the name. Layer thickness trades build time against surface quality. Orientation and support strategy decide distortion and where the scars appear. Alloy choice and powder management decide density and repeatability. Machining and heat treatment decide whether the near-net shape becomes a functional component.
That is why the productive version of this comparison is not a definition but a specification. Write the part’s requirements into the drawing, ask each supplier for the plan that meets them, and compare the plans. The acronyms can then be left where they belong, in the marketing material, while the decisions that matter stay visible.
FAQ
Are SLM and LPBF the same thing?
Laser powder bed fusion is the umbrella term used in standards for processes that melt metal powder layer by layer with a laser. SLM is one of the commercial names for that family, alongside DMLS and other supplier-specific labels. If a drawing or a customer’s specification uses LPBF, a supplier running what they call SLM is describing the same process, and the useful conversation is about parameters rather than names.
How much does DMLS cost?
Cost is driven by build time, support volume, alloy and post-processing rather than by the process name. A short part with little support in stainless costs less than a tall part with dense supports in a nickel alloy, and the finishing operations, including heat treatment and interface machining, are usually quoted separately. Asking for the operations to be listed makes two quotes comparable and shows where a design change would reduce cost.
Which process gives the better surface finish?
Layer thickness and orientation matter more than the machine label. Thinner layers reduce visible stepping and improve detail at the cost of build time, while the same part built at a different angle will show different surface quality on the same faces. Where a face has a finish requirement, the reliable answer is to machine it: the operation reaches a defined finish and leaves a predictable allowance.
Can the same part be quoted by two suppliers using different terminology?
Yes, and the comparison becomes straightforward once the specification is written around requirements rather than process names. State the alloy, the faces to be machined with their callouts, the required heat treatment and the inspection documentation, then compare what each supplier proposes. Differences in the answers, not in the vocabulary, show which quote actually delivers the part you need.
If two metal AM quotes use different process names, send the model and the requirement rather than the label. 6CProto reviews the geometry for laser powder bed fusion, plans orientation, supports and machining allowance, and returns a DFM report with the quote. Upload the file at the 6CProto quote page or send it to projects@6cproto.com.