

A machined part is rarely finished when it comes off the machine. The steps that turn a cut blank into a part you can install, plate or ship are secondary operations, and the order in which they run decides whether those steps cost a little or a great deal.
Which operations count as secondary
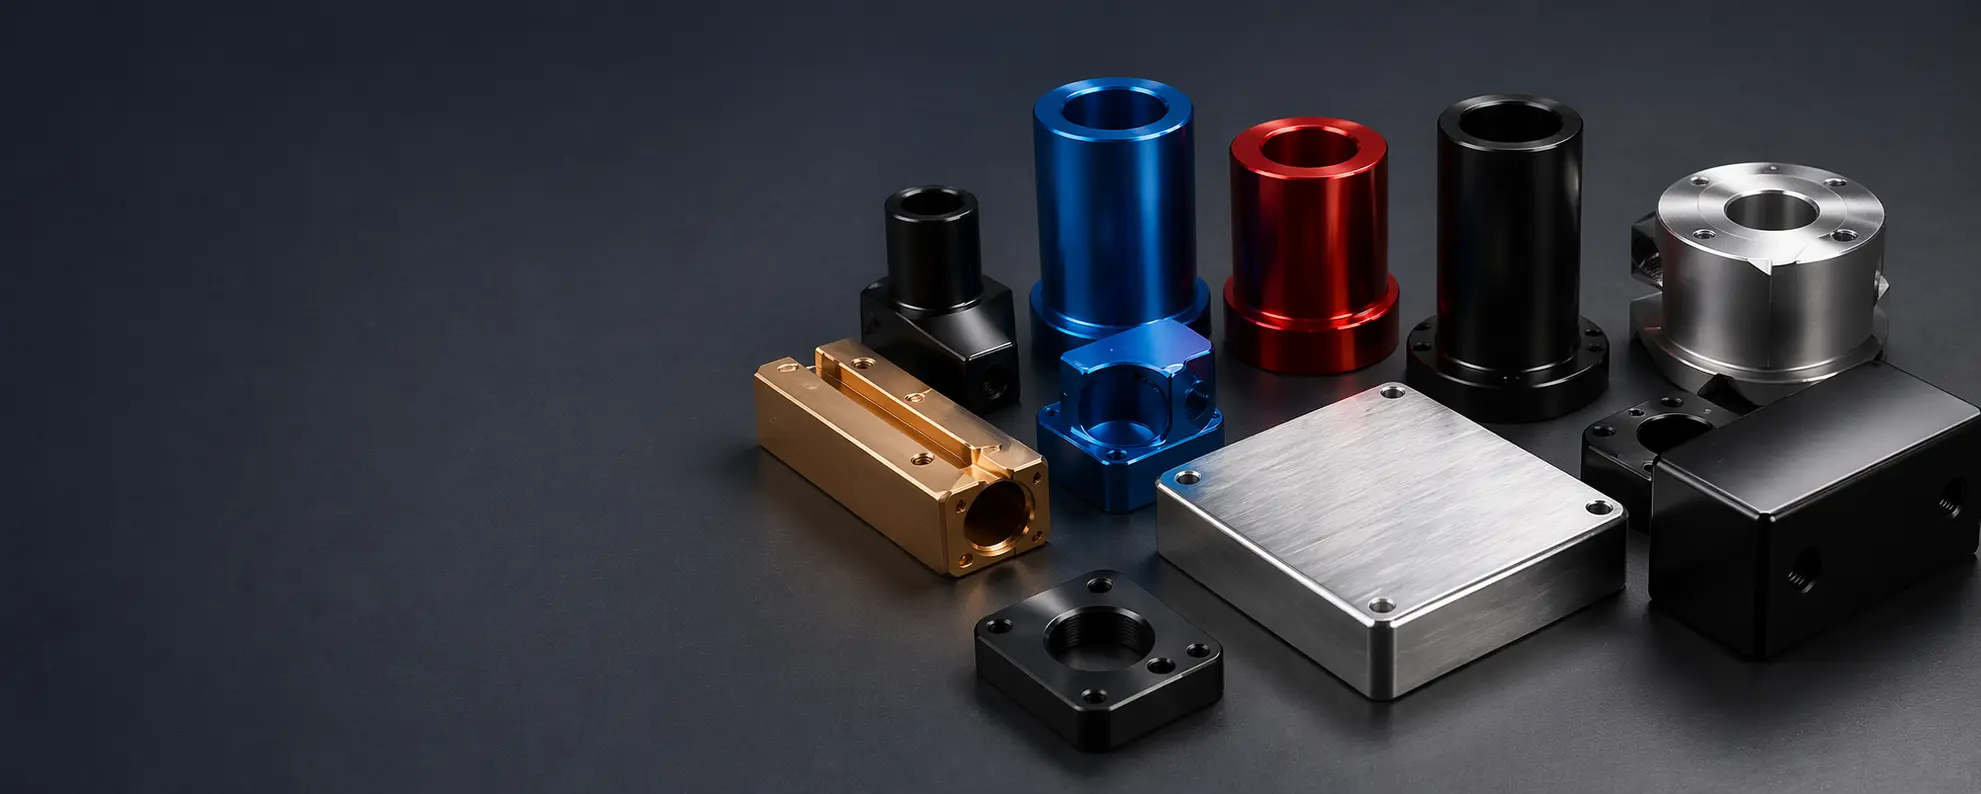
Any operation performed after the primary cut that does not remove the part’s defining geometry counts as secondary. In practice that covers deburring and edge breaking, tapping or thread milling performed off the main cycle, chamfering, surface finishing such as anodizing, plating or bead blasting, laser marking and engraving, cleaning, and final inspection. Pressing a bushing or a bearing into a finished bore is also secondary, even though it changes the assembly.
The list matters for quoting because each entry adds handling. Handling is charged per part regardless of how short the operation is, so five small secondary steps cost more than one step that does the same work in a single pass. This is the reason a part with a generous deburring note and no cosmetic requirement is often cheaper than an identical part with three finish callouts.
Why secondary operations should be planned before the first cut
Because they change the part the machine has to produce.
If a bore will be plated, the machined bore must be smaller by the coating thickness; if a face will be bead blasted after a sealing surface is cut, the mask has to be planned; if a thread will be rolled rather than cut, the blank diameter is different. Deciding the finishing route after machining forces the operation to compensate for a part that already exists, which is slower and less reliable than designing for it.
Sequence also affects geometry. Heat treatment between operations can move a part slightly, so a finishing cut may be needed after it rather than before. Plating and anodizing add material on external surfaces only, and a tight diameter needs to state whether the limit applies before or after the coating. Where a dimension is critical, the safest instruction names the condition at which it is measured.
Deburring, edge treatment and the parts nobody measures
Deburring is the most underestimated secondary operation. A burr left on a cross-hole or a thread entry is a handling injury, a particle source and, in a moving assembly, a wear point. Deciding the edge treatment on the drawing — a chamfer, a radius, or simply a note that edges must be free of burrs — removes a judgement the operator would otherwise make alone.
Where a part has many intersecting edges, hand deburring becomes a significant time line and is difficult to control consistently. A drawing that allows a small radius where it does not interfere with function lets the machine leave the edge in a controlled way, which is faster and more repeatable than finishing each edge by hand after the batch.
| Secondary step | Why it is scheduled | What to specify |
|---|---|---|
| Deburring and edge breaking | Safety, cleanliness, fit | Where a radius is permitted; where a sharp edge is required |
| Anodizing or plating | Corrosion, wear, appearance | Thickness or class; whether limits apply before or after coating |
| Bead blasting | Uniform matte appearance | Faces to mask; whether threads and bores are protected |
| Marking and engraving | Traceability, branding | Content, depth and a location clear of sealing surfaces |
| Cleaning and packing | Particle control, transit protection | Cleanliness level and how parts are separated |
How secondary operations change the quotation
In a well-structured quote, secondary operations appear as their own lines rather than folded into the machining rate. That is what makes them negotiable: a buyer can see that removing a cosmetic callout on an internal face saves a handling step, while keeping the finish on the visible surface protects the part that matters. Where they are hidden inside a single rate, the same decision is invisible.
Cost also depends on batch size for the same reason as machining. Setup-heavy steps such as masking for blasting or fixturing for laser marking are charged once, so the per-part cost of finishing falls as quantity rises, while purely per-part steps such as hand deburring do not. Knowing which category each step falls into tells you where a quantity increase will actually help.
Two standards are useful when specifying these steps. Coating and surface-condition terminology follows ASTM Committee B08, and the environmental obligations that apply to plating, blasting and cleaning lines are published by the US EPA. Machining and inspection terminology follows ASME and the NIST Manufacturing Extension Partnership.
Sequencing secondary operations across a batch
How the steps are ordered through a batch matters as much as which steps are chosen. Deburring before inspection prevents a burr being recorded as an out-of-tolerance edge. Threads are formed or cut before coating, and masked if the coating would otherwise close them. Marking goes on a finished surface only when the mark is deep enough to survive blasting. Getting the order wrong means repeating a step, and repeating a step means re-inspecting everything it touches.
The order also decides who owns the risk. If a part is plated before a final dimensional check, the plater owns the coating thickness and the machinist owns the pre-plate geometry, and a mismatch has to be resolved after the fact. Agreeing the sequence inside the order removes that ambiguity, which is why a quotation that lists secondary operations separately is easier to manage than one that hides them in a single rate. Process-safety requirements for plating and blasting lines are published by the US EPA, and surface-condition classifications by ASTM Committee B08.
Include your deburring and finish requirements in the drawing and request a quote so 6CProto can price the secondary operations as separate lines.
FAQ
Are secondary operations always more expensive than doing the work in the main cycle?
Not always. A deburring pass that runs as part of the machining cycle is cheaper than hand finishing after the batch, which is why a drawing that permits a controlled edge radius often reduces cost rather than adding it.
Does anodizing or plating change the part dimensions?
Yes. Coating adds material on the surfaces it reaches, so a bore that must stay within a limit is machined smaller deliberately. A drawing should state whether a dimensional limit applies before or after coating so the measurement condition is unambiguous.
Can threads and bores be protected during blasting or coating?
They can, by masking before the operation, but masking is a handled step with its own cost. The cheaper route is usually to design the part so the surfaces needing protection are not exposed to the process in the first place.