

Explore Sheet Metal Design, Materials & Assemblies
Aerospace sheet-metal work is a documentation game as much as a manufacturing one. A bracket, shroud, or lightweight structure must be strong and light, and—critically—proven: the alloy traceable, every inspection recorded, the process repeatable. Before a single flange is bent, the material certificate, the inspection plan, and the process records are written into the RFQ, because an aerospace part without its evidence is not an aerospace part, no matter how well it was made.
What Counts as an Aerospace Sheet Metal Part
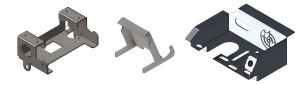
The parts that send engineers to sheet metal are functional and structural: brackets that mount components, shrouds that protect and route cables and ducts, lightweight panels and covers, and formed structures that carry load. They are fabricated from sheet, formed to shape, and assembled with fasteners or welding. They share a profile—thin, light, precisely formed, and full of the holes and features that mounting requires.
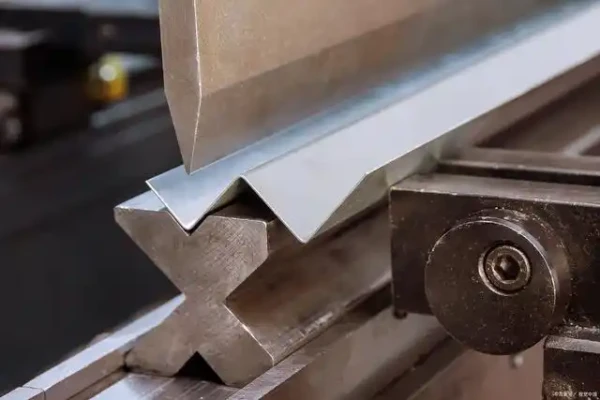
Brackets in aerospace tend to be thin-walled, formed, and hole-heavy. The web carries the load, the flanges stiffen it, and the holes mount or route through it. The same geometry that works on a bench can distort in the press brake if the order of forming and cutting is not considered: punching a hole pattern first and then bending across the hole row can pull the web, while forming first and punching second lets the bend radii control the hole positions. For a one-off prototype this is an annoyance; for a flight-adjacent part it is a nonconformance.
Shrouds and covers are the other common family: larger, more lightly loaded, and appearance-conscious. Their job is protection and routing, which makes edge condition, fastener spacing, and vibration behavior more important than raw strength. A shroud that rattles in service is a quality complaint even though it never fractures. The fabrication drawing for these parts should separate functional callouts from cosmetic ones: a bracket needs its hole positions and bend angles controlled; a cover needs its edge radii and fastener pattern controlled. Mixing the two on one tolerance block either over-prices the part or under-specifies the critical features.
Materials for Flight Structures
Material selection for aerospace sheet metal is a strength-to-weight and environmental-resistance decision, and it drives fabrication: each alloy forms, springs back, and welds differently, and the process must match. Aluminum dominates because it delivers the strength-to-weight balance with predictable forming behavior. 5052-class alloys bend and form well and resist corrosion in most interior environments; 6061-class alloys offer higher strength for brackets and fittings. The choice is a forming-versus-strength trade, not a simple preference.
Titanium appears where temperature, corrosion, or weight-saving efficiency forces it. It is stiffer per unit weight and survives higher service temperatures, but it springs back more, wears tooling faster, and needs slower forming. Stainless serves specific environments—corrosion-critical or high-temperature locations where aluminum behavior is insufficient. The alloy and temper should be locked on the drawing before quoting: when a shop quotes a part on 5052 and receives a drawing that calls 6061, the bend radii, springback, and edge condition all change, and the certificate follows the delivered stock. For fabrication questions around bend radii and formed feature limits, the sheet-metal design limits guide and the sheet metal tolerances post cover the practical window.
Lightweighting Without Losing Stiffness
Lightweighting is the aerospace design discipline: remove material where the load allows, keep it where the stiffness is needed. Sheet metal serves this with formed sections—flanges, ribs, and stiffened panels—that add stiffness without adding thickness. The engineering practice is to design the formed features for the load path, then verify the result with analysis or a prototype. A part that is simply thin is not lightweight; a part whose stiffness is designed into its sections is.
Three constraints should shape every lightweighting review:
- Place features on the load path. A small formed rib or a 90-degree flange adds far more bending stiffness than a modest gauge increase, at a fraction of the weight. The design review should look for flat zones that could carry a rib instead of simply thickening the sheet.
- Remove material only from stress-free zones. A lightening hole in a web reduces weight but can also remove the material that stabilizes the flange. The hole should sit inside the neutral load path while the flanges, ribs, and fastener zones keep their section.
- Design for vibration, not just static load. A light panel with an unfavorable natural frequency can fail from resonance where a heavier panel would not. Mass placement, fastener spacing, and edge restraint are part of the vibration design, and the prototype should be checked in the assembled condition, not as a loose panel.
Lightweight features carry their own tolerances, and the assembly fits that depend on them must be verified. Specify the tolerances together with the lightweighting itself—a thin web that is not held to its thickness callout changes the stiffness that the rib pattern was designed around.
Tolerances and Inspection Requirements
Aerospace tolerances are controlled and documented. The critical dimensions—mounting features, formed angles, and assembly interfaces—are called out on the drawing and verified at inspection, and the inspection records accompany the part. The practical scope is set in the RFQ: which dimensions, which reports, and what traceability. Sheet-metal tolerances differ by feature type, and the drawing should say so: hole positions can be held tighter than formed feature positions, because punching and drilling are more repeatable than bending. A single blanket tolerance that ignores this distinction either costs money or invites arguments at inspection, because the supplier cannot know which features carry the program risk and will hold every feature to the tightest practical value.
The inspection method should match the feature. Calipers verify a hole diameter, a coordinate check verifies hole positions, and a protractor or fixture verifies a bend angle. The supplier should confirm the method at quoting so the buyer knows what the report will prove. The RFQ that names the method produces an inspection report that answers the right questions, and the measurement practice follows the same discipline that NIST documents for metrology and measurement uncertainty.
First-article evidence is the practical gate for a new aerospace sheet-metal part. The first article confirms the tooling, the material, and the forming sequence together; approving it in writing before the batch runs protects both sides. The retained first article is also the reference for future reorders. For teams coming from machined parts, the precision machining services page explains an equivalent first-article and dimensional record discipline that carries over to formed hardware.
Prototype to Low Volume, With the Paperwork
Aerospace programs validate before they commit. The parts that get flown or delivered to a customer are the product of a chain that started with a prototype that was tested, measured, and signed off. A prototype that passes a fit check tells the team the geometry is right; a prototype that passes with full documentation tells the team the process is right, which is the evidence the next stage needs. Rushing through a lightweight prototype may save a week and cost a month later when the production order cannot reproduce the geometry.
Aerospace programs validate before they commit. The prototype bracket or shroud is produced, tested, and documented; the low-volume run follows with the process controlled and the records complete. Sheet metal fabrication serves both stages without tooling barriers, because the press brake, punch, and laser cutter need no hard tooling to change between runs.
The transition rule is to keep the geometry and the documentation standard stable from prototype to production. The part that validates as a prototype is the part that produces as a batch—and the risk sits in the documentation standard. A prototype accepted with a one-page note may not satisfy a production part’s record requirement. Specify the final documentation level from the start and let the early stages approach it, so the batch is not blocked by paperwork created after the fact. The documentation scope is negotiable, but only before the order: a research prototype may accept a reduced set, while a flight-adjacent part usually needs the full chain of material certificates, inspection records, and process records.
Frequently Asked Questions
Which sheet metal parts appear in aerospace?
Brackets, shrouds, panels and covers, and formed structures that mount and protect components—thin, light, precisely formed, and documented.
Which materials are used for flight structures?
Aluminum alloys as the workhorse, titanium where temperature or corrosion demands it, and stainless in specific environments. The selection follows the loads and conditions, and the alloy and temper are locked on the drawing before quoting.
How is lightweighting done in sheet metal?
With formed sections—flanges, ribs, and stiffened panels—that add stiffness without adding thickness, placed on the load path and verified for vibration behavior in the assembled condition.
What documentation accompanies aerospace parts?
Material certificates, inspection records, and process records, with the scope defined in the RFQ. For prototyping and low-volume runs, 6CProto’s sheet metal fabrication service and the aerospace industry page describe how that evidence chain is planned before the first part is made.