Inconel is engineered to keep its strength when everything around it has softened, and that is exactly what makes it difficult to cut. The alloy resists heat, and machining generates heat, so the two fight each other at the tool edge.
Why the alloy is hard to machine
Nickel-based superalloys retain strength at temperatures where steel has already lost most of it. Cutting forces stay high, the chip does not soften enough to break cleanly, and the heat generated by cutting stays near the edge because the material conducts it away slowly. The combination produces high tool temperatures, rapid edge wear and a tendency for the workpiece surface to work-harden if the tool rubs rather than cuts.
| Property | Effect during machining | Practical response |
|---|---|---|
| High-temperature strength | High cutting forces and difficult chip formation | Rigid setup, positive feed, no dwelling |
| Low thermal conductivity | Heat stays at the cutting edge | Lower surface speed, high coolant volume |
| Work hardening | A rubbing pass creates a hard skin | Engage the tool fully; avoid skimming cuts |
| Abrasive carbides | Accelerated flank wear | Wear-resistant tool grades; frequent edge changes |
| Gummy chip behaviour | Chips weld and re-cut | High-pressure coolant and chip control |
Tooling and parameters that survive
The practical strategy is to cut slower than feels natural and to keep the tool fully engaged. Surface speeds low enough to limit edge temperature, a positive feed per tooth that keeps the cutter biting rather than rubbing, and a depth of cut that clears the work-hardened layer from the previous pass are the three levers that matter most. Coatings and grades designed for high-temperature alloys make a measurable difference, but the parameters matter more than the tool.
Cooling is not optional. High-pressure coolant directed at the edge removes heat and clears chips that would otherwise be re-cut and work-harden the surface. Rigidity is the second requirement: the cutting forces are high, so short tool overhang, firm workholding and a machine in good condition all contribute more than any single parameter choice.
What the disadvantages of Inconel are
Cost, machinability and the difficulty of repair.
Four disadvantages come with the alloy. Material cost is high, and because it is difficult to cut, the machined cost is high as well. Tool life is short, so consumable cost is a visible part of any quotation. Machining is slow, which limits how much can be produced on a given machine. And the material’s tendency to work-harden means that a mistake is not easily recovered by taking a light cleanup pass, because the cleanup pass itself hardens the surface further.
A fifth consideration applies in service rather than in the machine. Inconel is difficult to weld and to rework, so a component that needs field repair is often replaced rather than restored. That is a design consequence rather than a machining one, but it belongs in the decision about whether the alloy is appropriate for the part.
Is Inconel harder than steel?
In cutting terms, yes, by a wide margin.
In terms of resistance to cutting, yes, considerably. Inconel retains its strength at temperatures where alloy steel has softened, and it work-hardens more aggressively, so the same tool and parameters that cut steel comfortably will fail quickly in Inconel. Hardness measured at room temperature is not the whole story: the difficulty comes from hot strength and from how the material responds to the cutting process, not only from how hard it is when cold.
The practical consequence is that Inconel is specified when service conditions demand it rather than when a part is merely strong. Where a part needs high strength at moderate temperature, a suitable alloy steel or a precipitation-hardening stainless steel is easier to machine and cheaper to produce, and the design should start there before moving to a superalloy.
Machinability of Inconel 718 in practice
718 is the most widely used of the family because it combines high strength with reasonable weldability for a superalloy, and it is the grade most often encountered in aerospace and energy work. Its machinability is poor relative to steel but it is well documented: the parameters are known, the tooling exists, and a shop that regularly processes the alloy will produce consistent parts. The risk lies with shops that treat it as a difficult steel, because the consequences of an incorrect parameter set appear quickly.
Two questions sort suppliers effectively. Do they machine 718 regularly, and what tool life do they achieve on a comparable part? A shop with a measured answer has a process; one that answers in general terms is likely to learn at the customer’s expense. Material and alloy data is published by ASM International, and measurement practice is described by the NIST Manufacturing Extension Partnership.
Designing for manufacturability in a superalloy
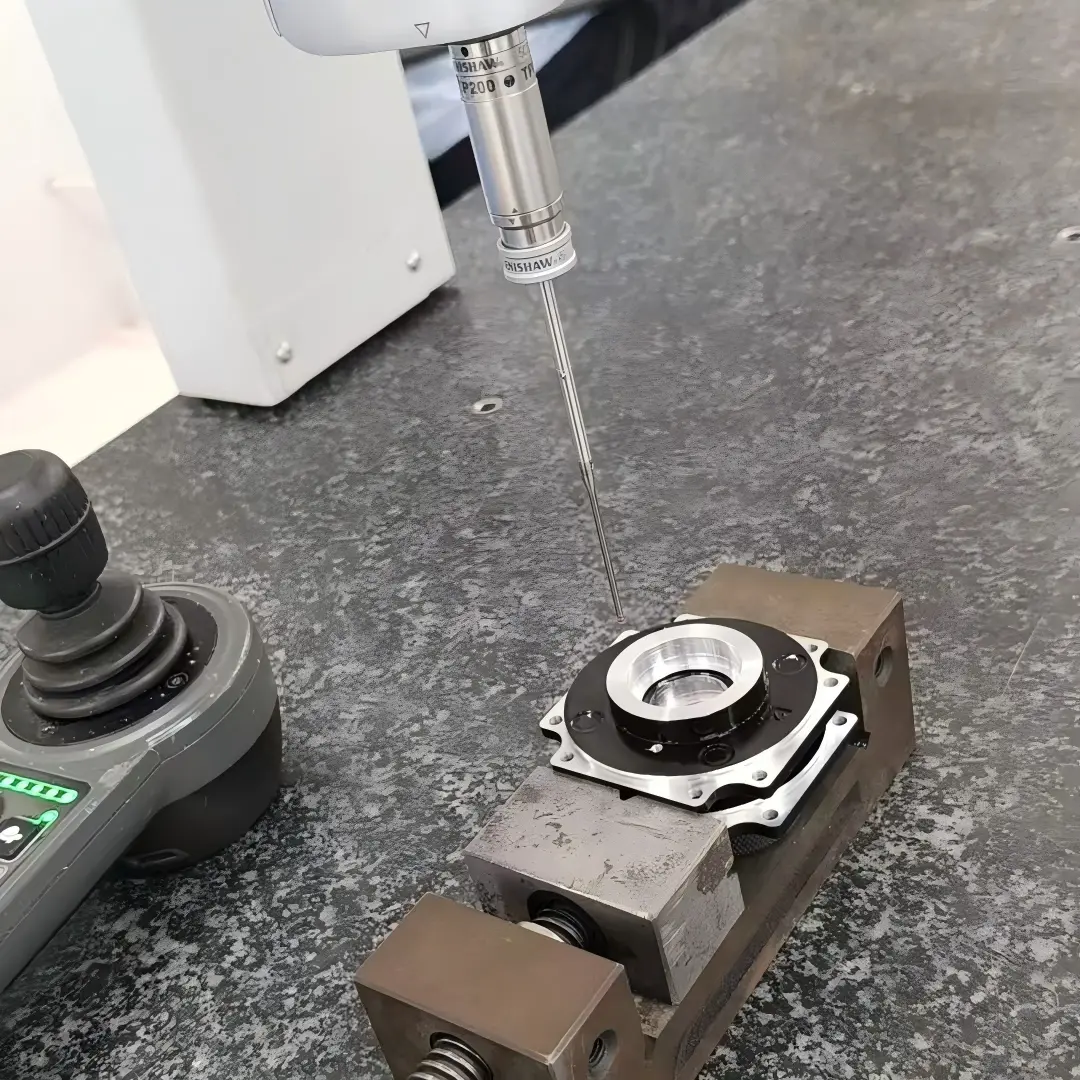
Design choices have a larger effect on cost here than in ordinary materials. Keep features accessible so that long, slender tools are not required, because tool deflection in a high-force cut produces chatter and premature failure. Radius internal corners, since sharp transitions concentrate stress in service and force a smaller cutter in machining. Avoid thin walls, which deflect and chatter under the cutting loads this alloy generates. And minimise the number of separately toleranced dimensions, because inspection in a slow process adds directly to the lead time.
Two specification notes reduce risk. State the exact grade and condition, since the family spans several alloys with different behaviour, and state the service temperature the part must survive, because that is what justifies the material choice in the first place. Drawing conventions follow ASME standards, and surface and coating terminology follows ASTM Committee B08. Machining fluid and swarf obligations for these alloys are set out by the US EPA. Process options are described under CNC machining.
Send the part with the grade, the service temperature and the critical fits, and request an Inconel machining quote with the tooling approach stated.
FAQ
What are the disadvantages of using Inconel?
High material cost, high machining cost because tool life is short and cutting speeds are low, slow production that limits throughput, and limited recovery from mistakes because light cleanup passes work-harden the surface further. Repair in service is also difficult.
Is Inconel harder than steel?
In terms of resistance to cutting, yes. It retains strength at temperatures where alloy steel has softened and work-hardens more aggressively, so parameters that cut steel comfortably will fail quickly. Room-temperature hardness alone does not explain the difficulty.
What is the machinability of Inconel 718?
Poor relative to steel but well documented, which means a shop that machines it regularly can produce consistent parts with known parameters and tool life. The risk lies with shops treating it as a difficult steel rather than as a superalloy.