A drawing that specifies 17-4 PH stainless steel is incomplete, because the alloy’s properties depend on the condition it is supplied in. The H designation that follows the alloy name is not decoration; it is the heat treatment that determines how the part behaves.
What 17-4 PH is
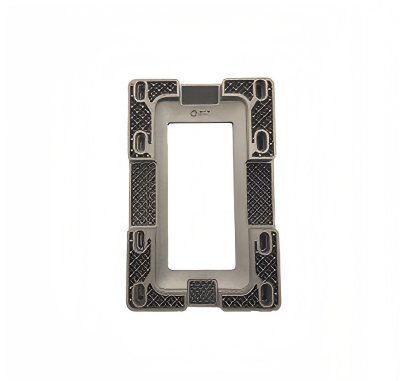
17-4 PH is a precipitation-hardening martensitic stainless steel, alloyed with copper so that a controlled heat treatment precipitates fine particles within the matrix and raises strength. It combines corrosion resistance comparable to common stainless grades with strength approaching that of alloy steels, which is why it appears in aerospace fittings, valve components, shafts, fasteners and medical instruments.
| Characteristic | What it means for a machined part |
|---|---|
| Precipitation hardening | Strength comes from a heat treatment applied after machining |
| Corrosion resistance | Better than many alloy steels; less than the austenitic stainless grades |
| Machinability | Machines well in the annealed or solution-treated condition |
| Distortion | Slight dimensional movement during aging; allowance may be needed |
| Condition dependence | Strength and hardness follow the aging treatment, not the alloy alone |
What H900 designates
The aging temperature, expressed in degrees Fahrenheit.
The H designation in a 17-4 PH specification refers to the temperature at which the material is aged after solution treatment, so H900 means aged at 900 F and H1150 means aged at 1150 F. Because the precipitate that provides strength forms differently at each temperature, the higher the aging temperature, the lower the resulting strength and hardness but the greater the toughness and ductility. The designation therefore tells a supplier which properties to deliver rather than simply which alloy to use.
Two practical consequences follow. H900 gives the highest strength and hardness within the common range of conditions, which is why it appears on highly loaded parts, while the over-aged conditions such as H1150 are chosen where toughness or resistance to stress corrosion cracking matters more than peak strength. And because the designation is part of the specification, a part quoted as “17-4 PH” without a condition should be queried rather than accepted.
How the part is brought to the H900 condition
The sequence matters. Material is normally supplied in the solution-treated or annealed condition, which is the state in which it machines most readily. The part is then aged at the specified temperature for a controlled time and cooled, during which the precipitate forms and the strength develops. Where tight tolerances are required, the sequence is often rough machine, age, then finish machine, so the final geometry is produced after the dimensional movement has occurred.
Aging is a controlled thermal process, and the resulting properties are verified from the material certificate and from hardness testing rather than assumed. That is the practical reason a drawing should state the condition: it tells the supplier to age the part and document it, rather than to machine the material as received. Heat treatment terminology and material data are published by ASM International, and inspection practice is described by the NIST Manufacturing Extension Partnership.
How H900 differs from H1150
The difference is a trade between strength and toughness. H900 delivers the highest strength and hardness of the standard conditions, which suits parts that carry high load in a compact section. H1150 is an over-aged condition with lower strength but greater ductility and improved resistance to stress corrosion cracking, which suits parts that must survive a corrosive environment under sustained load.
Choosing between them is a design decision rather than a procurement one. A shaft transmitting high torque in a protected environment may be best in H900; the same shaft in a marine or chloride-bearing environment may last longer in an over-aged condition despite its lower strength, because the failure mode changes from overload to cracking. Stating both the loading and the environment in the enquiry is what allows that trade to be made deliberately.
Machining and distortion
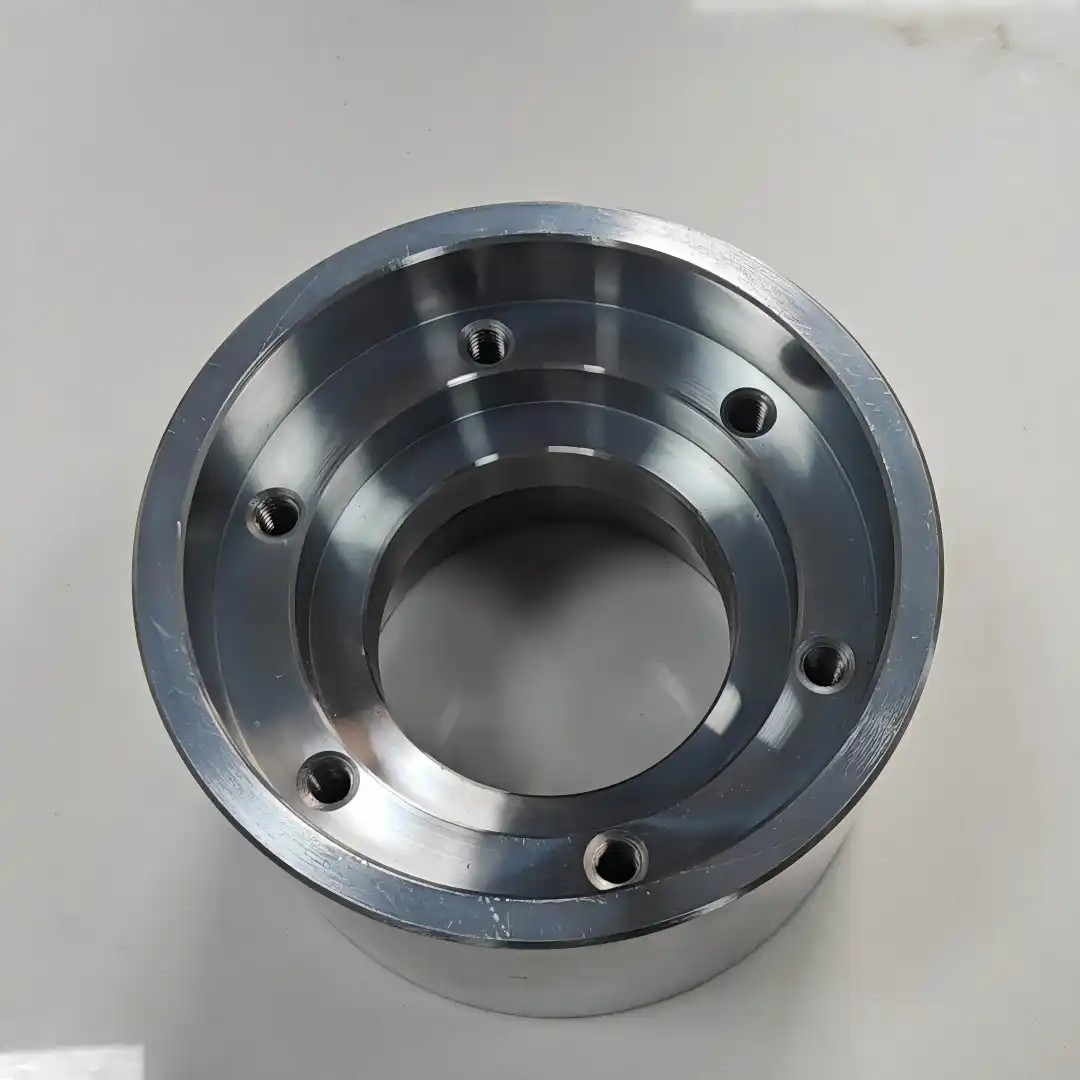
17-4 PH machines well before aging, producing good surface finishes with appropriate tooling and coolant. The difficulty is dimensional: aging can move a part slightly, and thin or asymmetric sections move more than compact ones. The standard approach for tight work is to leave finishing allowance, age the part, and then machine to final size, which places the controlled dimensions after the distortion rather than before it.
Two further points are worth planning. Machining after aging is possible but harder on tooling, since the material is at its strongest, so the sequence should be chosen deliberately rather than left to convenience. And where a part will be welded, the heat input affects the local condition, which means the aging treatment and the weld sequence have to be considered together. Drawing conventions follow ASME standards, and surface and coating terminology follows ASTM Committee B08.
How to specify 17-4 PH correctly
Name the alloy, the condition and the standard it is measured against. State the properties the part must achieve, particularly strength or hardness, so the condition can be verified rather than inferred. Identify the features that must hold tolerance after heat treatment, since those determine whether a finishing operation follows aging. And state the environment and the load, because the choice between H900 and an over-aged condition depends on both.
Two notes prevent disputes. Ask for the material certificate to record the condition actually supplied, since a certificate that names only the alloy does not prove the treatment. And state whether the part will be passivated or coated afterwards, because some surface treatments interact with the alloy’s corrosion behaviour and the sequence matters. Process obligations for heat treatment and finishing are set out by the US EPA, and machining routes are described under CNC machining.
Send the part with the condition, the load and the environment, and request a quote including the heat treatment sequence.
FAQ
What is H900 stainless steel?
It is 17-4 PH precipitation-hardening stainless steel in the condition aged at 900 degrees Fahrenheit, which delivers the highest strength and hardness of the standard conditions. The H designation refers to the aging temperature, not to a separate alloy.
How is 17-4 PH brought to the H900 condition?
The material is solution treated, machined in that condition, then aged at the specified temperature for a controlled time and cooled. Where tolerances are tight, the part is rough machined, aged, and finish machined afterwards so final dimensions follow the distortion.
What is the difference between H900 and H1150?
H900 gives the highest strength and hardness, while H1150 is an over-aged condition with lower strength but better ductility and resistance to stress corrosion cracking. The right choice depends on whether the part is governed by load or by environment.