

Explore 3D Printing Design, Materials & Finishing
Physics Sets the Rules, Not the Software
Printing builds a part layer by layer, and every layer must be supported by the layer below it. That simple fact produces the design constraints: overhangs beyond a certain angle need supports, thin walls may not form, and features that bridge open space droop. The slicer software can warn about violations, but it cannot suspend physics. The design approach is to know the process limits and design within them, then let a printability review catch what the design missed.
Physics also sets the build cost. A part that needs supports, thick walls, or a tall build costs more in material and time, and the design choices are cost choices. Process selection comes first, because the wall limits, overhang angles, and minimum feature sizes belong to the process: a design matched to the intended printer is a design that quotes economically, while a design built for one process may need rework for another.
Overhangs and Support Strategy
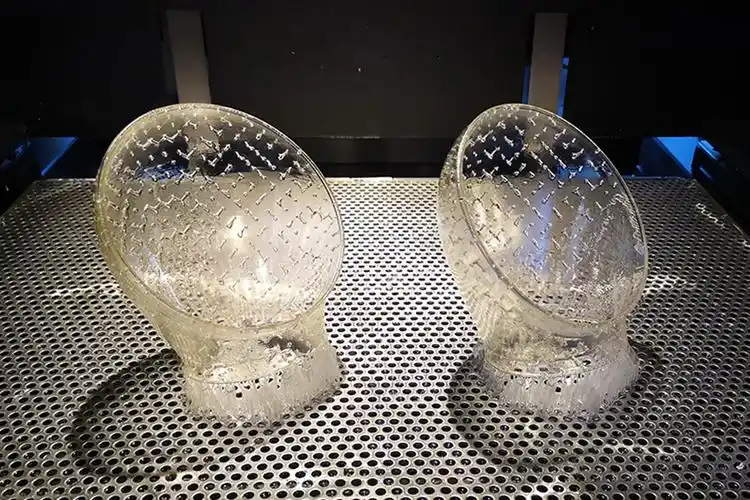
Overhangs are features that extend beyond the layer below them. Small overhangs print acceptably; larger ones need supports, and supports add material, time, and post-processing. The design lever is the angle: keeping overhangs at a conservative self-supporting angle avoids supports entirely. When supports are unavoidable, design for their removal with accessible geometry, clean break points, and surfaces where the support marks are acceptable.
Support surfaces are where the finish suffers. The faces that touch supports carry the marks, so place supports on hidden or non-critical faces and mark the critical surfaces on the drawing before orientation is chosen. Every cubic millimeter of support is material, machine time, and removal labor: a design that minimizes the support volume buys the saving in all three.
Minimum Wall Thickness by Process
Walls below the process minimum do not form reliably. As a reference, the stated minimum wall thicknesses are approximately 0.8 to 1.2 mm for FDM, 0.4 to 0.6 mm for SLA, 0.7 to 1.0 mm for SLS, 0.8 to 1.5 mm for SLM metal, and about 1 mm for MJF. These are starting points, not universal values: the actual minimum depends on the material, the geometry, and the feature, so stay above the minimum with margin, especially for structural walls and tall features. A wall at the minimum prints, but it may be weak or variable, and margin is the cheap insurance.
Wall thickness also interacts with feature height. A tall thin wall prints less reliably than a short one of the same thickness because each layer cures against less support, and cosmetic walls that will carry a surface treatment need extra thickness so the finishing does not break through. If a part is to be machined after printing, the printed wall has to start thick enough to allow the machining pass.
Lattices: When They Pay Off
Lattice structures replace solid material with a strut pattern, and they pay off when weight matters and the process can produce the geometry. The lattice has to respect the process resolution: struts must stay above the process minimum, and the cell size must be printable. A lattice that is too fine fails or fuses together, so the weight saving is only real if the geometry prints. The function of the lattice is the test: a structure that saves weight but fails under the load is a design failure, so test the lattice part against the actual load to confirm the strut size and cell pattern.
Orientation Changes Everything
Part orientation on the build platform decides support needs, surface quality, strength, and cost. Orientation affects which faces touch supports, how the layers align with the load, and how tall the build is, so the same part prints differently in different orientations. Choose orientation with the process: functional faces away from supports, load-bearing features aligned with the layers, and the build kept short.
The layers are the weak planes of a printed part, and a feature loaded across the layers can fail where the same feature loaded along them survives. State the load direction with the design so the orientation can protect the strength, and review the orientation with the supplier before the file is final, because orientation is a joint decision that serves the part only when it is chosen together.
A DFM Checklist Before Upload
Before sending a design for printing, run a short checklist: are overhangs within the self-supporting angle or support-friendly; are wall thicknesses above the process minimum with margin; are unsupported spans and bridges avoided or designed for support; are features oriented to avoid unnecessary supports; are critical fits marked for post-printing machining; and is the design optimized for build height. The checklist catches the common failures before they become failed prints, and it also covers the file itself: units, a solid model, and printability warnings should be verified before upload.
The checklist is also the RFQ input. Send the design with the checklist notes so the supplier reviews the known risks and confirms the process, and feed the printability review results back into the checklist. The loop of design, review, fix, and re-check is how a design converges on the printable.
Choosing the Process and Materials
Wall limits and feature sizes belong to the process, so the final process choice should match the part geometry. The 3D printing service page compares the process range, and the 3D printing materials page lists the resins and metals available at each resolution level. For parts that need tighter fits than the printed surface provides, post-printing machining at precision tolerances is the usual complement, and the process comparison between printing and machining is covered in the 3D printing versus CNC article. Where a printed part must meet a defined test method, the external reference can be found via NIST measurement standards.
The process comparison for specific resins and layer limits is also covered in the FDM versus SLA versus SLS article, which is useful when the part geometry could fit more than one process.
Lattice Design Decisions That Are Easy to Get Wrong
Lattice structures promise weight savings and interesting mechanical behavior, but they fail predictably when the design does not match the process. The first decision is unit cell size: a lattice that looks elegant in CAD may be impossible to print if the strut diameter falls below the machine’s reliable feature size, so the minimum sustainable thickness and the aspect ratio of the cell are process limits, not aesthetic choices. The second is orientation. Struts printed near the build direction carry different strength and surface finish than struts printed at an angle, and the same lattice printed in two orientations behaves differently.
The third is end connections. Every lattice connects to a solid boundary somewhere, and the transition zone, where the struts meet the wall, concentrates stress and often prints poorly because of local overheating or unsupported geometry. The design should add fillets and a small solid transition at the interface instead of bolting the lattice onto the wall with a sharp intersection, and the transition should be reviewed in the same DFM pass as the rest of the part.
Finally, lattices complicate every downstream step. Powder removal becomes harder, surface finishing reaches less, and inspection of interior struts is limited, so the lattice should only appear where the function pays for those costs: compliance, weight, or controlled stiffness. Functional lattices belong on 3D printing services with the process and material specified together, and the FDM vs SLA vs SLS guide helps match the technique to the feature size and surface requirement.
Overhang Rules That Differ by Process
Overhang behavior is not one number because the support strategy differs by process. In FDM, bridging and the layer direction decide what prints unsupported: a bridge along the layer axis can span a modest gap, while a large dome or a steep roof needs supports and the mark they leave. In SLA, the resin and the orientation decide support placement, and supports typically contact the part with small tips that leave blemishes needing post-processing. In SLS or MJF, the powder bed supports the part, so overhangs print without solid supports but the geometry still affects where powder packs and how well the surfaces fuse.
The design response is orientation-aware. Rotating the part so critical faces avoid supports, or so the smallest face carries the support scars, is often cheaper than redesigning the geometry. Chamfers and 45-degree transitions turn an unsupported ledge into a self-supporting slope, and a concave fillet at the base behaves better than a sharp transition. The DFM review should look at the part as the machine will see it, with the build direction stated, not as an abstract solid.
When in doubt, test the worst feature rather than the whole part. A small test coupon with the overhang angle, the wall thickness, and the smallest feature prints faster than a full prototype, and it answers the real question: what does this process produce at this size and angle. Coupons are especially useful when moving a design between 3D printing technologies, because the rules that were safe in one process are not automatically safe in the next.
FAQs
What angle can print without supports?
It depends on the process, but keeping overhangs at a conservative self-supporting angle avoids supports. Features beyond the angle need supports, which add cost and post-processing.
What is the minimum wall thickness for 3D printing?
As a reference, about 0.4 to 0.6 mm for SLA, 0.7 to 1.0 mm for SLS, 0.8 to 1.2 mm for FDM, 0.8 to 1.5 mm for metal, and about 1 mm for MJF, with margin recommended for structural features.
Are lattice structures worth the design effort?
When weight matters and the process can produce the strut geometry, yes. Below the process resolution lattices fail, so use them where the saving justifies the effort and the structure has been tested against the load.
Does orientation affect print quality?
Significantly. Orientation decides support marks, surface quality, build cost, and the direction of the layer lines that carry the load, so it should be chosen with the process rather than left to chance.