

Explore CNC Design & Material Selection
The Material Is the Largest Variable in Milling
The material is the largest variable in CNC milling. Aluminum mills fast with fine finishes, steel and stainless need controlled parameters, titanium and nickel alloys are slow and hard on tooling, and plastics need sharp tools and light cuts. The material choice drives the cycle time, the tool cost, and the tolerance, and the grade matters more than the family name. This guide maps the milling material families, their machining behavior, and the selection logic that matches the material to the part’s service.
The Material Families and Their Machining Behavior
Milling cuts the full range of machinable materials, and each family has a defined behavior on the machine. Aluminum is fast, clean, and forgiving with fine finishes, which suits brackets, housings, and enclosures. Mild steel machines well with good tool life and suits frames, brackets, and production parts. Stainless steel work-hardens at the cut, so it needs sharp tools and a rigid setup, and suits corrosion-resistant parts. Titanium is slow, hot, and hard on tools, which suits aerospace and medical parts. Nickel alloys are slow and tough with real tool wear, for high-temperature parts. Brass and copper machine excellent and clean for electrical and valve parts. Engineering plastics need sharp tools and light cuts for insulators and wear parts.
The table is a tendency guide. The exact grade, 6061 versus 7075 aluminum, 303 versus 316 stainless, or filled versus unfilled plastic, changes the machining behavior more than the family name, so the grade belongs on the drawing.
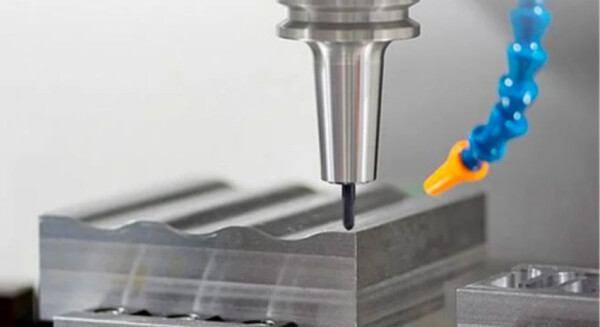
Aluminum: The Milling Default
Aluminum is the material that milling economics love. It cuts at high speed with low tool wear, produces fine surfaces, and holds tight tolerances, which keeps the cycle short and the cost low. 6061 is the general-purpose grade, and 7075 earns its premium where strength is the driving requirement. The design rules follow its softness: thin walls deflect less than in plastics but still need support for tight tolerances, and the thermal expansion is higher than steel, so the tolerance scheme should account for the measurement and service temperatures.
Steel and Stainless: Controlled Parameters
Mild steel mills well and is the low-cost route for structural parts that need more strength and stiffness than aluminum. The machining is forgiving with good tool life, and the parts are typically coated or painted for corrosion protection. Stainless adds corrosion resistance and work-hardens at the cut, so it needs sharp tooling, controlled feeds, and a rigid setup to avoid work-hardening the surface on the previous pass. The grade changes the result: 303 is friendly to tools, while 316 machines gummier and wears them faster. Stainless parts, fittings, medical instruments, and food equipment pay the machining premium for the corrosion behavior.
Titanium and Nickel Alloys: The Difficult End
Titanium and nickel alloys are the difficult end of milling. These alloys push cutting forces high, hold heat at the cutting edge, and consume tooling fast, so the process runs slow with ample coolant and consistent engagement. The cost per part is high, and the design should use the largest practical radii because small tools in these materials remove metal slowly and wear fast. These materials are chosen for the service, not the machining: titanium for strength-to-weight and medical compatibility, and nickel alloys for high-temperature strength. The machining difficulty is the price of the properties.
Tool Life and Cutting Parameters: The Material-Tool Match
The material sets the cutting parameters, and the parameters set the tool life. Aluminum runs high spindle speeds with long tool life; steel and stainless run moderate speeds with predictable wear; titanium and nickel alloys run slow with rapid wear; and plastics need sharp tools and light cuts. The cycle time and the tool cost follow the parameters, which is why the material decision is a cost decision. Tool wear changes the result before it is visible: a dull tool produces a worse surface, drifts from tolerance, and can work-harden the material, so the tool-change interval is part of the process control. The drawing should not expect a tolerance that the tool wear window cannot hold over the production run.
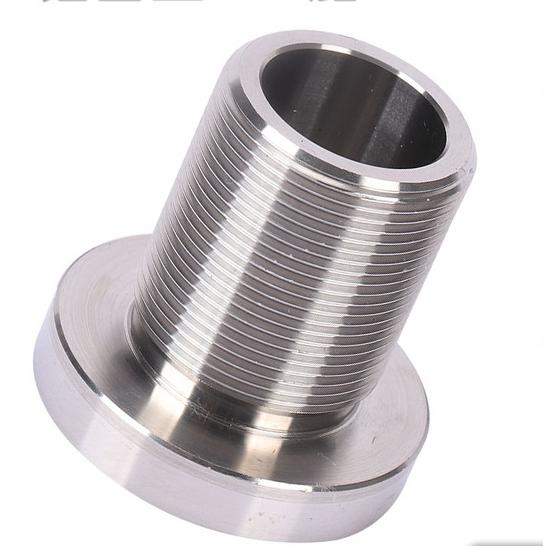
The milling strategy also affects the material behavior. Trochoidal and high-efficiency milling keep the tool engagement constant, which protects the tool edge and manages heat in tough materials, and the strategy is chosen by the material and the feature. The program and the tooling are part of the material story, because the same geometry cuts differently under different strategies.
Brass, Copper, and Plastics: Special Cases
Brass and copper machine with excellent, clean behavior, which makes them the natural choice for electrical and valve parts where conductivity matters. The chips are easy to handle and the finishes hold well, and the main process note is chip control in the machine. Engineering plastics deflect more, soften with heat, and move with moisture and temperature, so they need sharp tools, light cuts, and realistic tolerances. The same geometry that mills easily in aluminum needs different parameters and callouts in nylon or PEEK, and the CNC machining materials page lists the grades the shop can quote.
Read the Drawing as a Machinability Map
The drawing communicates more than the shape; it communicates the machining risk. A deep pocket with a small corner radius is a slow tool path in any material, but in titanium it becomes a tool-failure risk, while in aluminum it is merely a longer cycle. A thread that starts close to a wall, a thin web between bores, and a tolerance on a face that the fixture cannot hold all read differently by material. Send the drawing with the material callout and ask the shop to flag the features that are difficult in that specific grade, because the same geometry that quotes cleanly in 6061 may double the tool budget in 17-4 PH.
Selecting the Material for the Part’s Service
The material-tool match goes beyond the grade to the tool coating and geometry. Aluminum and brass cut cleanly with standard carbide end mills and generous flute geometry for chip evacuation; stainless and titanium benefit from tools with sharper edges and lower helix angles that resist edge breakdown; and nickel alloys often justify coated tooling to extend the interval between changes. The same material can behave differently with a worn tool versus a fresh one, which is why the tool-change schedule is a process parameter rather than a maintenance detail. Ask the supplier how tool life is managed on the material you specify, because the answer predicts the consistency of the surface and the tolerance across the run.
Coolant and chip control complete the picture. Aluminum and copper produce stringy chips that must evacuate cleanly to avoid re-cutting; titanium and nickel trap heat in the tool, so flood coolant and high-pressure delivery matter; and plastics can be degraded by coolant chemistry, which is why some shops run them dry with air. These process choices do not change the drawing, but they set the achievable surface, the burr condition on the edges, and the follow-on deburring effort, so they belong in the supplier conversation rather than in the quote’s small print.
The selection logic starts with the service, not the machine. A bracket that must be light and cost-effective is 6061 aluminum; a frame that needs strength and stiffness at lower material cost is steel; a fitting that must resist corrosion in food or medical service is stainless; a part that must survive high temperature is a nickel alloy; a part that must run hot without softening is titanium. State the load, the environment, the weight requirement, and the quantity, and the material choice follows.
Confirm the grade and its machinability before quoting, and design with the material’s behavior in mind. A free-machining grade that costs more per kilogram can be cheaper per part because the cycle is shorter, and the comparison should be per part at the real quantity, not per kilogram. The CNC milling service page and the CNC machining tolerances guide cover how the material choice interacts with the tolerance scheme. The CNC machining materials page lists the grades the shop can quote.
Conclusion
The milling material choice is a service decision with machining consequences: aluminum for speed and value, steel for strength, stainless for corrosion, titanium and nickel for extreme service, and plastics for their special properties. Confirm the grade and its machinability before quoting, and design with the material’s behavior in mind. A CNC milling partner that matches the material to the part and the machine is the one that delivers the tolerance and the finish the drawing intends. The NIST measurement standards for material grades and general tolerances define the language the drawing and the inspection share.
FAQs
What is the easiest material to CNC mill?
Aluminum is the easiest and most economical: it cuts fast, holds tolerances, and finishes well with low tool wear. Brass and acetal are also excellent millers, while titanium, nickel alloys, and some stainless grades are the difficult end.
Can a CNC mill cut hardened steel?
Yes, with the right tooling and machine: hard milling uses coated carbide or CBN end mills on hardened steel for dies and molds. The process needs rigidity and controlled parameters, and the drawing should use the largest practical radii because small tools in hard material wear fast.
What material should I choose for a milled bracket?
6061 aluminum is the default for light, cost-effective brackets; steel suits higher strength and stiffness at lower material cost; and stainless suits corrosion or food and medical service. The choice follows the load, the environment, and the weight requirement.