

Two bars with the same steel designation can arrive with different hardness, structure and machining behavior. Choosing annealed vs normalized steel therefore requires more than matching chemistry. The condition on the purchase document must support both the machining route and the properties required when the component enters service.
For suitable carbon and low-alloy steels, full annealing and normalizing use different cooling paths after heating. Their outcomes depend on composition, section and the actual cycle. A general expectation that one condition is softer cannot replace grade-specific procurement requirements or a measured acceptance range.
This comparison focuses on condition selection for precision-machined components. It does not prescribe a furnace cycle or treat normalizing as a substitute for hardening and tempering. The important distinction is between incoming stock condition, any intermediate treatment and final delivered condition. Each can be different, provided the drawing and manufacturing sequence make that intentional.
The machining scope should identify when the stock condition matters to cutting and when the final condition matters to function. A material change that shortens machining time is not acceptable if it leaves the delivered component outside its required property or dimensional state.
What changes in annealed vs normalized steel?
Cooling changes structure; grade controls the result.
Compare annealed vs normalized steel within the same grade and section, then connect the specified thermal condition to hardness, machining behavior and final component requirements before substitution approval.
Full annealing commonly uses controlled slow cooling, while normalizing typically involves cooling in air or gas after the appropriate heating stage. Bodycote's normalizing process description identifies grain refinement and more uniform structure as objectives for carbon and low-alloy steels after forming operations. That description is not a universal hardness guarantee.
The cooling rate inside a thick section differs from that at its surface. Composition also changes the transformations that occur. Consequently, two nominally normalized products can require different property expectations when their section or steel differs.
Specify what the selected condition must accomplish. If the purpose is predictable incoming structure before machining, that is a different requirement from achieving a final strength level. Avoid writing a condition name as a proxy for every desired property. The comparison should remain attached to the actual material specification, product form and section represented by the certificate or test specimen.
Evaluate hardness without equating softness with machinability
Softer does not automatically mean easier to machine. Hardness influences cutting forces and wear, but chip control, ductility, microstructure and surface response also matter. A very ductile material can create troublesome chips or a poor finish even when its bulk hardness is low.
Use grade-specific data and a representative machining trial when the condition change is consequential. Bodycote's annealing description identifies softening and improved ductility as process objectives; it does not establish a universal cutting-speed advantage. A machinability decision should consider the actual tool, feature and production requirement rather than turn that general objective into a numerical cycle-time promise.
For a long slender component, residual stress and stock removal balance may be as important as tool wear. For a small threaded feature, burr behavior and surface integrity may dominate. The route used in milling a functional feature should therefore be evaluated using the geometry that drives acceptance.
Separate trial observations from released limits. A shorter cycle on one bar is evidence about that trial, not proof that all normalized stock will machine faster or that all annealed stock will give a better surface. Keep stock identification with the result.
Purchase and identify the incoming stock condition
Incoming condition belongs on the material order, not only in a shop instruction. Identify the grade, product form, section, delivery condition and applicable material specification. Where a hardness range or other property is essential, state it with its test basis instead of assuming that a condition word supplies the limit.
Check whether the stock has already experienced cold work, straightening, forging or another thermal operation. Those histories can affect the starting structure and residual stress. A bar described only as steel of the correct chemistry may leave the machining team to infer a condition that was never purchased.
TWI's annealing guide distinguishes several mechanisms and purposes covered by the term annealing. That breadth is exactly why a purchase order should not use the word without the required material state. Full, subcritical and other annealing treatments should not be treated as interchangeable labels.
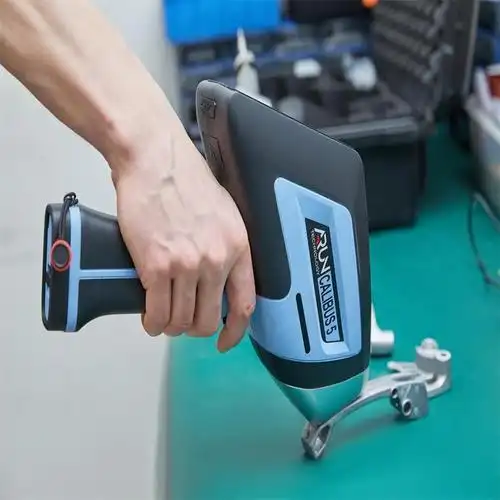
Before cutting expensive features, compare the incoming records with the released requirements. If the certificate lacks a relevant condition or property, resolve the discrepancy before assuming that appearance, spark behavior or a quick file test can supply the missing evidence. Preserve stock-to-part traceability where the application requires it.
Verify the final material state and dimensions
Final-state acceptance should answer two questions: what treatment or supplied condition is documented, and what properties or geometry have actually been checked. A treatment certificate records a process or condition; a hardness result records a measurement at a stated location. Neither independently proves every aspect of the component’s structure and performance.
Match evidence to the requirement. If hardness is controlled, define the method, location and acceptable range. If microstructure is critical, agree the examination and sampling basis. If dimensional stability matters, measure after the last operation capable of changing the part. A pre-treatment dimensional report cannot establish final straightness.
TWI's heat-treatment support description treats mechanical testing, metallurgical examination and process assessment as distinct activities. Use the same distinction in a procurement package: require the evidence needed for the function, without claiming that one convenient result covers all of it.
The inspection agreement should say whether acceptance applies to the stock, a representative coupon or the finished part. Sampling must remain linked to the lot and relevant section. An undocumented coupon from another heat is not equivalent evidence merely because its nominal grade matches.
Compare steel conditions within a grade-specific boundary
The comparison below uses qualitative process information rather than unsupported hardness numbers. Actual ranges belong to the chosen grade and product specification. Keeping the comparison within that boundary avoids a misleading table that assigns one hardness to all steel.
| Material and condition | Typical objective | What remains grade-dependent | Release evidence |
|---|---|---|---|
| Suitable carbon steel, full annealed | Softening and ductility | Resulting structure, hardness and machining response | Specified delivery condition and applicable tests |
| Suitable carbon steel, normalized | More uniform, refined structure after prior processing | Transformation through the section and final properties | Grade, section and condition documentation |
| Low-alloy steel, normalized | Conditioning structure for the defined route | Cooling response and whether further treatment is required | Material-specific specification |
| Quenched and tempered steel | A separately defined hardened and tempered state | Compatibility with any later thermal exposure | Final property and process requirements |
Bodycote's annealing and normalizing overview supports the distinction between these treatment objectives. The final row is included to prevent a category mistake: an existing hardened-and-tempered requirement cannot be replaced by normalized stock solely because machining becomes convenient. Substitution approval must address the component’s functional property requirements as well as manufacturing behavior.
Investigate a proposed normalized-stock substitution
Assume a hypothetical steel bracket is purchased in the annealed condition, rough machined, then inspected for a mounting-bore relationship. A supplier proposes normalized stock to improve consistency after prior forming. No strength, hardness or price values are assumed in this example.
First compare the released material specification and required final state. If the drawing requires only a named grade but the design relies on a particular property, that omission must be resolved before evaluating the substitution. Next compare certificates for the actual candidate stock, including section and condition.
Prepare representative coupons or parts using the same machining sequence. Record chip behavior, tool condition, burrs and dimensional movement after each significant stock-removal stage. Measure the bracket unrestrained so that a fixture does not conceal distortion. Keep the trial quantity and observations separate from statistical production claims.
If further heat treatment is required, repeat the relevant checks after that operation. The preferred incoming condition is the one that supports a compliant final part with a controlled route. A favorable rough-machining result is insufficient if subsequent treatment changes the critical bore position or invalidates the intended mechanical state.
Separate hardness, chemistry and process evidence
Hardness is a useful discriminator, but it is not a complete material identity test. Different structures can give overlapping hardness readings. Surface preparation, test location, section and the chosen method also influence interpretation. Use the result to answer the specified question rather than inferring an entire heat history from one indentation.
Likewise, chemistry confirms composition within the measurement’s scope but does not establish that a normalizing cycle occurred. A certificate may identify the supplied condition without proving the condition after later processing. These are complementary records, not substitutes for one another.
If residual-stress control is the concern, do not rename normalizing or annealing as stress relief. TWI's stress-relief guidance explains the separate purpose and the importance of material and temperature history. An additional treatment can change an already established condition and should be reviewed as part of the route.
When results disagree, compare the evidence chain before rejecting a material family. Check stock identity, represented section, sampling location and the timing of each measurement. Investigate whether the comparison unintentionally mixes incoming stock data with finished-part data. A narrower, well-supported conclusion is more useful than an unexplained universal statement that one condition is stronger or more stable.
Write incoming and final conditions as different requirements
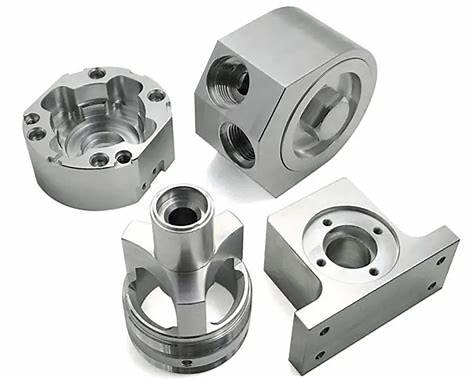
The drawing should separate the condition required for purchasing from the condition required for delivery. When those differ, define the responsibility for the intermediate route and identify the final acceptance tests. Include property limits only when they are justified by the design and can be measured on an agreed basis.
For a machined part, state which dimensions apply after final treatment and any subsequent finishing. Identify surfaces where scale removal, decarburization concerns or machining allowance must be addressed through the selected process specification. Do not copy a furnace temperature or holding time from a general guide into a production note without a material-specific procedure.
Record approved substitutions by grade, product form and condition. A blanket permission to use equivalent steel leaves both chemistry and thermal state uncertain. If the design permits alternative conditions, show the acceptance requirements that make those alternatives equivalent for the actual component.
The handoff should make it possible to trace a failed dimension or unexpected machining response back to a documented starting condition. That is more valuable than a lengthy process note that names annealing and normalizing but never states what the purchased stock or delivered part must satisfy.
FAQ
Can normalizing remove a hardened surface layer?
A new thermal cycle can alter an existing hardened condition, but the outcome depends on the steel, layer-producing process, temperature history and cooling path. It should not be used as an informal way to erase an unknown treatment. Identify the prior condition and obtain a material-specific disposition. If the surface layer is functionally required, the final component must still meet that requirement after every subsequent operation, including any proposed normalizing treatment.
Is a normalized material certificate enough for a welded assembly?
The certificate describes the represented incoming material, not automatically the local condition after welding. Welding introduces a thermal cycle and a heat-affected region that can require its own qualification and acceptance. Define the assembly requirements with the responsible welding and materials specialists. Keep the stock certificate as part of traceability, but do not use it to claim that the complete welded joint retains the same structure or properties everywhere.
Should a drawing specify annealed steel when only appearance matters?
Only if that condition has a justified role in manufacturing or function. Appearance is usually controlled through defined surface and finishing requirements, while annealing identifies a material-processing state. Using a condition label to obtain a cosmetic result can restrict sourcing without defining the desired surface. Clarify whether the concern is machining marks, scale, coating appearance or another observable feature, then specify that requirement and any necessary material condition separately.
Conclusion
The practical choice between annealed and normalized steel begins with the required final state. Cooling path and starting structure influence machining behavior, but grade, section and subsequent operations prevent a universal ranking. A softer incoming bar, a refined structure and a compliant finished component are related objectives rather than interchangeable descriptions.
Purchase the condition intentionally, retain stock identity and verify the characteristics that actually matter. Keep process documentation, hardness, microstructure and final dimensional evidence within their separate scopes. A substitution becomes defensible when those records show that the intended component requirements remain satisfied through the complete route.
For a machining review, provide 6CProto the steel specification, incoming and final conditions, critical features and required evidence. This supports a focused discussion of the material route without treating a general heat-treatment label as proof of the finished part’s performance.
{“@context”: “https://schema.org”, “@type”: “FAQPage”, “mainEntity”: [{“@type”: “Question”, “name”: “Can normalizing remove a hardened surface layer?”, “acceptedAnswer”: {“@type”: “Answer”, “text”: “A new thermal cycle can alter an existing hardened condition, but the outcome depends on the steel, layer-producing process, temperature history and cooling path. It should not be used as an informal way to erase an unknown treatment. Identify the prior condition and obtain a material-specific disposition. If the surface layer is functionally required, the final component must still meet that requirement after every subsequent operation, including any proposed normalizing treatment.”}}, {“@type”: “Question”, “name”: “Is a normalized material certificate enough for a welded assembly?”, “acceptedAnswer”: {“@type”: “Answer”, “text”: “The certificate describes the represented incoming material, not automatically the local condition after welding. Welding introduces a thermal cycle and a heat-affected region that can require its own qualification and acceptance. Define the assembly requirements with the responsible welding and materials specialists. Keep the stock certificate as part of traceability, but do not use it to claim that the complete welded joint retains the same structure or properties everywhere.”}}, {“@type”: “Question”, “name”: “Should a drawing specify annealed steel when only appearance matters?”, “acceptedAnswer”: {“@type”: “Answer”, “text”: “Only if that condition has a justified role in manufacturing or function. Appearance is usually controlled through defined surface and finishing requirements, while annealing identifies a material-processing state. Using a condition label to obtain a cosmetic result can restrict sourcing without defining the desired surface. Clarify whether the concern is machining marks, scale, coating appearance or another observable feature, then specify that requirement and any necessary material condition separately.”}}]}