

Explore Rapid Prototyping & Low-Volume Guides
Ask for a quote on 100 CNC machined parts and the unit price looks absurd next to the same part at 5,000 pieces. The gap is not a pricing trick—it is the shape of the cost model. Before the first part is cut, every order absorbs work that has nothing to do with the part count: reading the drawing, writing the program, preparing fixtures, proving the first article, and handling the paperwork. Low-volume pricing is simply the story of how those fixed blocks spread across a small number of parts, plus the variable costs that scale with each unit. This guide separates the three charge types, works through the numbers, and gives you a line-item checklist that exposes the assumptions hiding inside any quote.
The Cost Model That Explains Every Quote
Everything in a low-volume quotation fits into three buckets: one-time charges, recurring charges, and pass-through costs.
- One-time charges are paid once per project: hard tooling such as molds or dies, custom fixtures, and sometimes first-article inspection development.
- Recurring charges repeat on every order or every run: programming, setup, soft-tooling amortization, and order administration.
- Pass-through costs scale with each part or shipment: material, machine time, finishing, per-part inspection, packaging, and freight.
Read as a formula, per-part cost equals one-time charges divided by quantity, plus recurring charges per order divided by quantity, plus pass-through cost per part. At small quantities the first two blocks dominate—which is why a simple part at 100 pieces looks expensive per unit. At high volume those blocks vanish into a rounding error and the pass-through lines decide the price. The buyer who understands this stops comparing unit prices across different quantities and starts asking which order-level costs are actually in the quote.
Pass-through charges deserve the closest look because they are where otherwise identical quotes diverge. Material is priced by grade and by form, so a standard 6061-T6 bar and a special-order alloy can differ by more than the machining line itself—which is why the CNC machining materials library is the right reference when comparing quoted alloys. Finishing is often charged by surface area or by batch rather than by piece, which changes the comparison when the same part is quoted at two quantities. Inspection scales with the number of critical dimensions and the depth of the report—a quick visual check and a CMM report with dimensional data are different cost lines. Freight depends on weight, packaging, and destination, which is why comparing landed cost rather than unit price is the only fair comparison.
How Quantity Changes the Quote
The math is easiest to see with a worked example. Suppose an order carries $500 of one-time tooling, $400 of recurring setup and programming, and $11 of pass-through cost per part. The per-part price looks like this:
| Quantity | Fixed share per part | Pass-through per part | Total per part |
|---|---|---|---|
| 100 | $9.00 | $11.00 | $20.00 |
| 500 | $1.80 | $11.00 | $12.80 |
| 2,000 | $0.45 | $11.00 | $11.45 |
The example is deliberately simple, but it shows the shape that matters: unit price falls quickly at first, then flattens. Beyond a few thousand parts the fixed share is small, and further savings come from variable-cost breaks such as cheaper material pricing or faster cycles—not from the fixed block shrinking again.
The shape is not a reason to over-order. If you need 500 parts, the relevant comparison is 500 against the alternatives at 500, not against a price at 100,000 that assumes a different process entirely. Reading the curve also means reading the total, not just the per-part number. A batch of 2,000 parts at $11.45 each is roughly $22,900 of manufacturing cost; ordering the same parts in four runs of 500 adds the recurring setup charge three extra times. The curve therefore answers two different questions—how large a single batch should be, and whether repeated small orders cost more than one larger order. Both answers depend on the supplier’s recurring-charge policy.
What Design Choices Change Cost Before Production
Design decisions move both blocks of the model, and at low volume the leverage is larger because the fixed share is bigger. The highest-leverage levers are:
- Material grade and form: a standard grade in a standard stock size avoids minimum-purchase surcharges and long material lead times.
- Feature depth and geometry: deep pockets, thin walls, and long tools extend machine time, which no quantity discount removes.
- Tolerance spread: tolerances tighter than the function needs add finishing passes and inspection hours to every part.
- Finish scope: a cosmetic finish is a per-part step; specifying it only where the product needs it keeps cost down.
- Setup count: features that need a second machine or a second operation add a recurring charge to every order.
None of this argues against quality. It argues for specifying quality where the product needs it, and for reading a quote to see which of these levers are already priced in; formal quality-management expectations for the supplier follow international quality standards. A design change that removes a second setup or a custom tool saves money at every quantity—and saves proportionally more at low volume.
How Cost Structures Differ by Process
Different processes put their weight on different blocks, which changes the quantities where each becomes attractive.
| Process | Where the cost sits | Practical guidance |
|---|---|---|
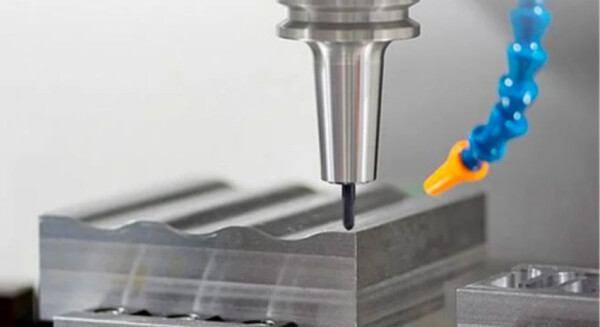
| CNC machining | Programming and setup recurring; machine time per part | Strong for functional metal and plastic parts at almost any low volume |
| 3D printing | Very little tooling; machine time and material per part | Suited to complex geometry and single-digit quantities |
| Vacuum casting | Master pattern and silicone mold one-time; low per-part cost | Competitive for small cosmetic batches; mold life limits repeat runs |
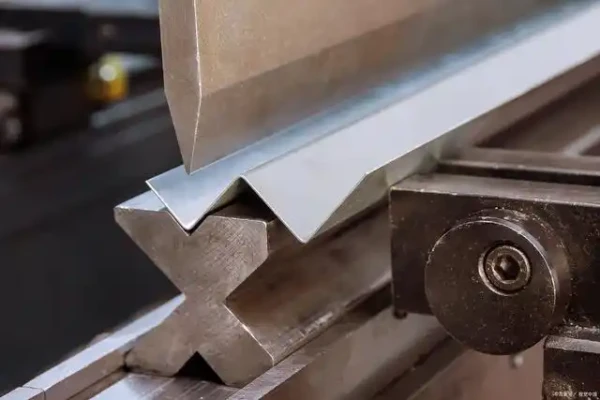
| Sheet metal fabrication | Programming and tooling recurring; low material and bending cost | Common for enclosures and brackets across a wide quantity range |
| Injection molding | Hard tooling one-time; very low per-part cost | Becomes competitive when tooling is amortized across sufficient demand |
Injection molding is the clearest example of why fixed thresholds fail; the injection molding service page breaks out the tooling line the same way a quote should. It becomes competitive when tooling is amortized across enough parts, but the break-even point varies materially with part size, resin, cavity count, tool specification, required finish, and forecast stability. The useful method is to compare total landed cost at your expected quantity rather than apply a universal “thousands of parts” rule. A low-volume manufacturing program at 6CProto spans these processes, which makes the quantity comparison a real choice instead of a forced one.
Quantity Ladders, Minimums, and the Reorder Trap
Quotes rarely arrive as a single smooth curve; they come as quantity ladders with discrete steps. The price per part falls as the fixed block spreads, and the material and labor lines follow the batch—but the quote that jumps discontinuously between quantities deserves a question about setsup and minimums. Minimum order quantities exist for a reason: a supplier that stops a CNC line to run ten parts absorbs the setup in the quote, while a sheet-metal run needs its bend tooling and fixtures regardless of batch size. The buyer should ask what the price step actually buys—additional setup, new material lots, or a different inspection sampling plan—because a step that is simply a round-number discount is a pricing convention, while a step that reflects real setup and material economics is a fact about the process.
The reorder trap is subtler. A low initial price can hide recurring charges that apply to every future order: if programming is re-billed on each release, if fixtures are stored for a fee, or if a new first-article inspection is triggered by every engineering change, the second order costs more than the first. Asking "what does the next order cost?" is often more revealing than asking "what does this order cost?"—and it is the question that separates a one-off quote from a repeatable manufacturing relationship.
A Quote-Comparison Checklist for Buyers
The most practical asset in this article is a line-item question set to run against any low-volume quote. For each line, ask the supplier the question on the right—the answer reveals where the money actually sits.
| Quote line item | Ask the supplier | Why it matters |
|---|---|---|
| Setup / programming | Charged once, per release, or on every reorder? | Reveals the real cost of repeat orders |
| Tooling / fixture | Who owns it? How long is it retained? | Avoids hidden restart costs |
| Inspection | Is first-article inspection included? What report comes with it? | Prevents surprise quality-document fees |
| Material | What grade and form are assumed? Is there a MOQ surcharge? | Shows substitution headroom |
| Finishing | Priced by surface area, batch, or piece? | Explains why the same part differs across quantities |
| Freight / taxes | Included or excluded? | Compares landed cost, not unit price |
Run these questions against two or three suppliers and the picture changes from “who is cheapest” to “who is charging for what.” A practical way to run the checklist is to score answers rather than totals: record the line items, mark which charges are one-time versus recurring, and note the assumptions behind material and finishing. The same exercise is central to evaluating an instant quote for 5-axis work, where the instant 5-axis quote evaluation asks exactly these questions before the number is trusted. Then compare the two lowest totals line by line—a supplier that is cheaper on machining but assumes a non-standard material may not be cheaper once the material surcharge lands. That hour of work reliably surfaces the hidden-cost pattern that unit-price comparison misses.
FAQs
Why is the per-part price so high for a small batch?
Because one-time and recurring charges—tooling, programming, setup, and first-article inspection—are spread across a small number of parts. At 100 pieces a $900 fixed block adds $9 per part; at 2,000 pieces it adds $0.45.
At what quantity does low-volume manufacturing stop making sense?
There is no universal number. The per-part curve flattens once the fixed share is negligible—often by a few thousand parts—but the right quantity depends on the process, geometry, material, and finish. Compare total landed cost at your actual quantity instead of applying a fixed threshold.
What should I ask for in a low-volume quote?
Ask for line items: setup and programming, tooling or fixtures, material, machining or fabrication, finishing, inspection, and freight. Then ask which charges are one-time, which repeat per order, and which are per part.
Can I reduce low-volume cost without changing quantity?
Yes. Standardize material grades and stock sizes, relax non-functional tolerances, batch orders to avoid repeated setups, simplify geometry to cut machine time, and review the design feedback before committing. Each lever removes either a fixed or a variable block.