

Explore Sheet Metal Processes & Supplier Selection
How Metal Stamping Lowers the Cost of High-Volume Parts
Metal stamping services boost high-volume production by using custom dies and high-speed presses to form complex parts from coil or sheet metal in a fraction of a second. Once the tool is tuned, each stroke produces another identical part, which is why the economics, quality consistency, and throughput all change at scale. A bracket that takes minutes to machine can be stamped in milliseconds, and the per-part cost falls because the tooling investment is spread across hundreds of thousands of pieces.
The gains are real but conditional. Stamping trades tooling cost against per-part cost, so the high-volume economy is earned only when volume and design stability justify the tool. This guide explains how the processes work, where progressive dies beat single-hit tooling, which materials suit stamping, and how to bring a program into stamping without repeating the mistakes that break die projects.
How the Processes Work: Progressive vs. Single-Hit
Progressive die stamping feeds coil through a multi-station die, performing several operations at each press stroke until a finished part exits with every hit. One station pierces a hole, another forms a bend, a third coins a contact area, and a fourth cuts the final profile. Because the strip advances through all stations per stroke, progressive dies are the most cost-effective route for stable, high-volume parts.
Single-hit stamping uses separate dies and presses for each operation, or one stroke for one form. It costs less upfront and suits lower volume, larger parts, or thick materials where multi-station tooling is not justified. Many programs run both: laser cutting with a press brake and single-hit tools for early production, then migrate to a progressive die once demand stabilizes.
The difference is a volume decision, not a technology preference. The break-even volume, where the progressive tool’s higher cost is repaid by lower per-part cost, is the number to calculate before tooling starts. A good supplier will show that calculation rather than sell the fancier tool.
The Common Stamping Operations
Stamping is a family of operations, and most production parts use several in sequence:
- Blanking cuts the outer profile from strip or sheet.
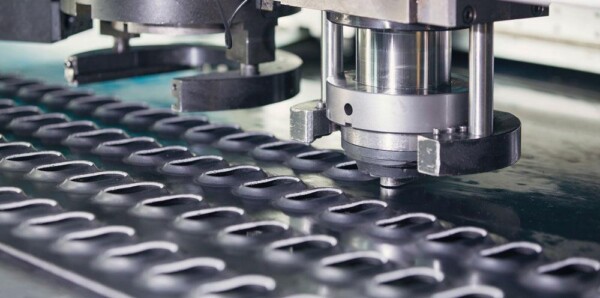
- Piercing punches holes, slots, and cutouts.
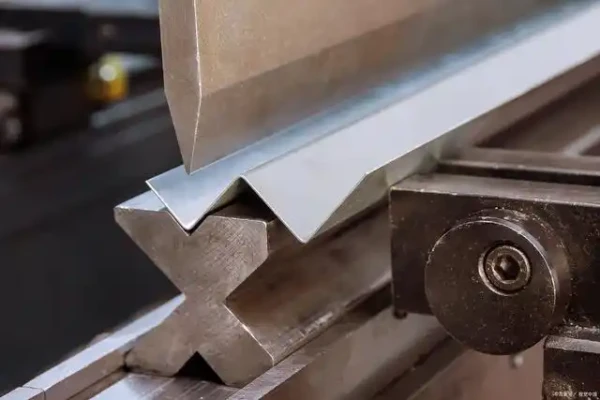
- Bending creates angles, flanges, and tabs.
- Forming shapes complex contours and channels.
- Coining tightens tolerances and sharpens features in specific zones.
- Embossing raises or recesses logos and patterns.
- Drawing forms cups and deep-drawn housings.
A single progressive tool may combine five or more of these in a carefully sequenced layout. The strategic use of coining deserves attention: contact areas can be coined to control thickness within tight bands while non-critical regions stay as simple blanks. That mix of coarse and fine features in one press shot is the real power of precision stamping, and it is why the die layout matters more than the press itself.
What Precision Stamping Delivers at Scale
The difference between commodity stamping and precision stamping shows up in microns and parts-per-million. A generic tool may drift with wear and heat, producing parts that pass a loose in-house check but fail the customer’s gauge. Precision stamping controls the variables: die design, in-die sensing where volume justifies it, material condition, and press tuning, so dimensional variation stays low across millions of parts.
For tight-tolerance applications, connectors, terminals, brackets, and shielding in automotive, electronics, and medical devices, precision stamping routinely holds important features within about plus or minus 0.05 mm when the part and die are well designed. The realistic number depends on thickness, geometry, and material, and DFM discussion is the only honest way to set it. Ask what tolerance is demonstrated on a similar part, not what the brochure claims.
Materials and Thicknesses That Stamp Well
Stamping works on materials that deform rather than crack under the die: low-carbon steel, stainless steel in the 300 series, aluminum and its alloys, copper and brass, and some coated or pre-finished materials. Thickness ranges from thin foil up to heavy plate, with each material grade behaving differently under the press.
- Low-carbon steel is the general workhorse: formable, weldable, and cheap at volume, covering brackets, enclosures, and structural parts.
- Stainless steel brings corrosion resistance, and the 300 series grades stamp well when the die geometry allows for the hardening the alloy exhibits under deformation.
- Aluminum stamps cleanly with lighter tonnage, carries the weight advantage, and suits heat-management and lightweight parts.
- Copper and brass appear in electrical contacts, terminals, and decorative parts where conductivity or appearance matters.
Material and thickness choices interact with the die. Change the grade or gauge and springback, formability, and required tonnage all change, often demanding die modification or a full redesign. Confirm the material with the stamping partner before tooling, and treat any later change as a tooling question.
Springback deserves its own note because it is the failure most often discovered after tooling. When the press releases, the material returns partway, and the difference between the die angle and the final part angle depends on the grade, the gauge, and the bend radius. A die that does not over-bend for the materialu2019s springback produces parts that consistently miss the drawing, and the fix is a die change, not a tolerance conversation. The material grade and thickness must be fixed at DFM so the die is designed against the real springback.
`n
Coil and strip preparation matters at the same level as the die. Strip width, flatness, and surface condition feed directly into the tool, so a coil with edge damage or inconsistent gauge produces scrap at press speed. Precision piloting and lubrication, part of the line setup, keep the strip registered to the die through every stroke. These details are invisible in the per-piece price but visible in the reject rate.
When Stamping Replaces Machining or Laser Cutting
Not every part should be stamped. The economic crossover appears when three conditions hold: the part is needed in stable high volume, the geometry suits a die, and the design is frozen enough that the tool will not be re-cut next month. A machined or laser-cut part earns its keep at low volume because it needs no tooling; stamping earns its keep when the tooling is amortized over enough parts.
The migration pattern is practical: prototype with laser cutting and forming, run early production with single-hit tools, then move to a progressive die when demand stabilizes. Each step buys information at the cheapest price and keeps tooling money unspent until the design is proven. Stamping a part that has not been validated multiplies tooling risk, because die changes are expensive and slow.
Keeping a High-Volume Line Efficient and Stable
A stamping line is stable only when the variables are managed. Feed, lubrication, and strip condition are set for the run. Coining or sensing stations check critical features in-die where volume justifies it, catching drift before it becomes scrap. Dies are tracked and maintained on a schedule, because a worn edge shows up as drift before the parts fail inspection. Process capability data, collected across runs, is what converts a good first article into a predictable production line.
Buyers should ask for lifecycle cost models that include die maintenance, sharpening, and potential redesign, not just the per-piece price. A cheap part is not cheap if the die dies after a short run, and die maintenance is a real line cost that belongs in the comparison. The same model should show the break-even volume against machining or laser cutting, so the process decision is made on data.
Tolerance terminology and stamping practice in this guide align with the standards and engineering references published by ASME (ASME codes and standards), which also define the drawing conventions used in die and strip layout.
`n
Choosing a Stamping Partner and Starting Early
Because tooling is the risk, DFM review and die design belong before the tool order, not after it. 6CProto’s punching services cover progressive and single-hit stamping, and the sheet metal fabrication page shows the surrounding processes, laser cutting, forming and bending, and fabricated assemblies, that prototypes and panels use before stamping. The sheet metal materials page lists available grades and gauges so the material question is settled before tooling.
Starting early matters most. A DFM workshop on the prototype catches springback, hole-pattern, and tooling-approach issues while the design is still cheap to change. The article “How Should You Specify Sheet Metal Tolerances?” shows how the same discipline applies to the parts that will graduate into stamping, and the automotive industry page describes the high-volume applications where stamping is the standard answer.
FAQ
Can stamping handle complex 3D shapes?
Yes, but with limits. Complex shapes may need multiple forming stages, drawing operations, or secondary processes. Very deep or intricate geometries often combine stamping with machining or assembly steps instead of pushing a single die too far.
Are progressive dies always cheaper in the long run?
Often, but not always. Progressive dies pay off at high volume; lower or uncertain demand may never amortize the tooling cost. The break-even calculation, not the tool type, is the decision basis.
How long does a progressive die take to build?
Typical timelines run from 6 to 12 weeks depending on complexity, part size, and tool-room workload. Simulation, strip-layout optimization, and trial runs improve die reliability but extend the schedule, so plan the tooling lead time into the program.